Custom Investment Casting Foundry in China
Custom Investment Casting Services & Foundry Capabilities
SIMIS Investment Casting Manufacturing Capabilities
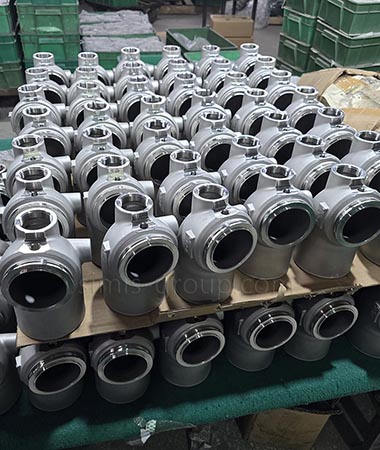
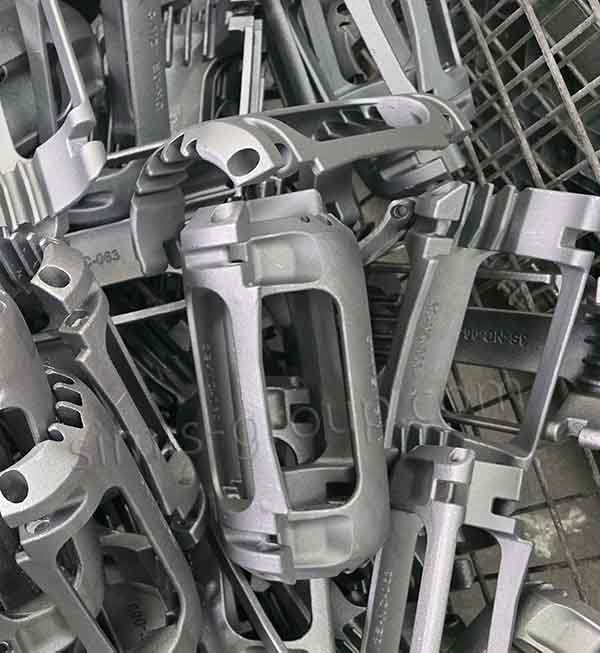
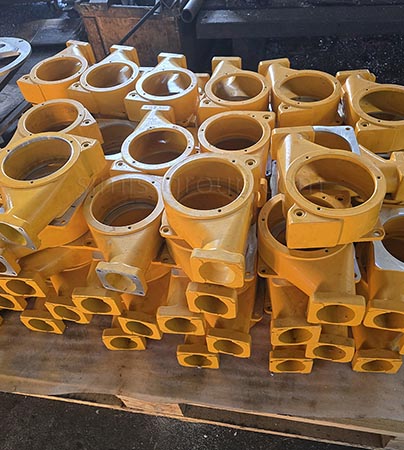
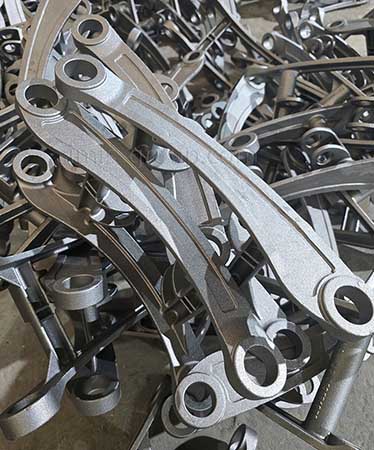
SIMIS manufactures custom investment castings (lost-wax castings) from customer 2D drawings and 3D models. We offer silica sol and water glass (sodium silicate) ceramic-shell routes for selected carbon steel, alloy steel, stainless steel and heat-resistant steel components. Process selection depends on the specified grade, casting geometry, quantity, as-cast tolerance and surface finish.
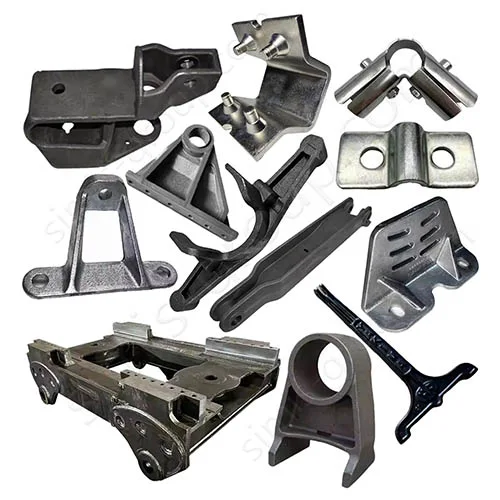
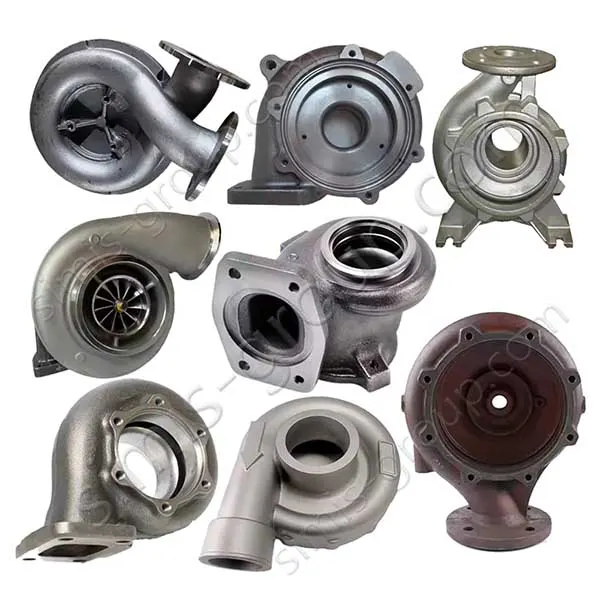
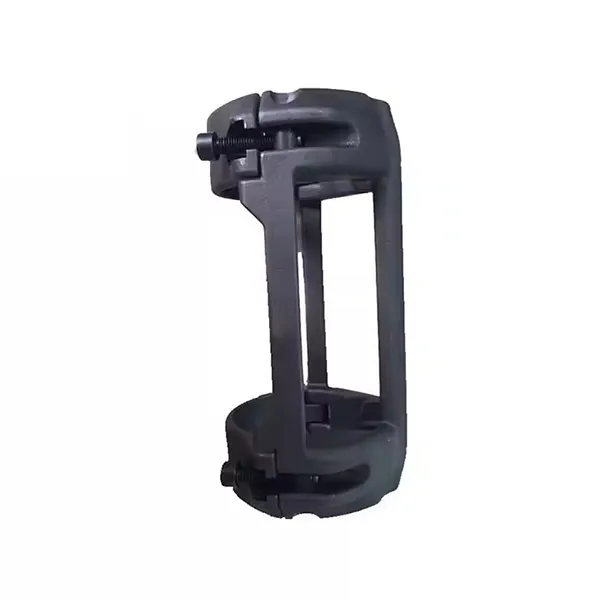
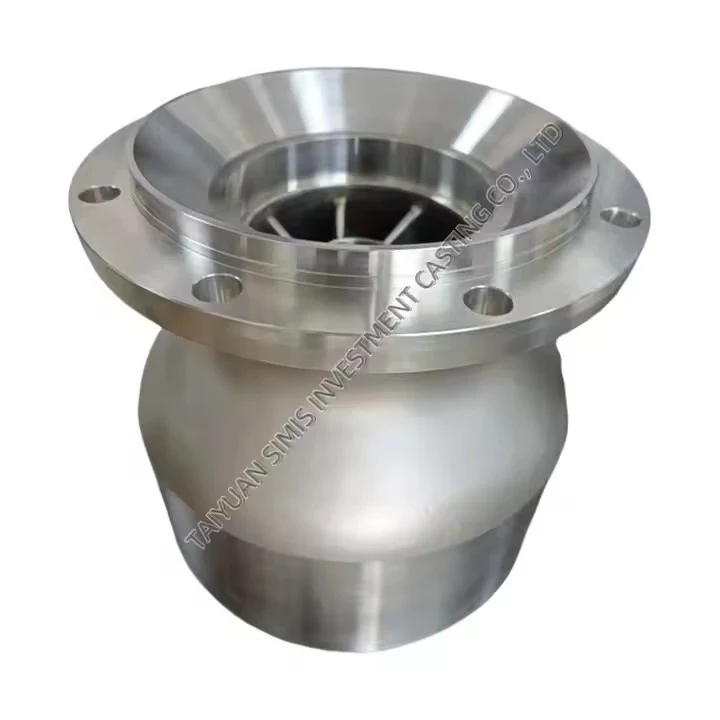
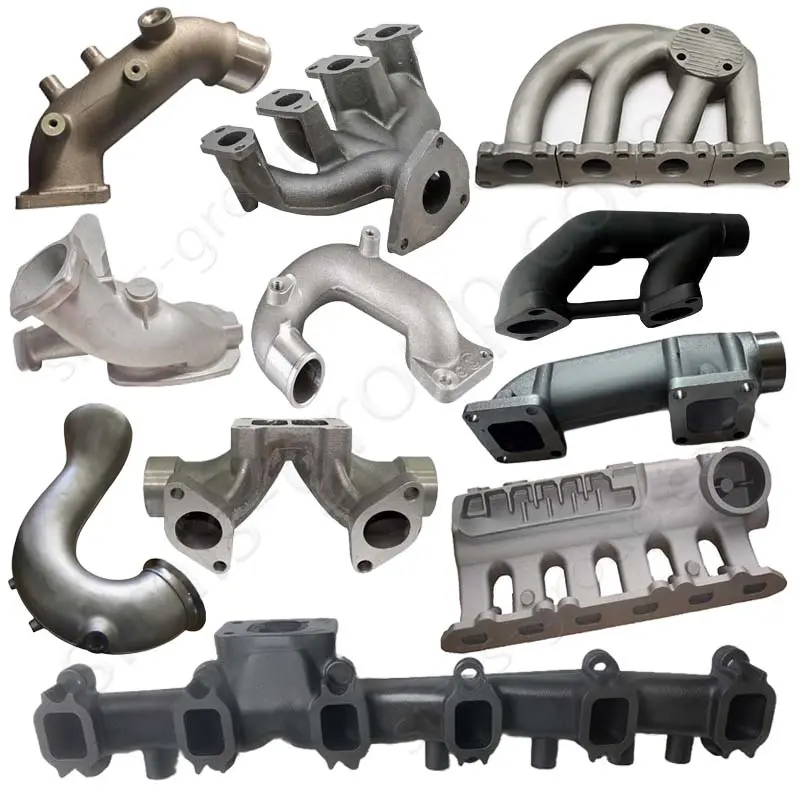
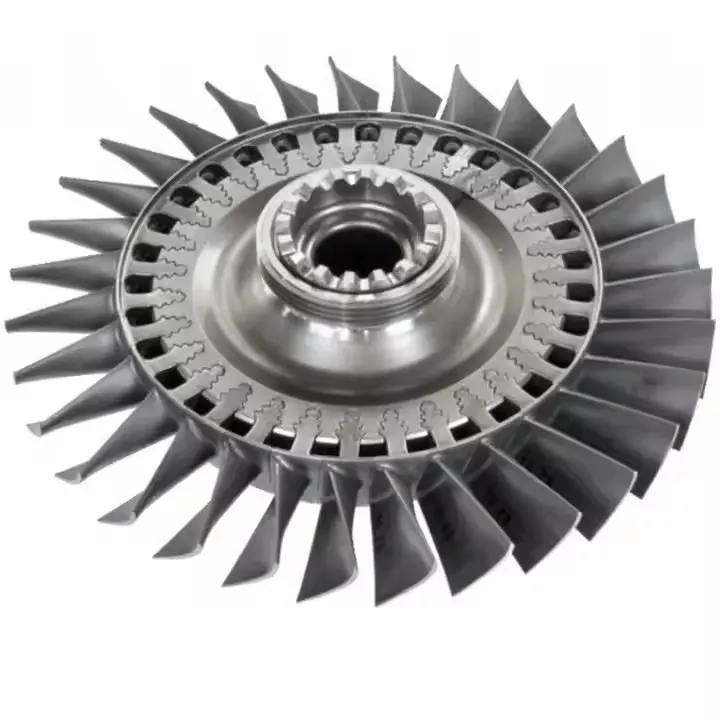
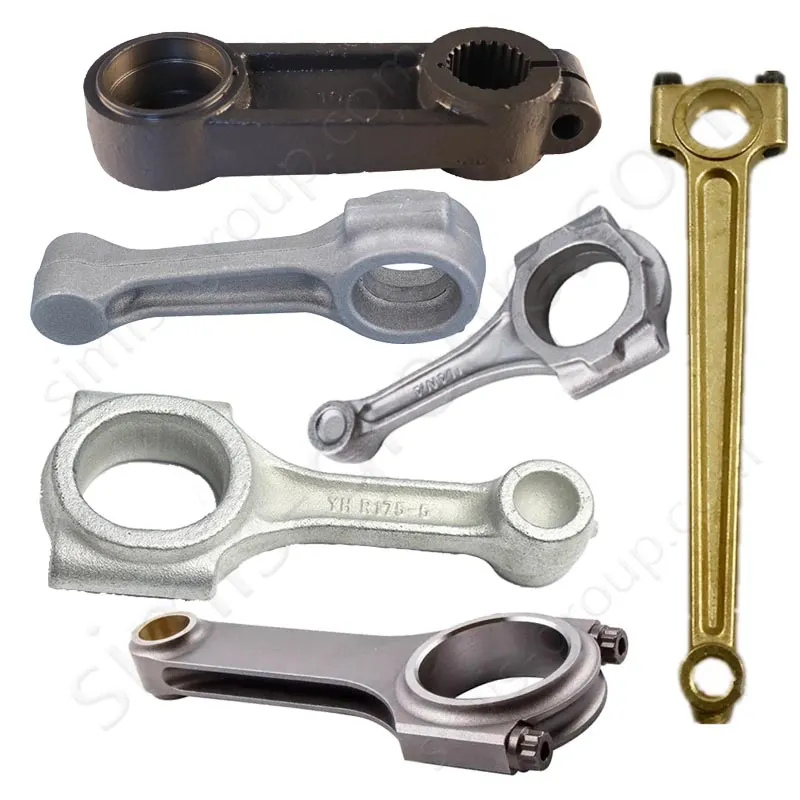
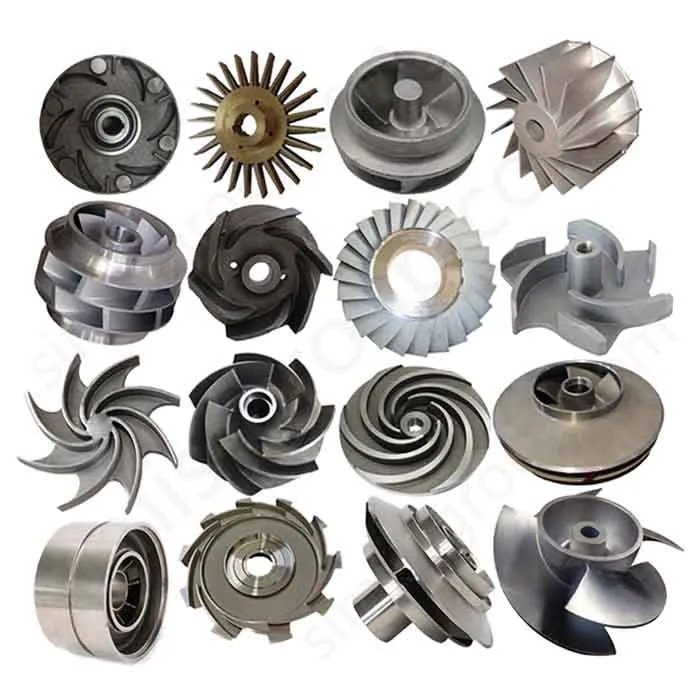
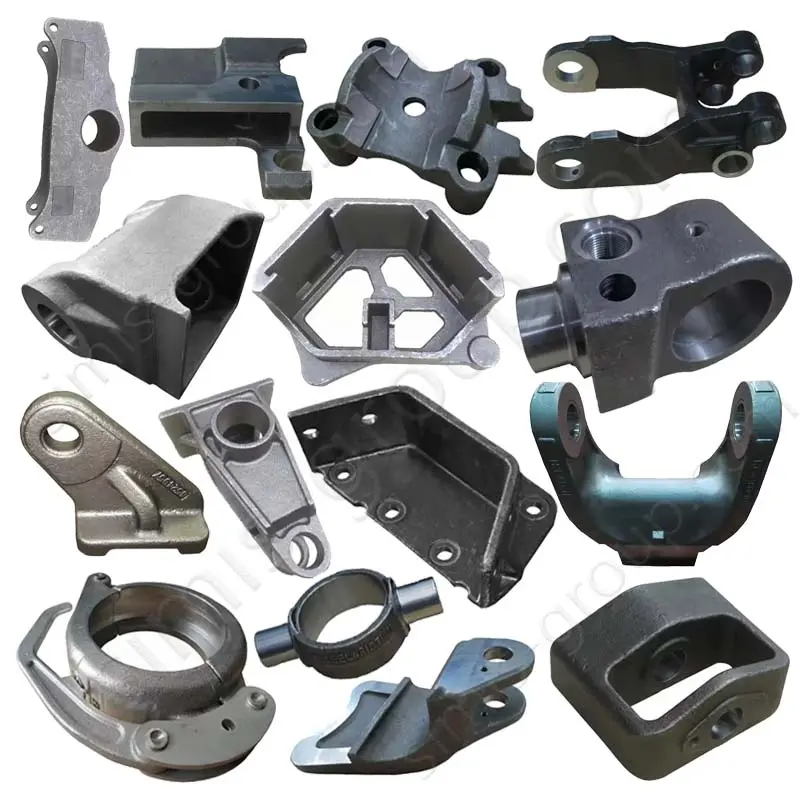
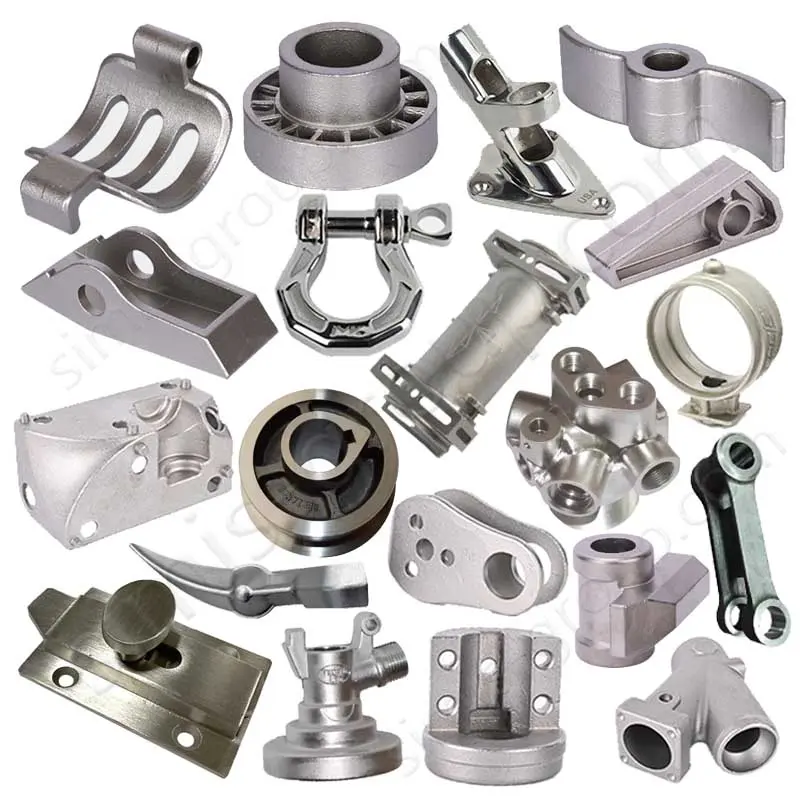
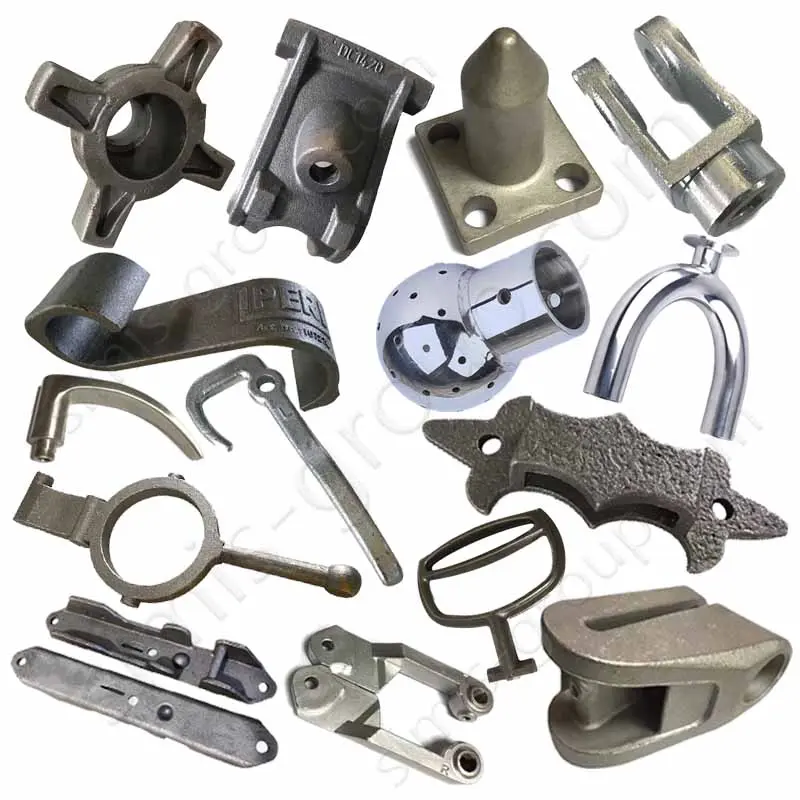
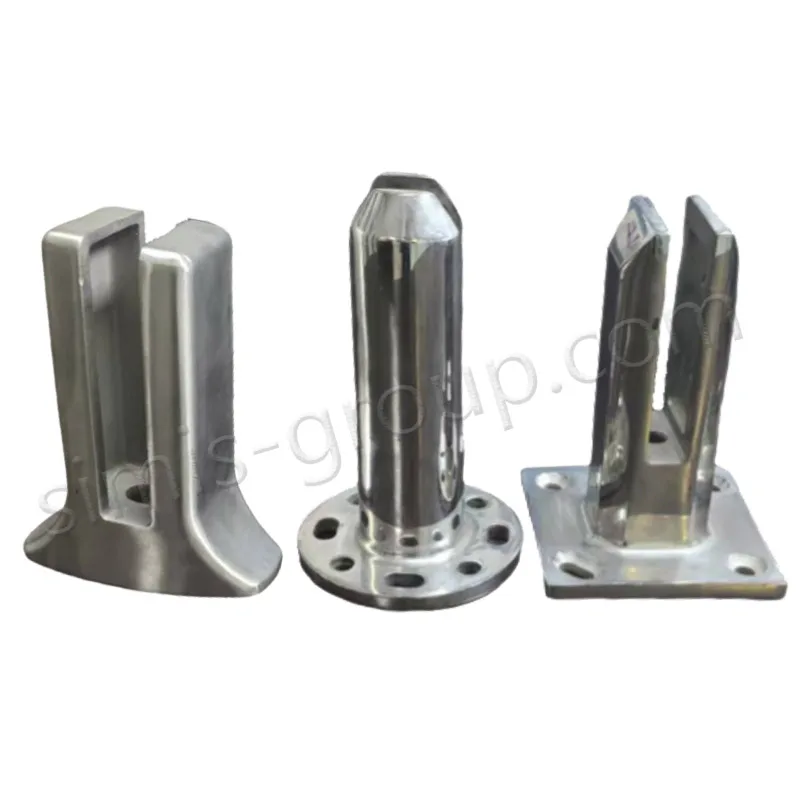
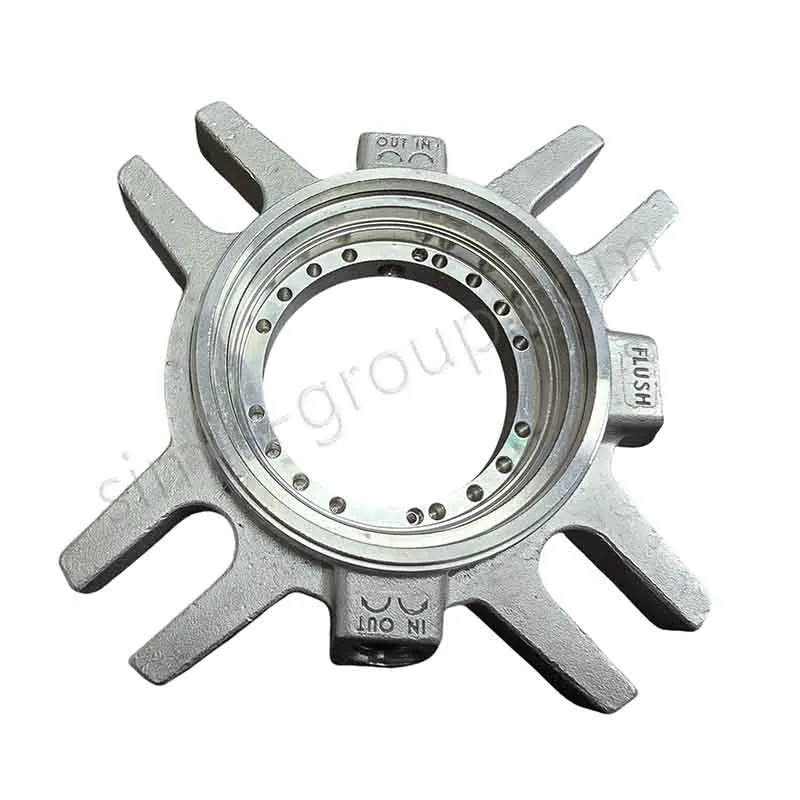
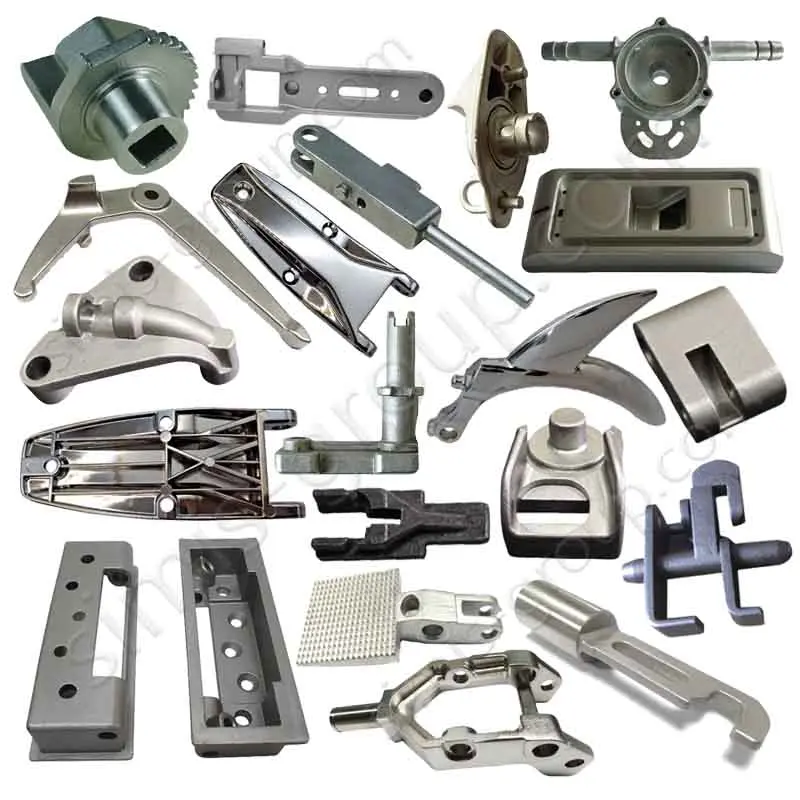
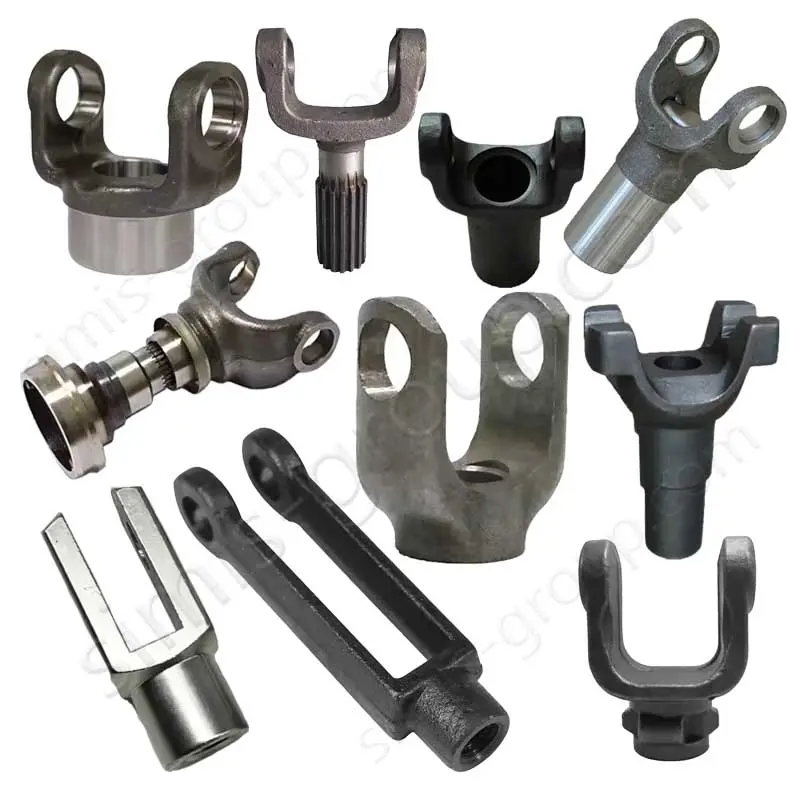
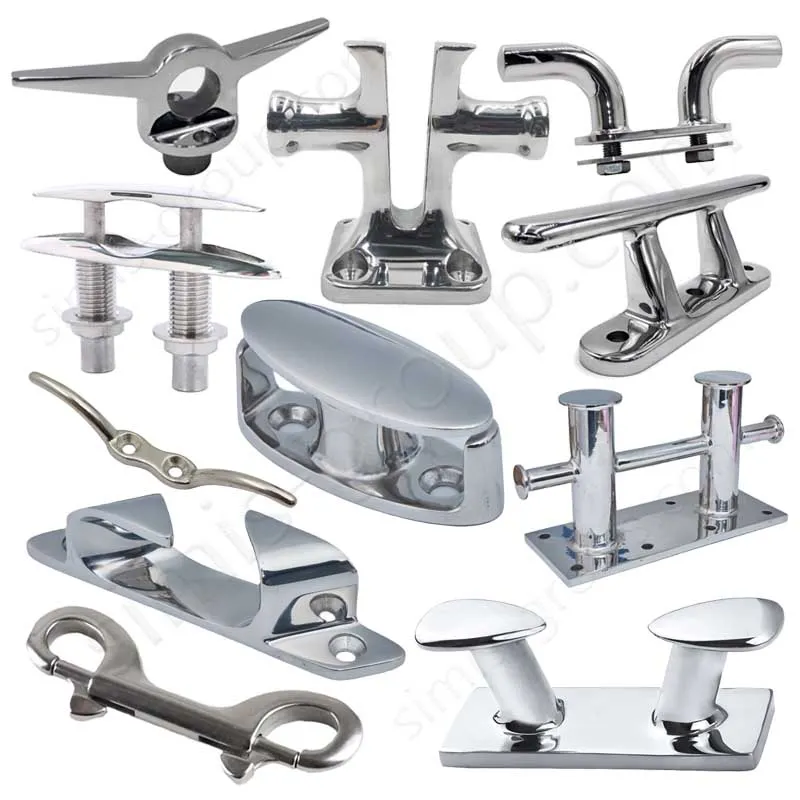
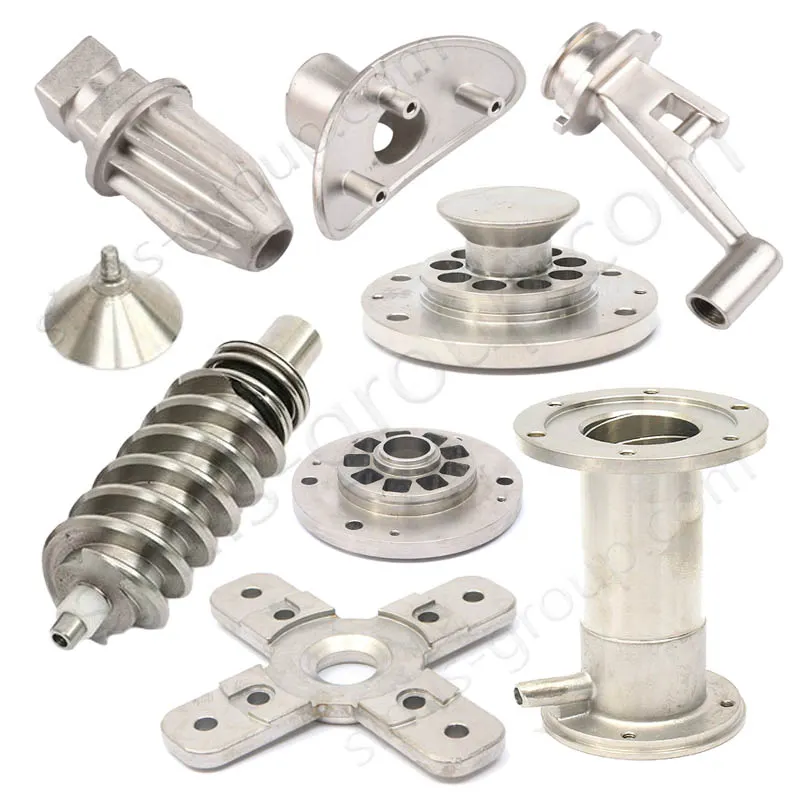
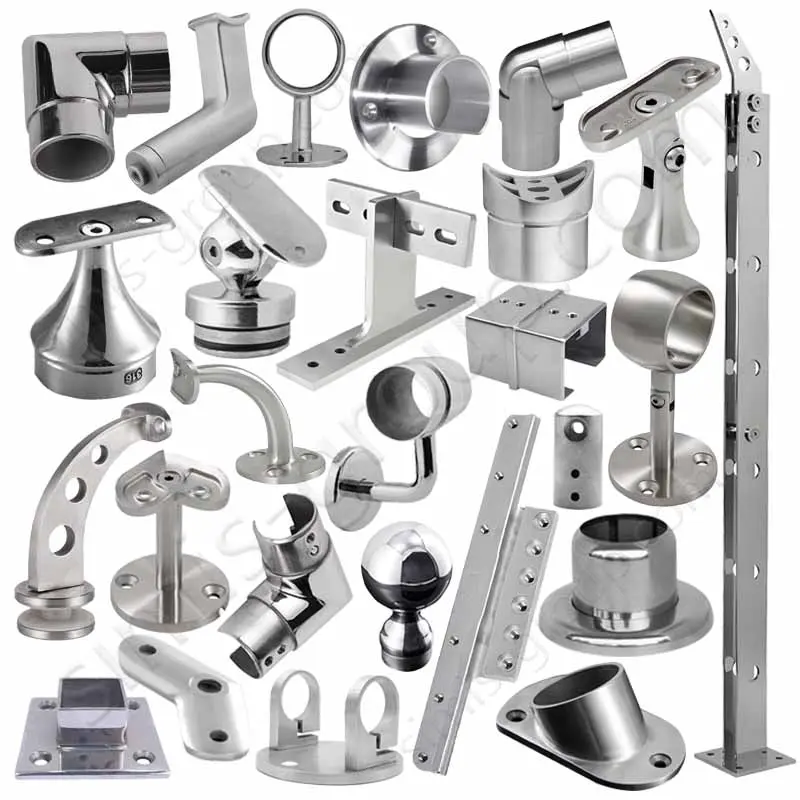
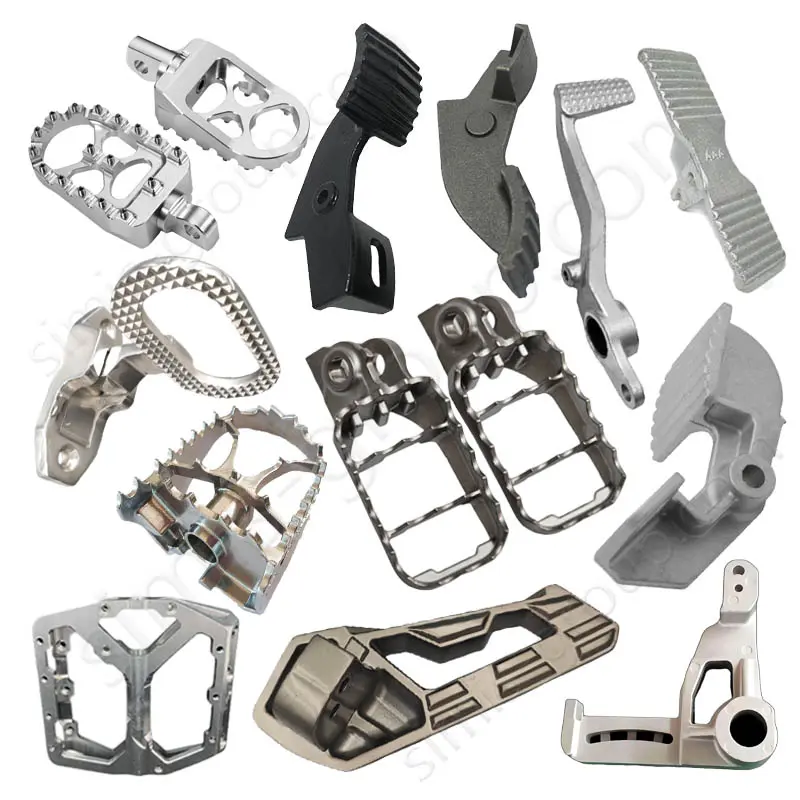
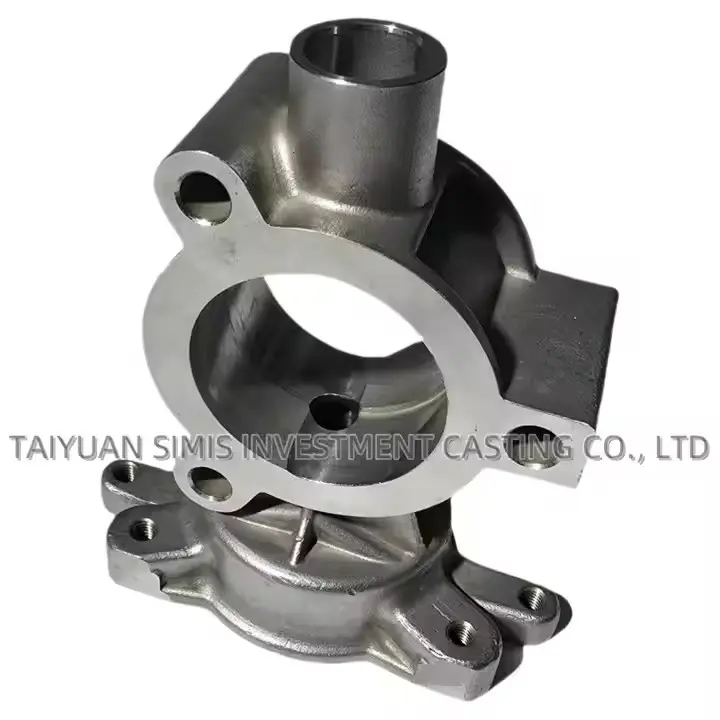
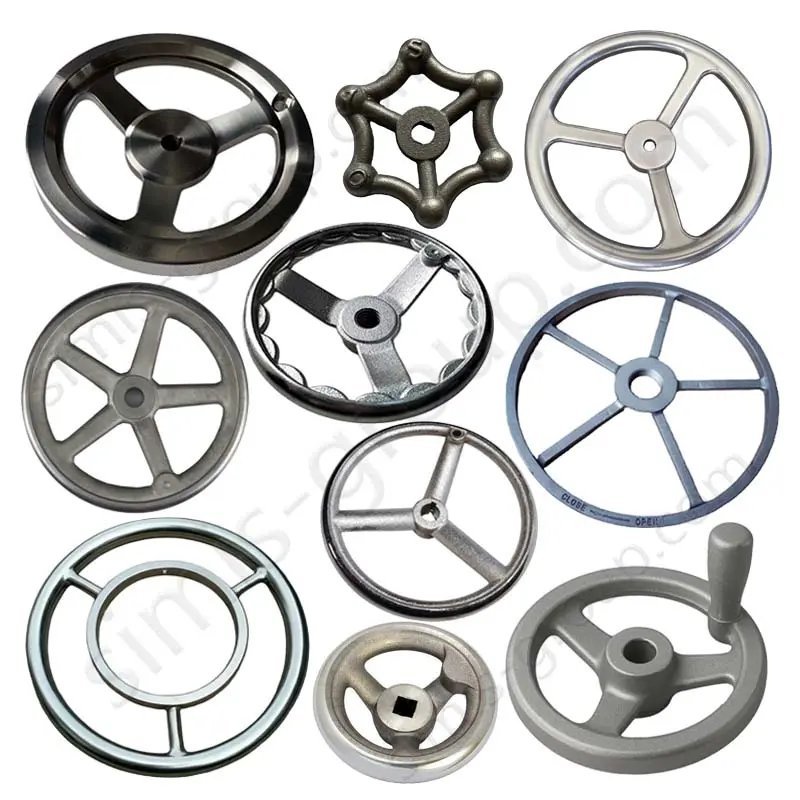
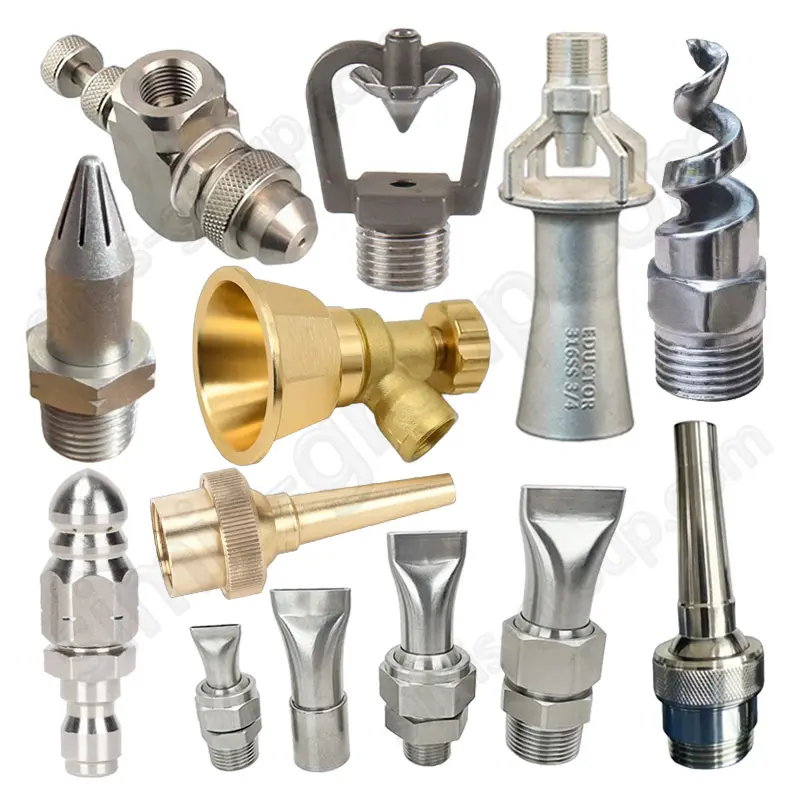
Typical OEM applications include precision brackets, valve and pump components, impellers, fittings and mechanical connectors. Our production resources include wax-pattern injection, ceramic-shell preparation and induction melting. Heat treatment, CNC machining and inspection can be coordinated according to the approved drawing and order requirements.
| Investment casting route | Reference piece weight | Reference maximum dimensions | As-cast tolerance | As-cast surface roughness |
|---|---|---|---|---|
| Water glass / sodium silicate | 0.5–100 kg | 600 × 600 × 400 mm | CT7–CT9 | Ra 6.3–12.5 μm |
| Silica sol | 0.01–50 kg | 500 × 500 × 300 mm | CT5–CT7 | Ra 1.6–3.2 μm |
OEM Investment Castings & Precision Metal Parts


Investment Casting Production Process & Quality Control
Investment Casting Process Overview
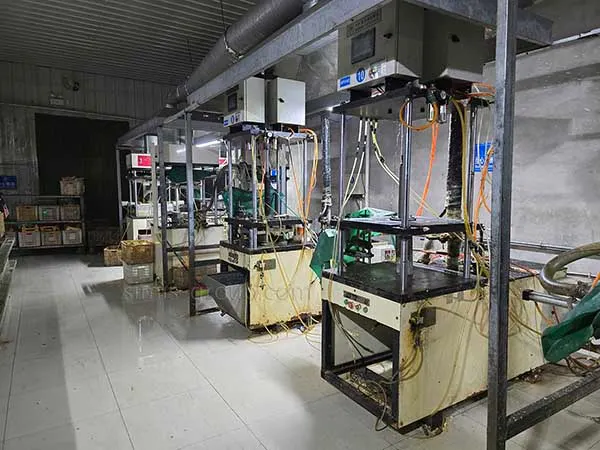
SIMIS plans lost-wax casting production around the approved part drawing, specified alloy, wax tooling, ceramic-shell route and acceptance criteria. The process covers wax-pattern production, assembly and shell making, dewaxing, shell firing, metal pouring, cleaning and any required heat treatment or CNC machining. Inspection points are defined according to part risk and customer requirements.
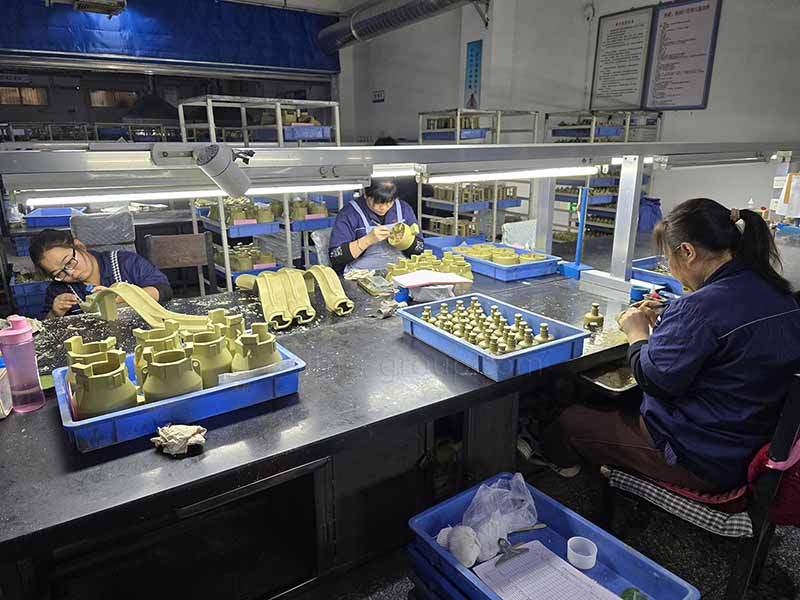
1. Wax Pattern Making
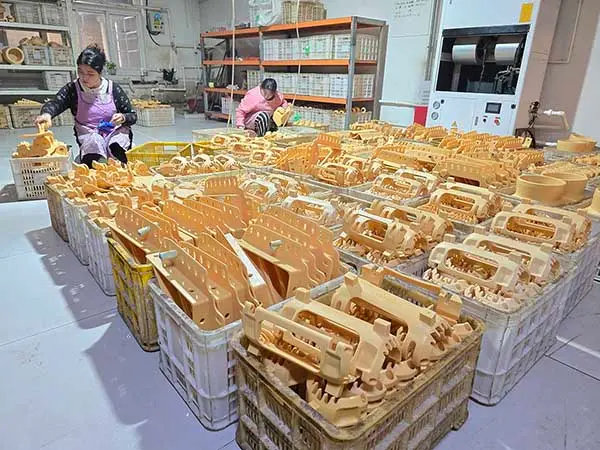
Produce wax patterns using tooling made for the approved casting design. Check dimensions and key features, including allowances for solidification shrinkage and subsequent machining. Pattern quality and repeatability are reviewed before assembly into the gating system.
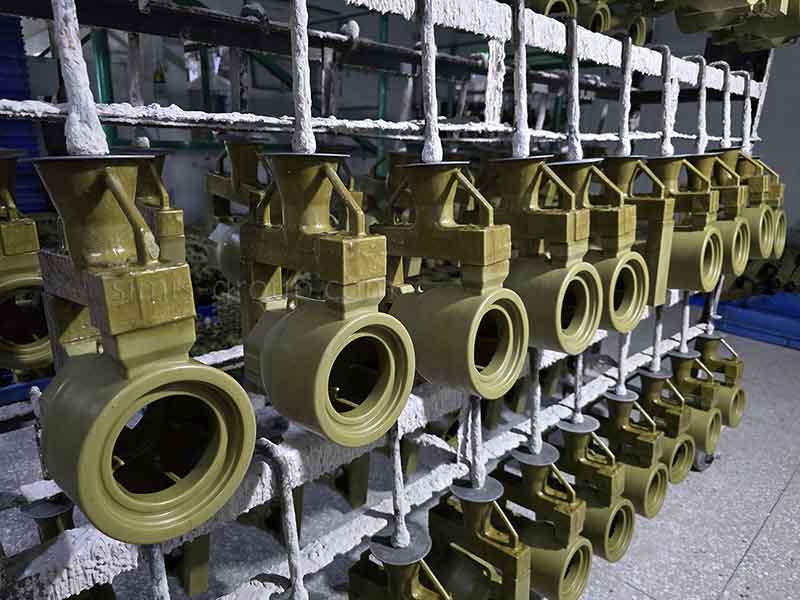
2. Wax Assembly (Tree Building)
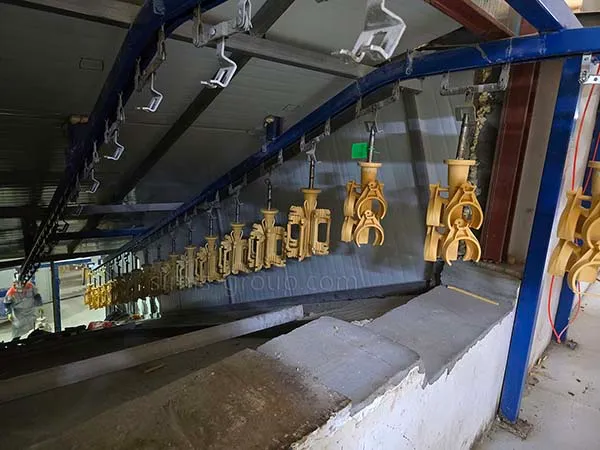
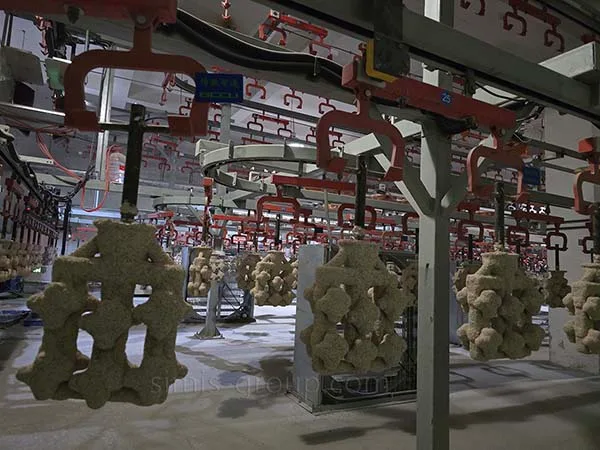
Attach approved wax patterns to a runner and gating system to form a casting cluster. The assembly layout is selected according to part size, alloy, feeding needs and production quantity. Connections and pattern placement are checked before ceramic-shell coating.
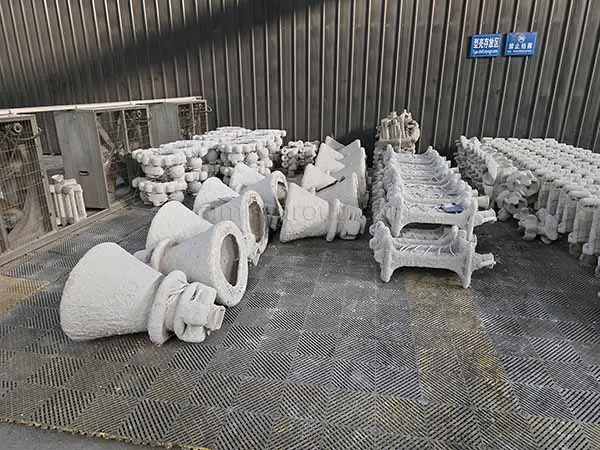
3. Ceramic Shell Making
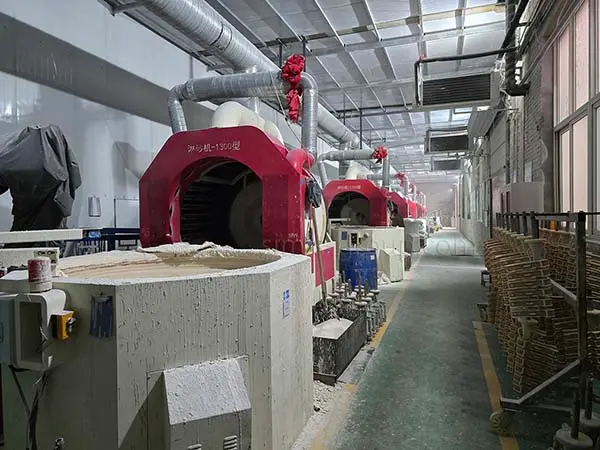
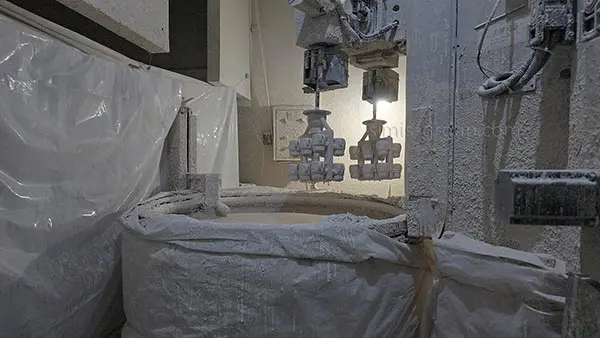
Build the ceramic shell by applying successive refractory slurry and stucco layers around the wax assembly. Select the silica sol or water glass route according to the part specification and planned casting process. Control coating coverage, drying and shell condition before dewaxing.
4. Dewaxing
Remove wax from the completed ceramic shell using a suitable controlled dewaxing process. Review shell condition and internal cavity integrity before firing. Wax removal parameters depend on tooling, shell construction and plant operating procedures.
5. Shell Firing
Fire or preheat the dewaxed shell according to the refractory system and casting alloy. The firing cycle prepares the ceramic mold for metal pouring and helps remove remaining moisture or residues. Shell temperature and handling are controlled according to the approved production route.
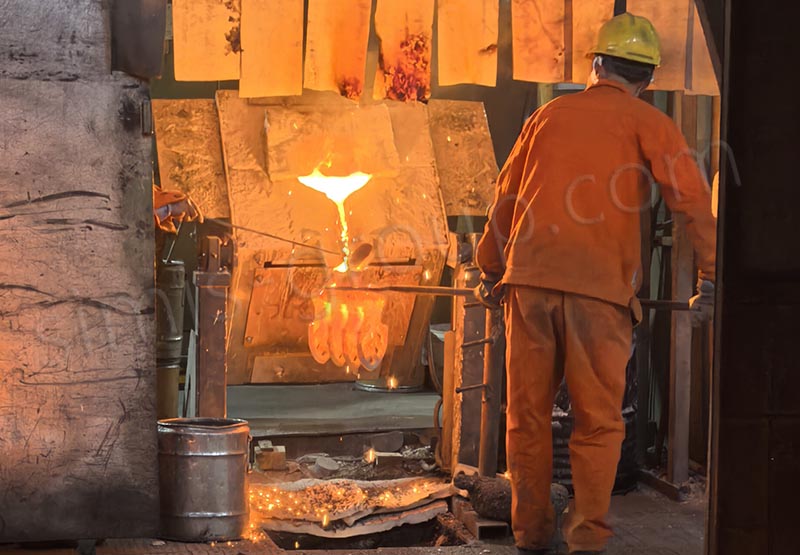
6. Melting and Metal Pouring
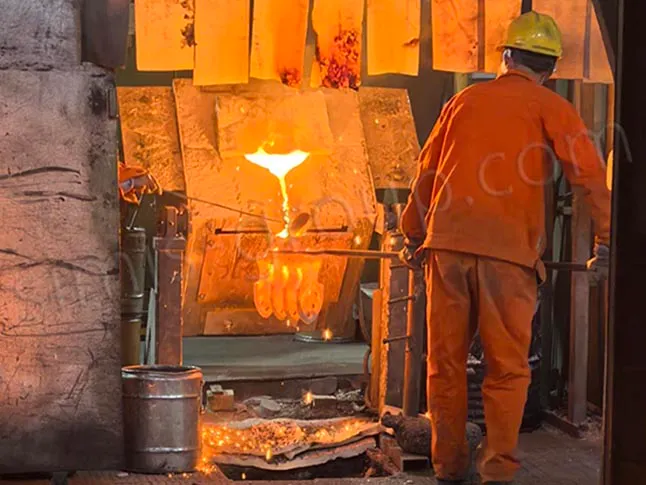
Melt the specified carbon steel, alloy steel, stainless steel or other approved alloy under the applicable composition and temperature controls. Pour into the prepared ceramic shell using the designed gating and feeding arrangement. Process conditions are selected for casting soundness, part geometry and production requirements.
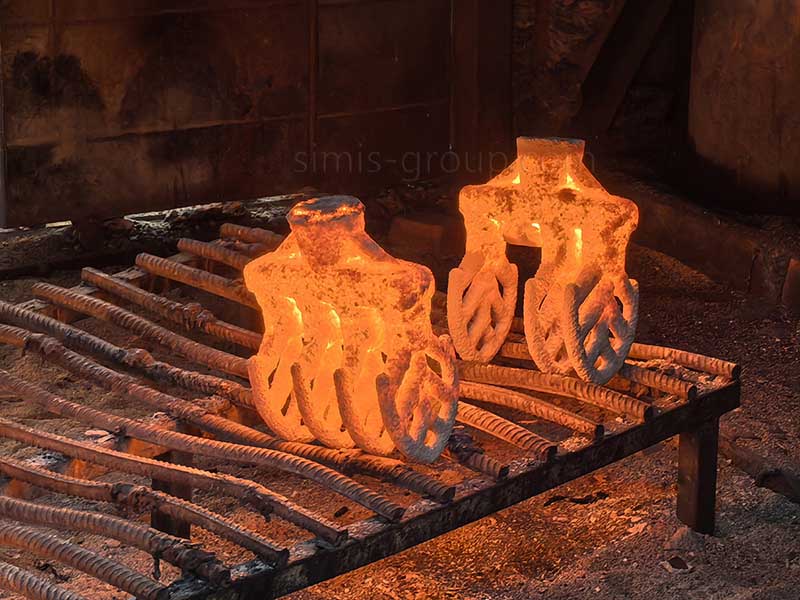
7. Cooling and Solidification
Allow the poured cluster to solidify and cool under conditions suitable for the alloy and section thickness. Cooling and feeding requirements are considered to manage shrinkage, distortion and casting integrity. Shell removal takes place after the appropriate cooling stage.
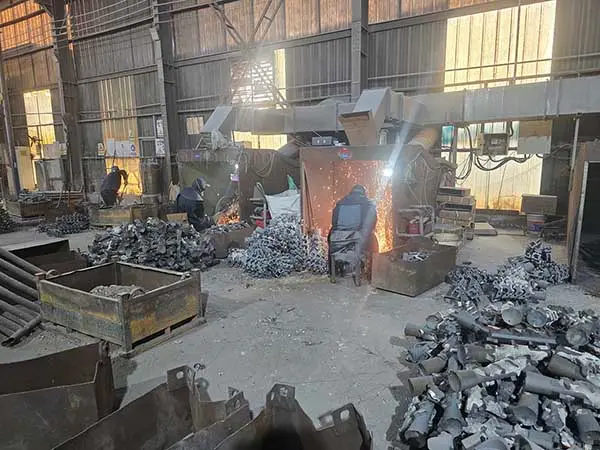
8. Knockout, Cutting and Cleaning
Remove the ceramic shell, separate castings from the runner system and clean residual refractory material. Carry out suitable gate removal, grinding or surface cleaning operations while protecting critical cast surfaces. Inspect the parts for visible defects before further processing.
9. Heat Treatment, Machining and Inspection
Carry out specified heat treatment, CNC turning, milling, drilling or surface finishing where required. Check dimensions, alloy condition, surface quality and functional interfaces against the approved drawing. Material certificates, mechanical tests and non-destructive examination reports are provided when specified by the agreed inspection plan; accepted parts are then identified and packaged for delivery.
Investment Casting Materials & Alloy Grades
Steel Alloys for Custom Investment Castings
SIMIS focuses on custom investment castings in carbon steel, alloy steel, stainless steel and selected heat-resistant cast steels. The production route, alloy grade and applicable specification are reviewed together with the drawing, mechanical properties, operating conditions and required inspection. The grades below are examples already referenced on this page, not a guarantee that every grade is available on every line.
| Material category | Representative casting grades / specifications | Typical investment-cast OEM parts |
|---|---|---|
| Carbon cast steel | ASTM A216 WCB / WCC, subject to casting-route review | Valve components, brackets, pump parts and industrial fittings |
| Low- and medium-alloy cast steel | ASTM A217 WC6 / WC9; specified ASTM A148 grades | Structural connectors, levers, machinery parts and power-equipment components |
| Stainless cast steel | ASTM A351 CF8 / CF8M / CF3M; ASTM A743 CA6NM | Valve and pump components, pipe fittings, marine and process-equipment parts |
| Heat-resistant cast steel | Selected ASTM A297 grades such as HK / HT / HU, subject to technical confirmation | Furnace fixtures, exhaust-system and other high-temperature components |
For material-specific manufacturing options, see Steel Casting. For critical machined dimensions, see our CNC Machining services. Submit the material grade, drawing, estimated quantity and inspection requirements for a quotation.