Custom Pressure Die Casting Manufacturer in China
Custom Pressure Die Casting Services & Manufacturing Capabilities
SIMIS High-Pressure Die Casting Manufacturing Capabilities
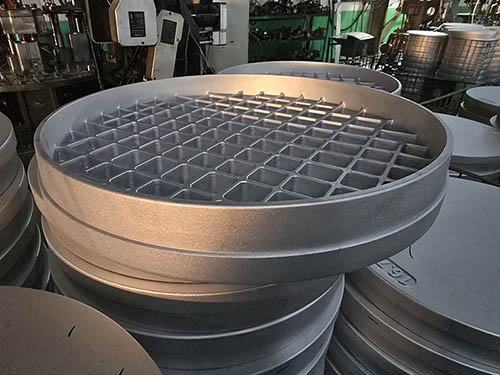
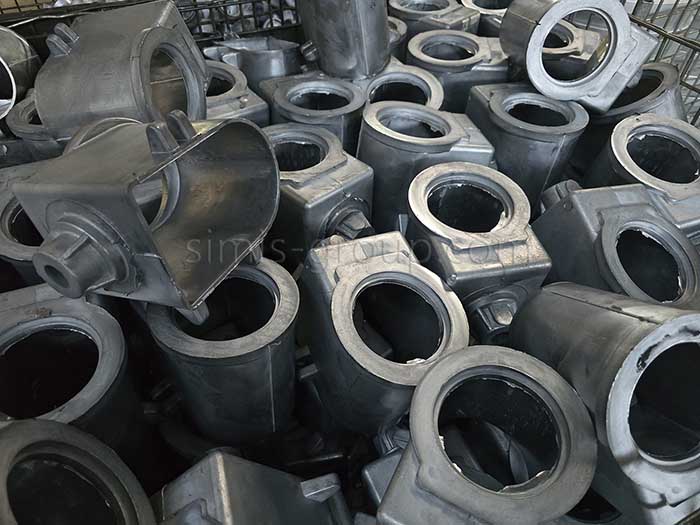
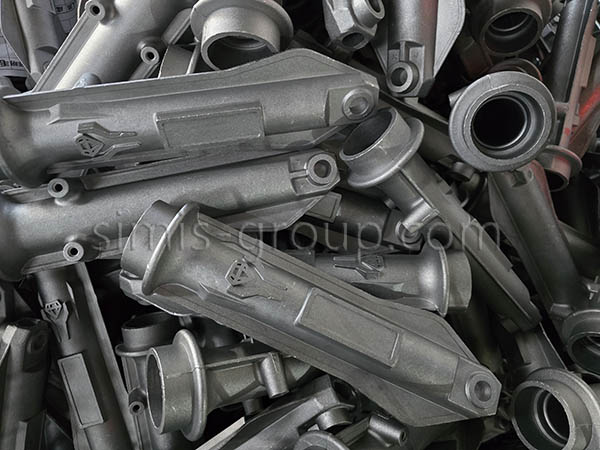
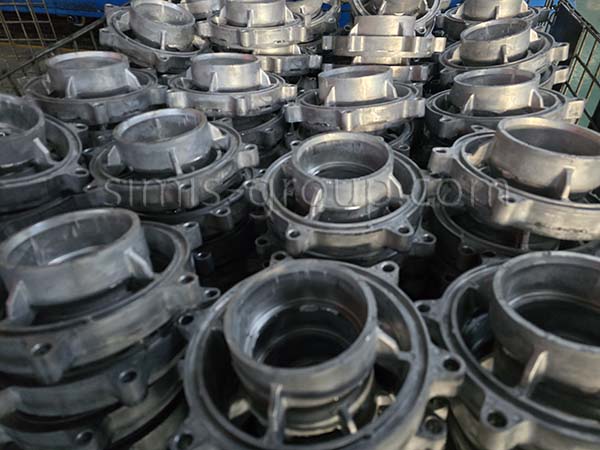
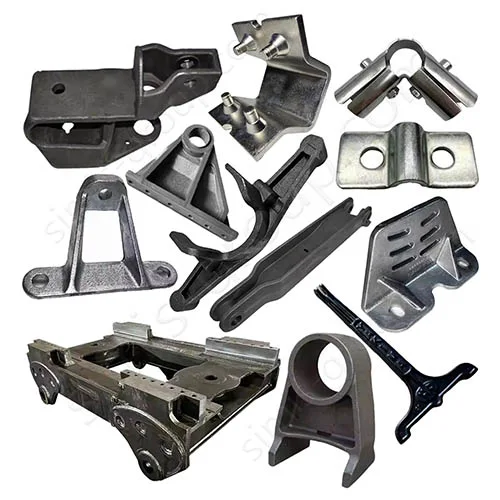
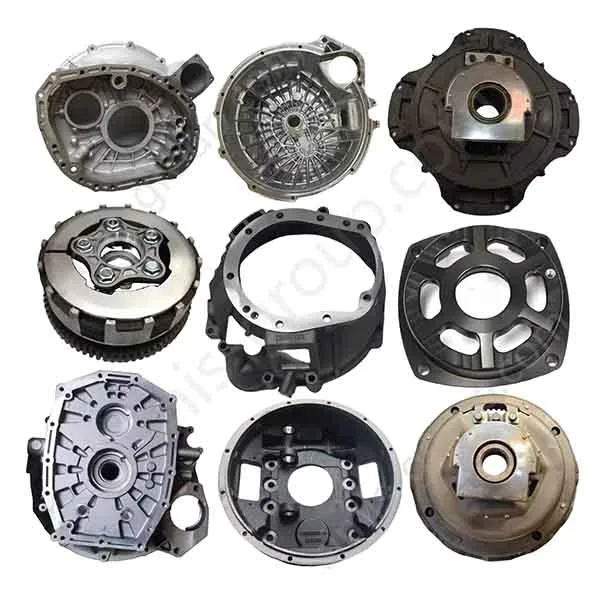
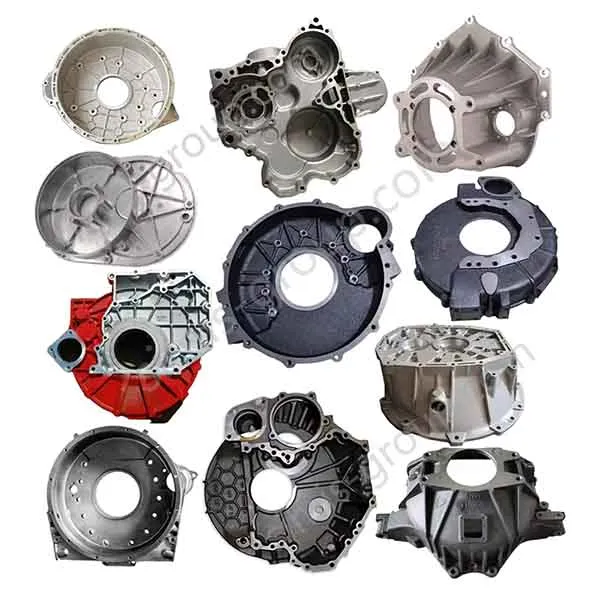
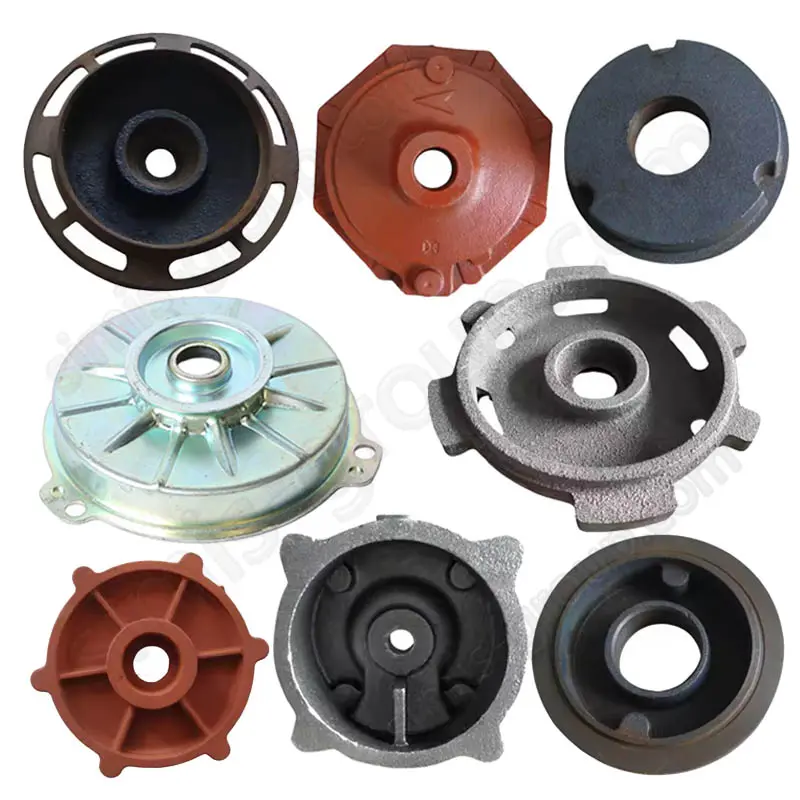
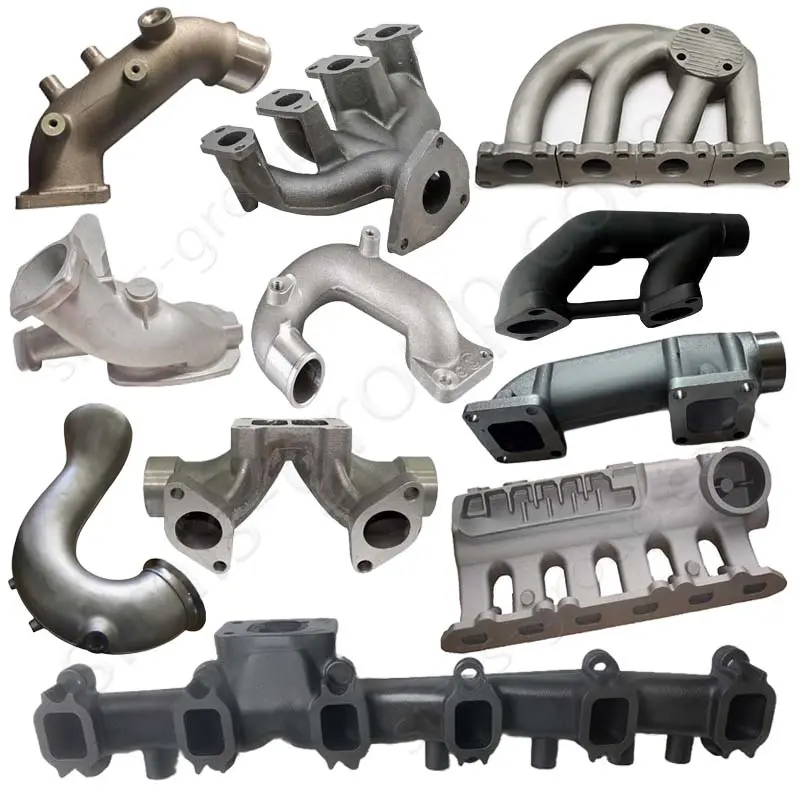
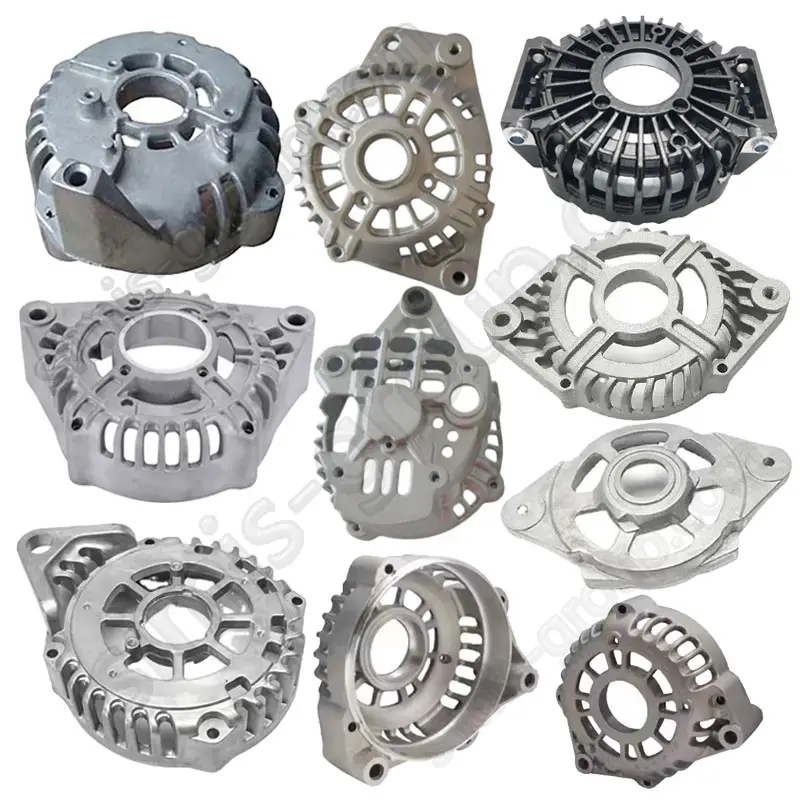
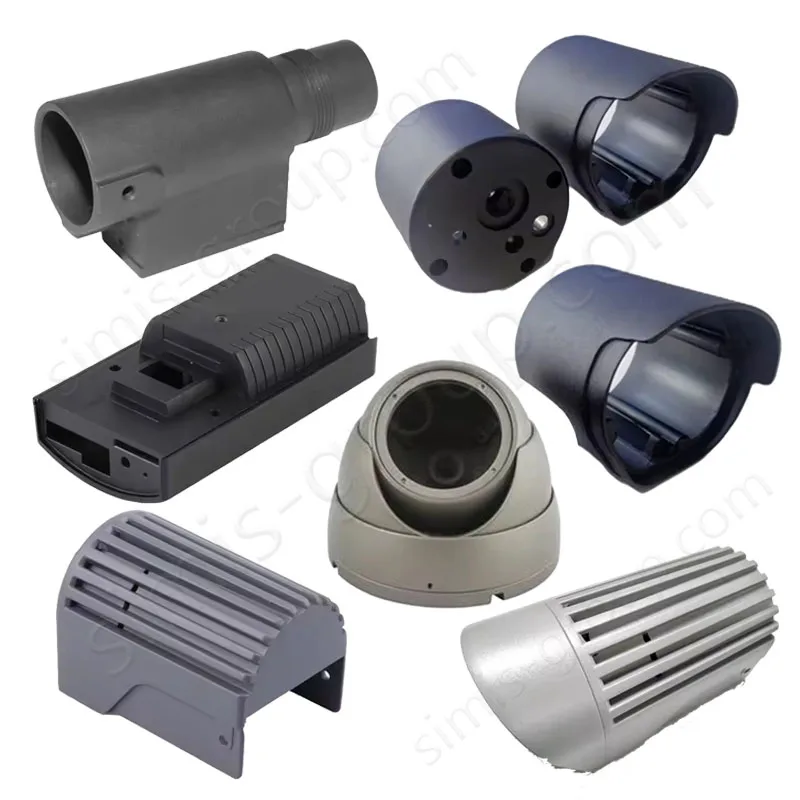
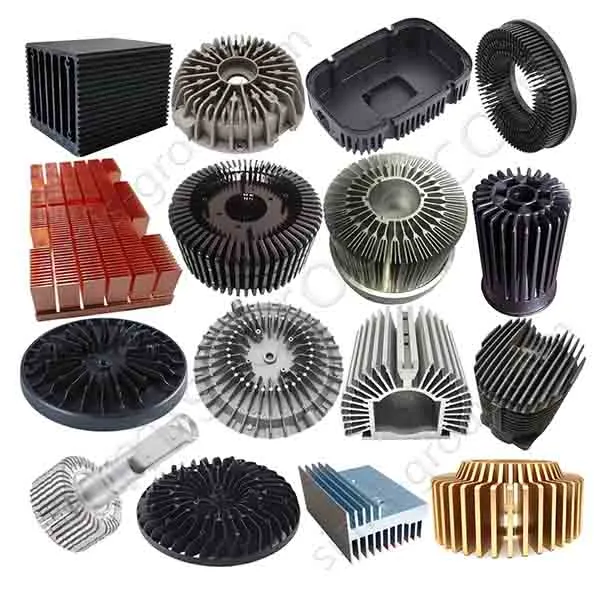
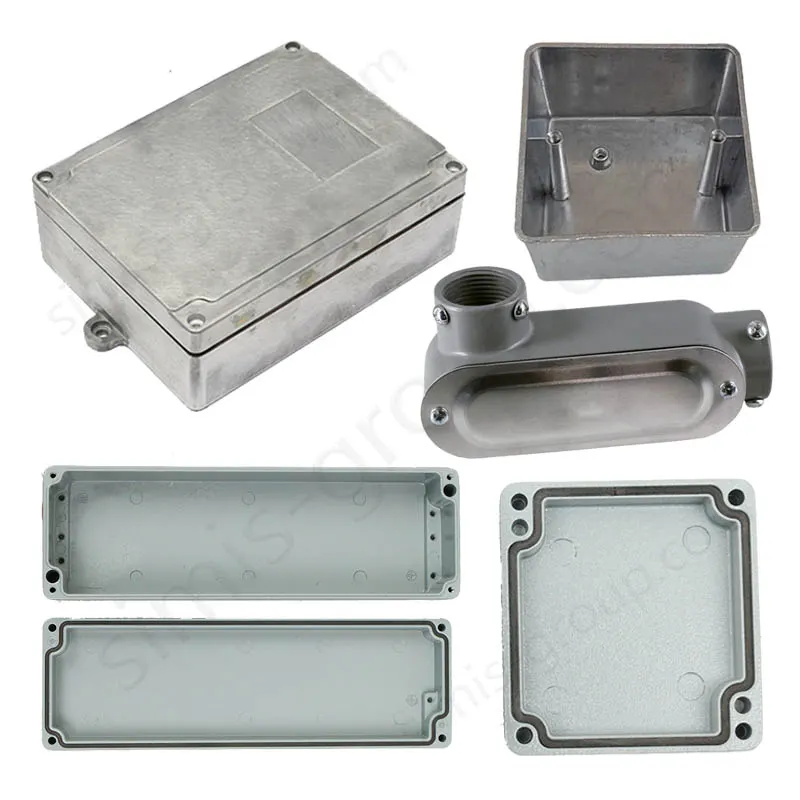
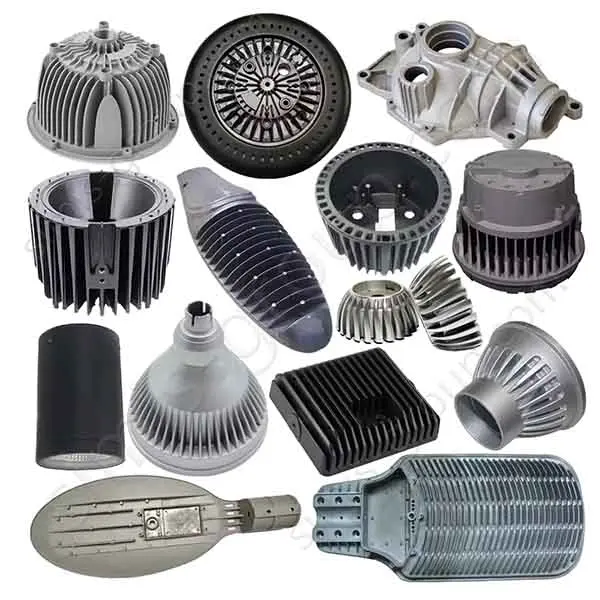
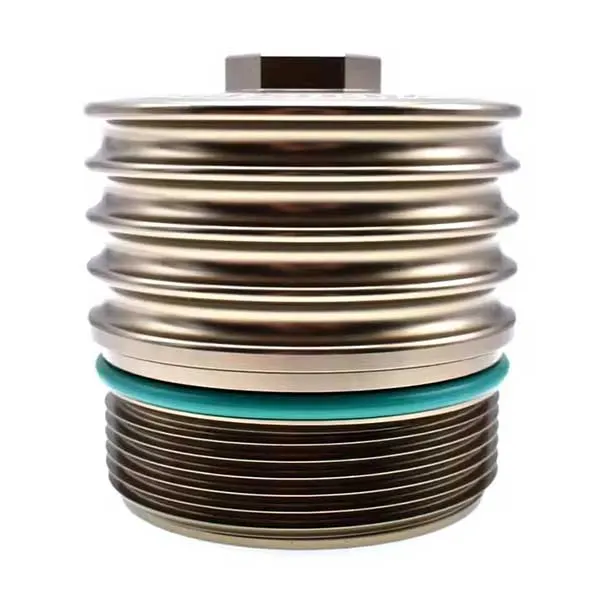
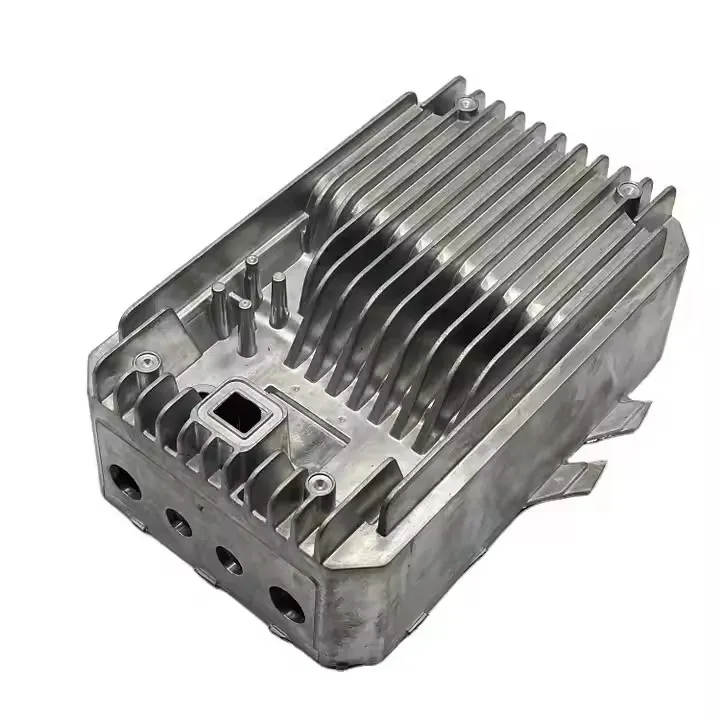
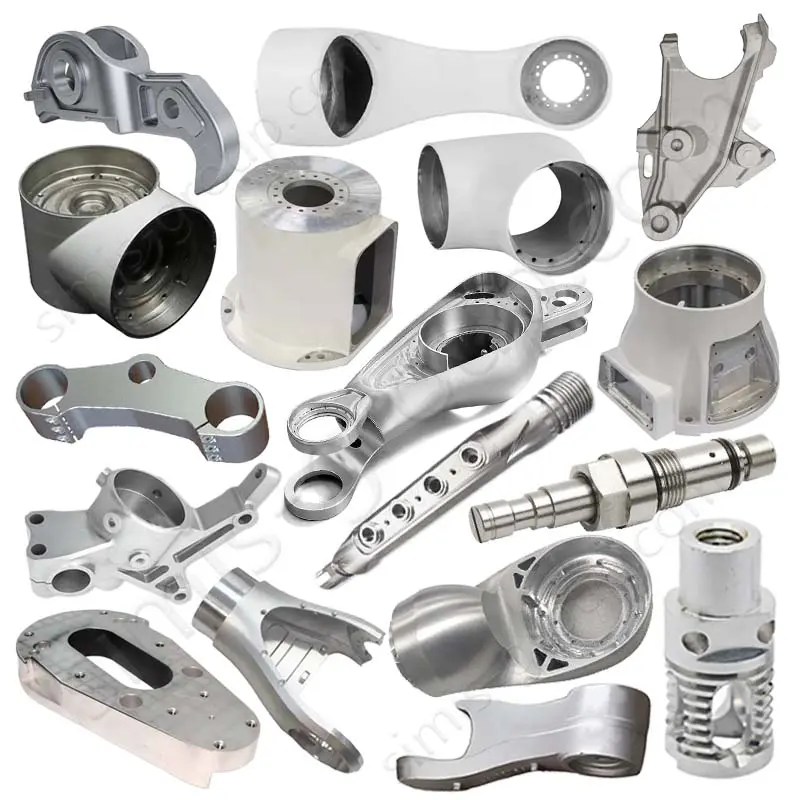
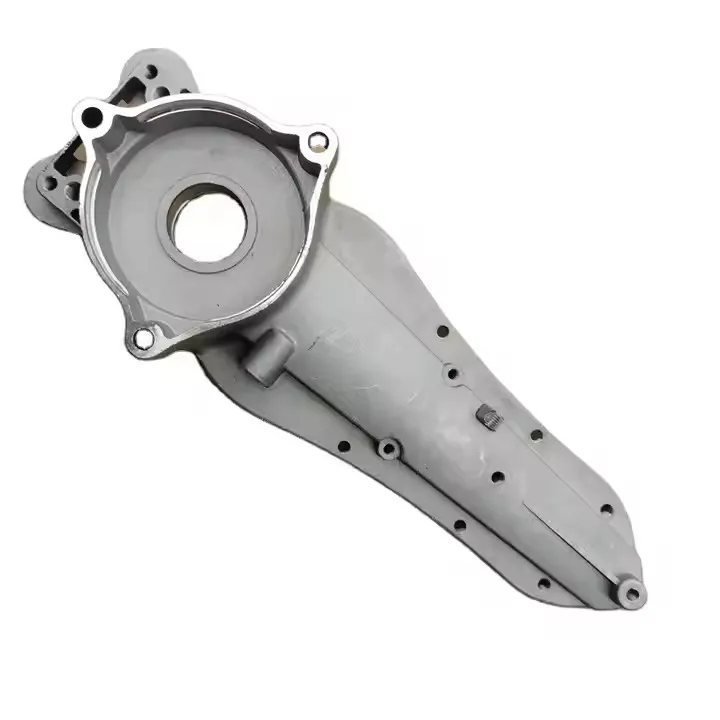
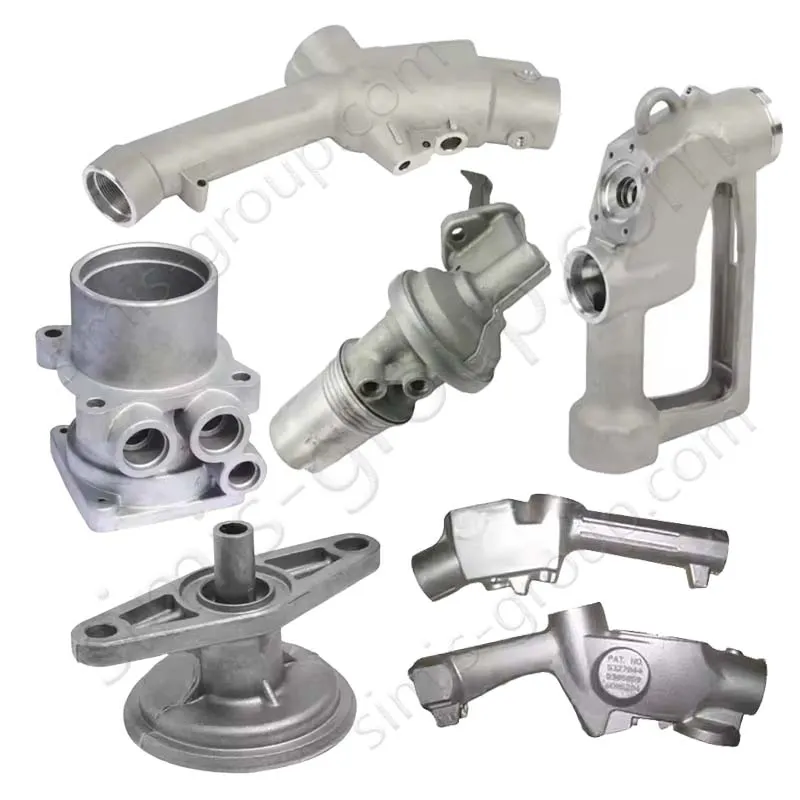
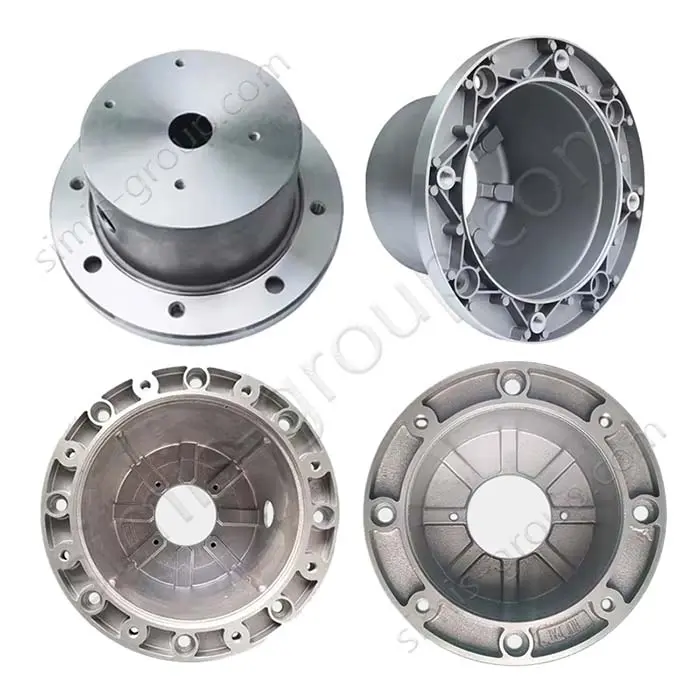
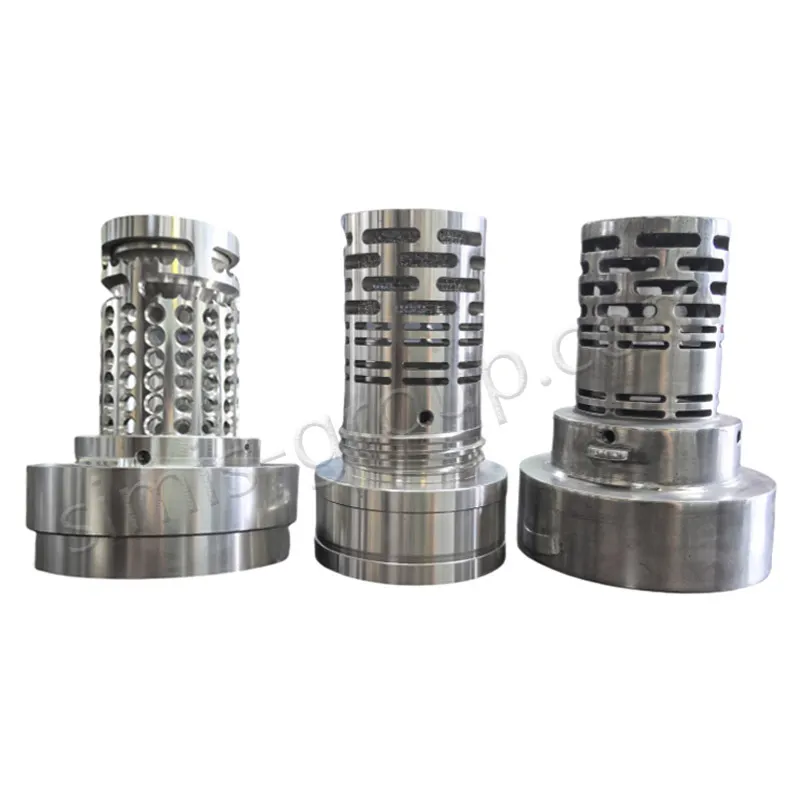
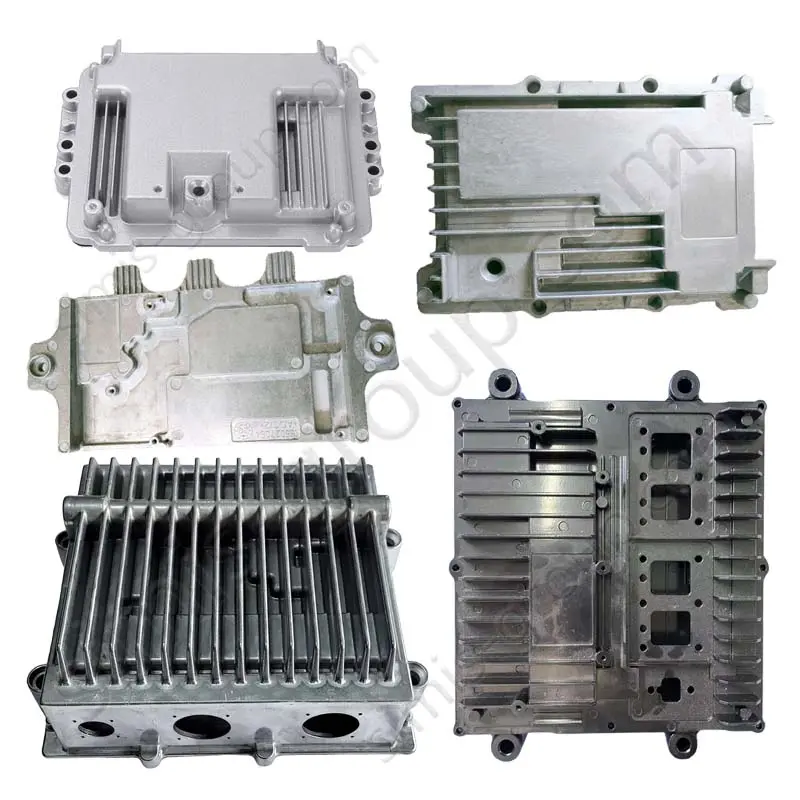
SIMIS provides custom high-pressure die casting for aluminum and zinc alloy OEM components manufactured from customer drawings. Aluminum parts are produced using cold-chamber machines, while zinc alloy parts can use suitable hot-chamber equipment. Typical products include lighting housings, heat sinks, electrical enclosures, gearbox covers, brackets and other industrial parts. Die design, casting, trimming, CNC machining and finishing are coordinated according to each project.
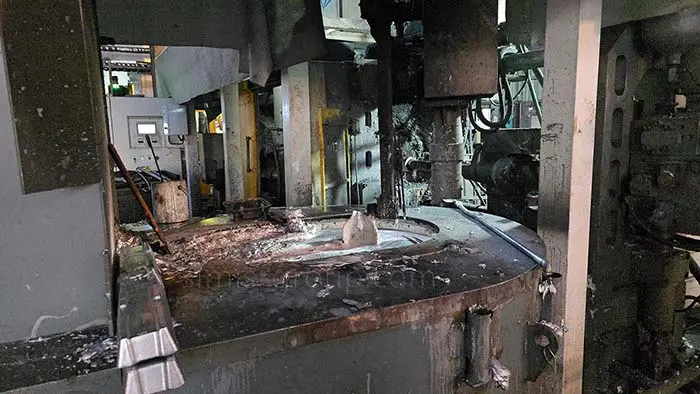
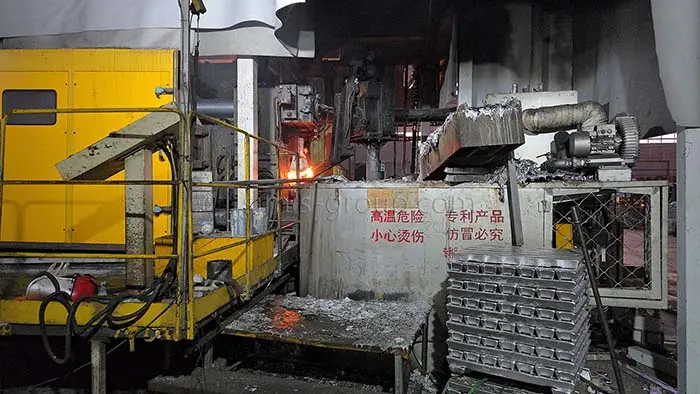
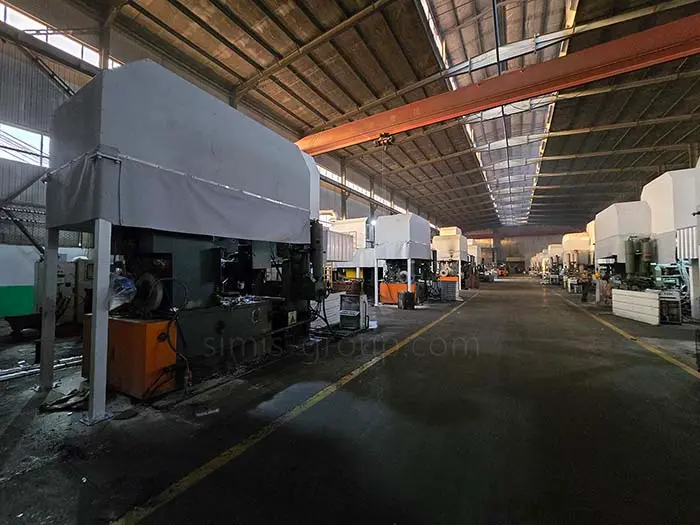
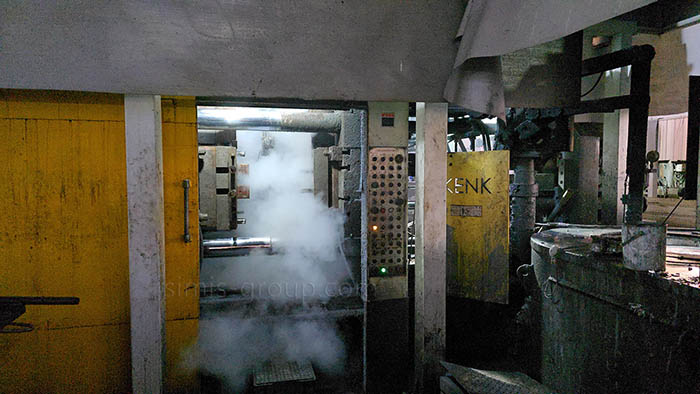
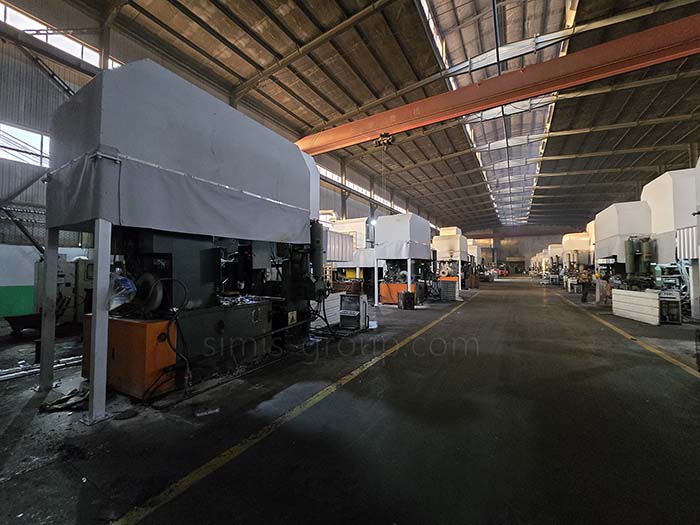
Our current equipment list includes cold-chamber die casting machines rated at 280, 500, 800, 1,250 and 1,600 tonnes, and hot-chamber machines rated at 88, 160 and 280 tonnes. Supporting operations include alloy melting and holding, die-temperature control, automated handling, trimming and surface preparation. Machine suitability is evaluated against projected casting area, part geometry, wall sections, alloy and production volume.
| Die casting route | Machine clamping force | Reference part weight | Precision / finish reference |
|---|---|---|---|
| Aluminum alloy, cold chamber | 280–1,600 tonnes (listed machines) | 0.02–10 kg (Aluminum Casting page) | CT4–CT6; Ra 0.8–3.2 μm (material-page references) |
| Zinc alloy, hot chamber | 88–280 tonnes (listed machines) | Confirm for each part and machine | Drawing-specific dimensional and surface requirements |
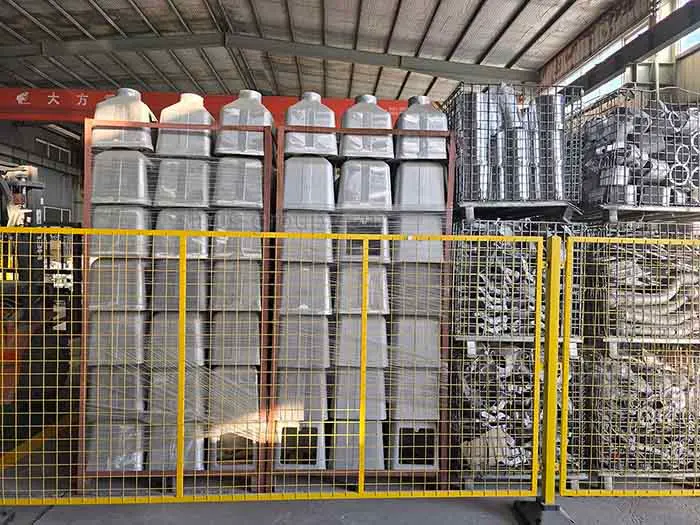
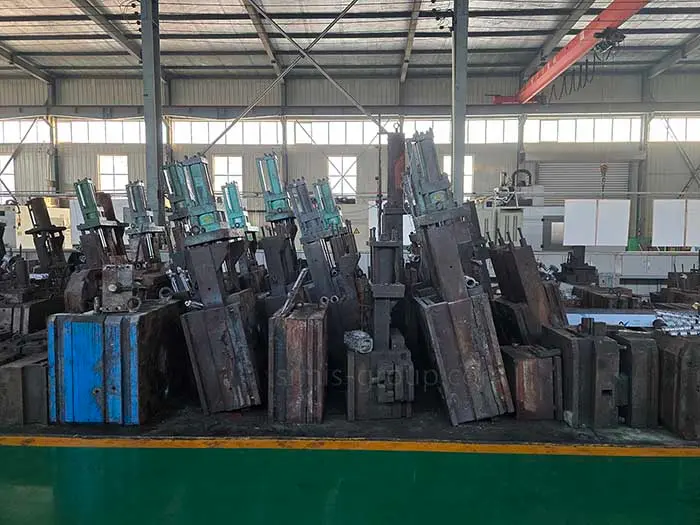
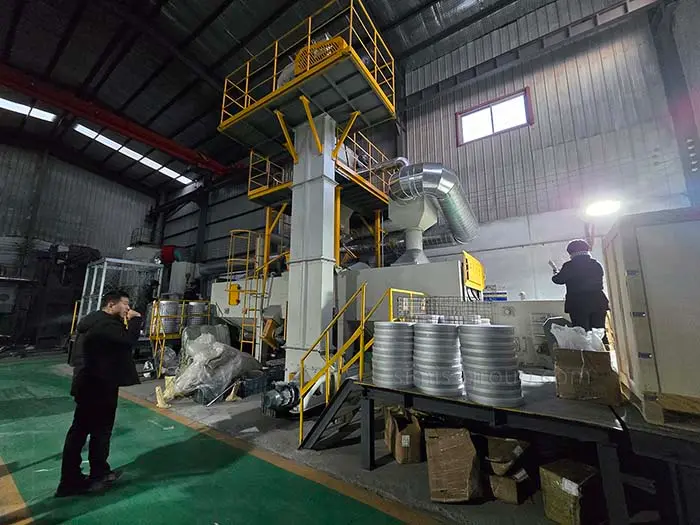
OEM Die Castings & Custom Metal Parts





Pressure Die Casting Process & Quality Control
High-Pressure Die Casting Process Overview
SIMIS coordinates high-pressure die casting from drawing review and tooling through alloy preparation, controlled injection, trimming, machining and inspection. The selected route depends on alloy type: cold-chamber machines are used for aluminum alloys, while suitable zinc alloys can be processed on hot-chamber machines. Die filling, venting, solidification and critical machining surfaces are reviewed against the part specification and planned batch quantity.
1. Die Design and Engineering Review
Assess the customer drawing, alloy grade, projected casting area, wall thickness, draft angles, undercuts and required annual volume. Review die parting, sliders, ejector locations, gates, overflows and venting. Critical machined surfaces and inspection datums are identified before die design is approved.
2. Die Manufacturing and Verification
Manufacture or coordinate the die inserts and mold components using approved tool-steel specifications, machining and heat treatment as required. Check cavity geometry, cooling channels, alignment and moving components before production trials. Tooling changes are recorded and agreed with the customer when they affect the approved part design.
3. Alloy Melting and Preparation
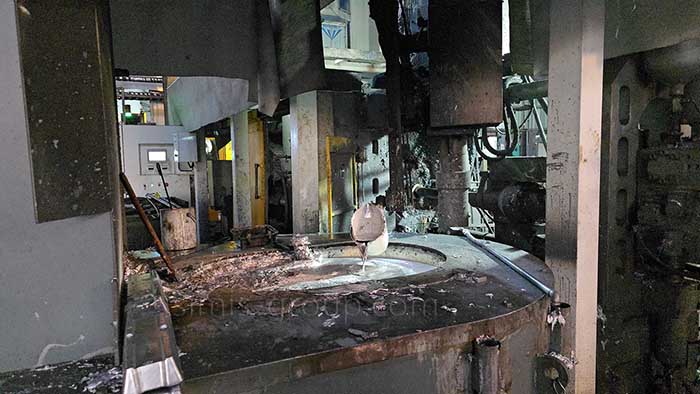
Prepare the specified aluminum or zinc die-casting alloy and confirm its material requirements before production. Control melting and holding conditions, temperature and melt handling according to the selected alloy and equipment. Material composition, contamination controls and any required records are defined by the project specification.
4. High-Pressure Injection and Die Filling
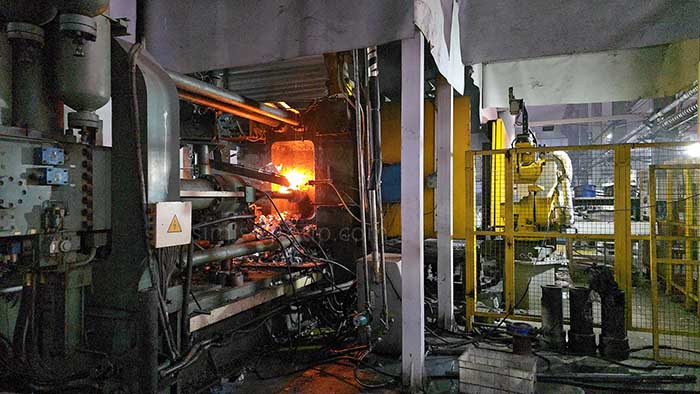
Inject molten alloy into the closed steel die using the selected cold- or hot-chamber process. Control the shot profile, die temperature, filling, pressure and venting to promote consistent castings and reduce avoidable gas entrapment. Final porosity limits, where required, are agreed in advance; high-pressure die casting does not guarantee zero internal pores.
5. Cooling and Solidification
Hold the casting in the die while the alloy solidifies under the selected cycle conditions. Monitor die temperature, cooling time and process consistency to manage shrinkage, distortion and surface condition. Settings are adjusted according to casting geometry, wall thickness and alloy rather than applying one fixed cycle to every component.
6. Ejection, Trimming and Deburring
Open the die, eject the casting and remove gates, runners, overflows and flash by trimming and suitable finishing operations. Inspect visible surfaces, ejection marks and dimensional features before subsequent machining. Cleaning and trimming improve external condition but do not eliminate internal casting porosity.
7. CNC Machining and Surface Finishing
Perform specified machining of threads, mounting faces, bores and other functional features. Depending on the alloy and drawing, suitable finishing may include blasting, polishing, painting, powder coating or approved conversion treatments. Heat treatment is evaluated separately: conventional high-pressure die castings are not automatically suitable for full solution treatment and T6 tempering.
8. Final Inspection and Approval
Inspect die castings against the released drawing and agreed quality plan. Typical checks cover dimensions, appearance, machined interfaces and alloy requirements. For sealed or critical parts, leak testing, X-ray or CT examination, and defined porosity acceptance criteria may be specified. The inspection scope and records are established for each order.
Pressure Die Casting Materials & Alloy Grades
Aluminum & Zinc Alloys for Custom Die Castings
SIMIS focuses its routine pressure die casting description on aluminum and zinc alloys for custom housings, connectors, brackets and machinery components. The final alloy is selected according to the customer drawing, strength requirements, casting design, corrosion environment and expected volume. Representative grades below are examples for engineering review, not a promise that every grade is available on every machine.
| Material category | Representative grades / route | Typical OEM applications |
|---|---|---|
| Aluminum die-casting alloys | A380, A383 and customer-specified equivalent grades; cold-chamber route, subject to project approval | Motor and gearbox housings, electronic enclosures, heat sinks, lighting parts and brackets |
| Zinc die-casting alloys | Zamak 3, Zamak 5 and selected ZA grades; hot-chamber suitability confirmed by alloy and equipment | Small fittings, connectors, instrument housings and precision hardware |
| Magnesium die-casting alloys | AZ91D or AM60 may be evaluated only after confirming dedicated melting, handling and machine capability; AZ31 is not presented as a routine HPDC grade | Selected lightweight housing or structural components where an appropriate qualified production route exists |
| Copper alloys | Specified brass or bronze grades; do not assume ordinary aluminum/zinc die casting equipment is suitable | Valve, pump or connector components may instead require copper alloy casting routes |
For related OEM manufacturing options, see our Aluminum Casting, Gravity Permanent Mold Casting and CNC Machining services. Send your 2D/3D drawings, specified alloy, critical dimensions, surface requirements and estimated quantity for a manufacturing review and quotation.