Custom Ring Rolling & Ring Forging Factory in China
Custom Ring Rolling & Ring Forging Services
SIMIS Ring Rolling & Ring Forging Manufacturing Capabilities
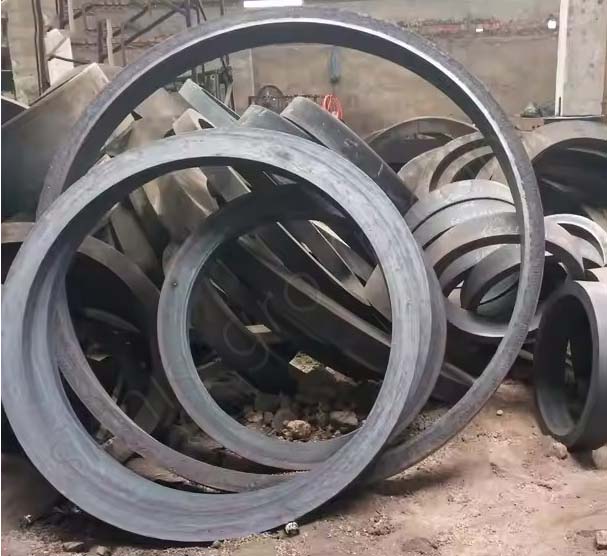
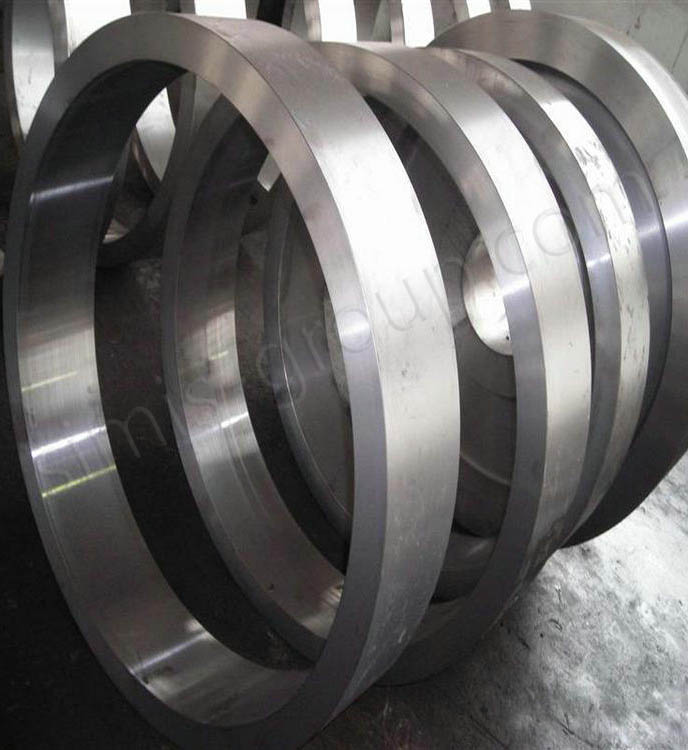
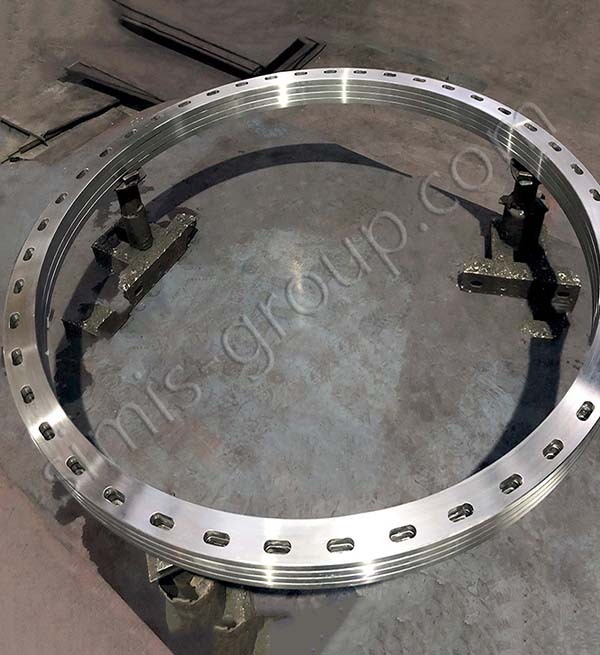
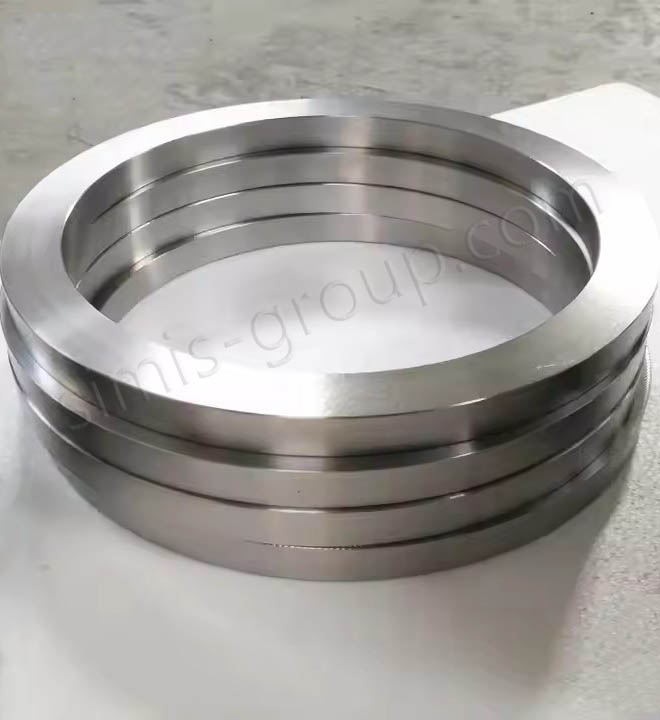
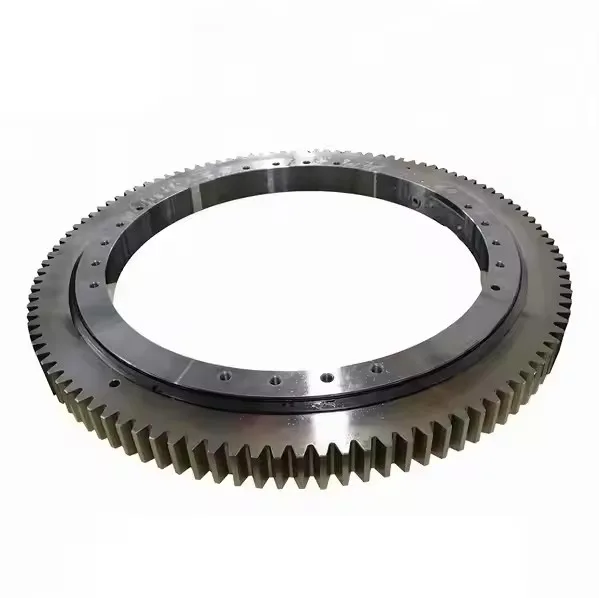
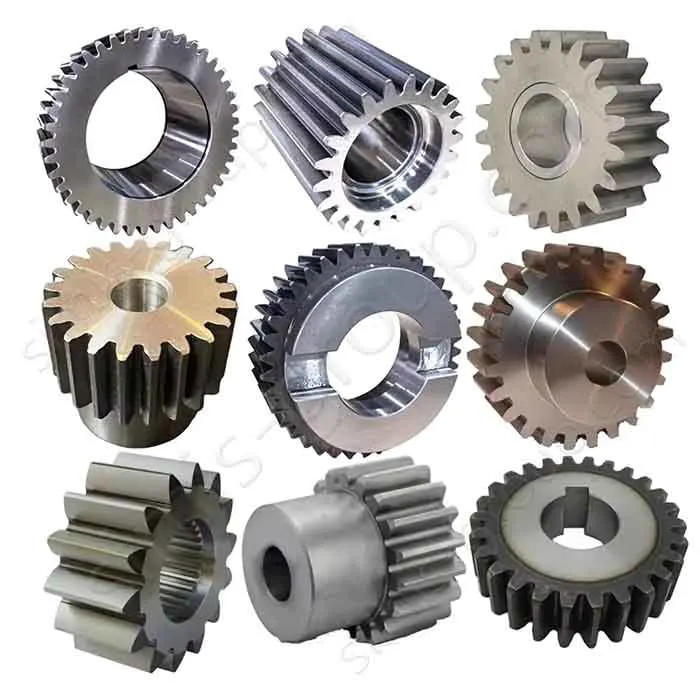
SIMIS manufactures custom seamless rolled rings and ring forgings for OEM industrial equipment from customer drawings. Our published process scope covers radial–axial ring rolling, hydraulic preform forging, material-specific heat treatment, CNC turning and dimensional inspection. Typical components include bearing and slewing rings, gear-ring blanks, flanges and heavy-duty annular parts. Final properties and finished tolerances depend on the alloy, forming schedule, heat treatment and machining specification.
| Equipment / capability | SIMIS reference |
|---|---|
| Radial–axial ring rolling mill | Outside diameter Ø300–2,500 mm |
| Rolled-ring wall thickness | 30–400 mm |
| Ring height | Up to 400 mm |
| Individual ring weight | 10–1,500 kg |
| Hydraulic forging presses | 1,000–3,000 tons |
| Heating / soaking furnaces | 3–5-ton stated furnace load; ±5°C stated temperature control |
| Handling and heat treatment | 5–10-ton lifting capacity; air-circulation/pit furnaces and quench media listed |
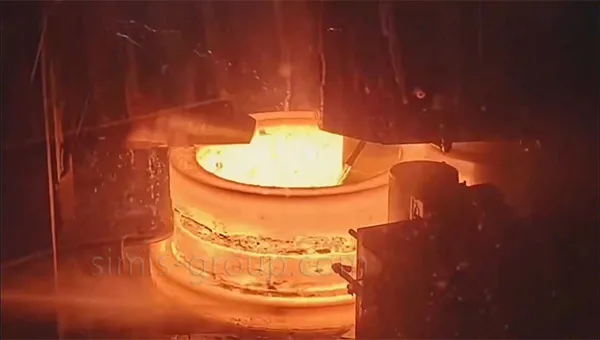
Custom Seamless Rolled Rings & OEM Forged Parts
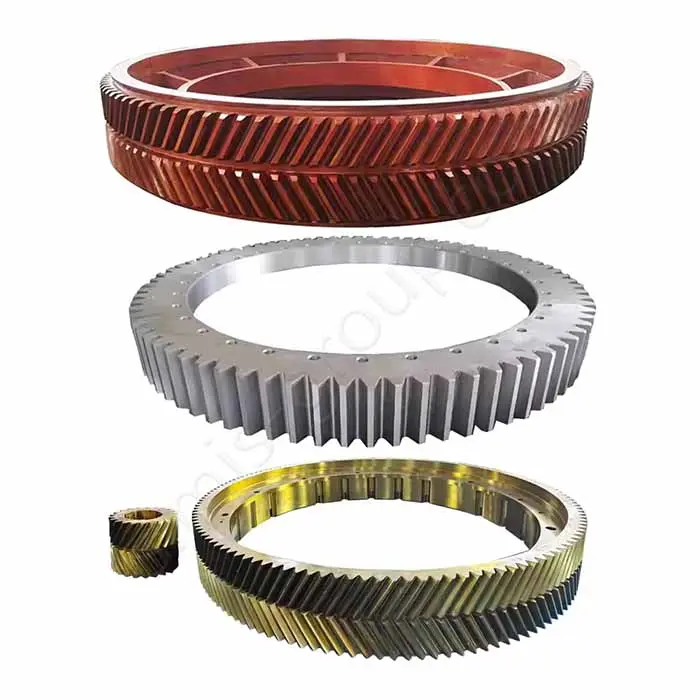

Ring Rolling Production Process & Quality Control
Ring Rolling Process Overview
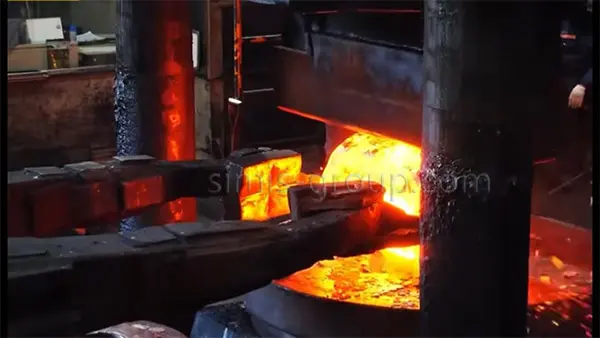
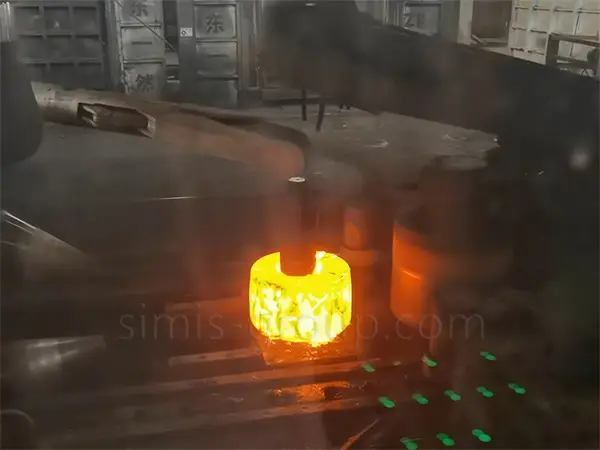
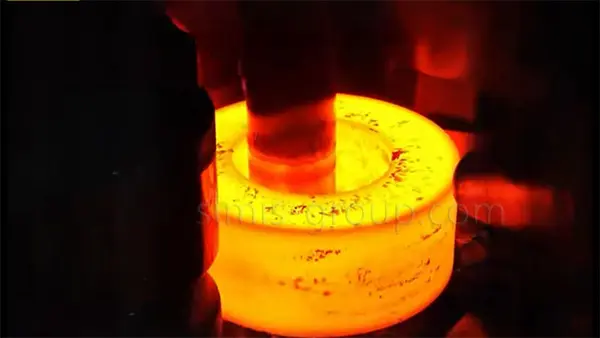
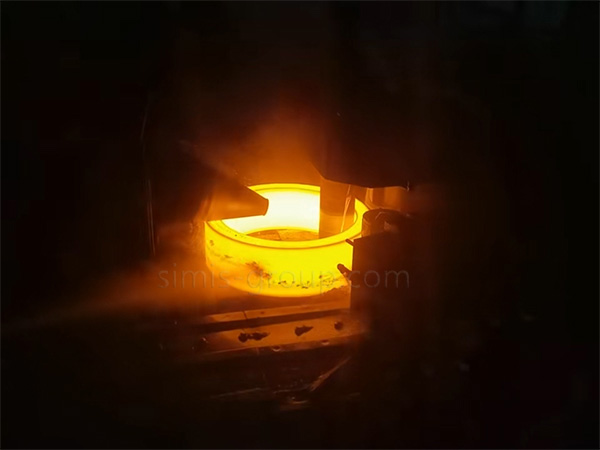
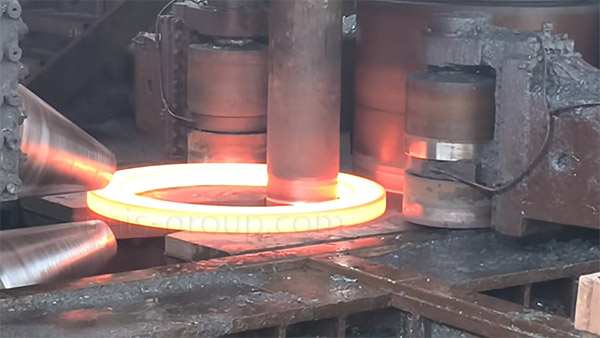
SIMIS ring rolling begins with a traceable billet selected for the required grade, dimensions and final mechanical properties. The billet is heated, upset and pierced to create an annular preform. Radial–axial rolling then reduces the ring cross-section through repeated rotation between the main roll, mandrel and axial rolls while increasing the ring diameter.
1. Material Review and Billet Preparation
Review the customer drawing, target alloy, outside and inside diameters, ring height, machining allowances and required mechanical properties. Choose a suitable ingot, bloom or bar-derived billet and calculate the starting material volume for upsetting, piercing and ring expansion.
Check raw-material identification and supporting documentation for the specified grade. Billet preparation may include sawing, surface conditioning or removal of defects. Carbon steel, alloy steel and stainless steel are reviewed against their own forging temperatures and processing requirements.
2. Billet Heating and Temperature Control
Heat the prepared billet to the approved hot-working range for its alloy and section size. Allow sufficient soaking for the required temperature distribution, and avoid unnecessary overheating, excessive scale or temperature loss before forging. Heat-up and handling conditions are selected according to billet mass and furnace loading.
3. Upsetting, Piercing and Ring Preforming
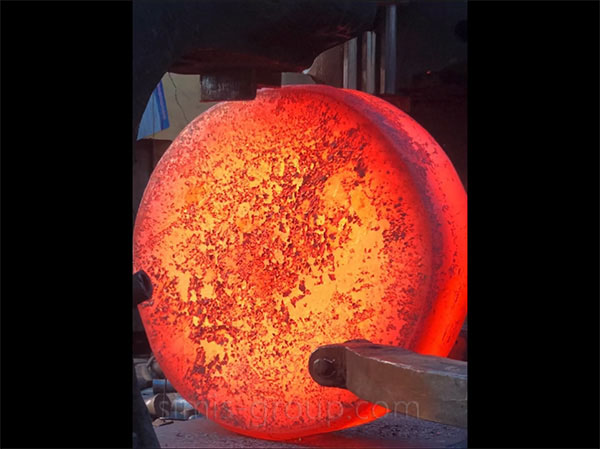
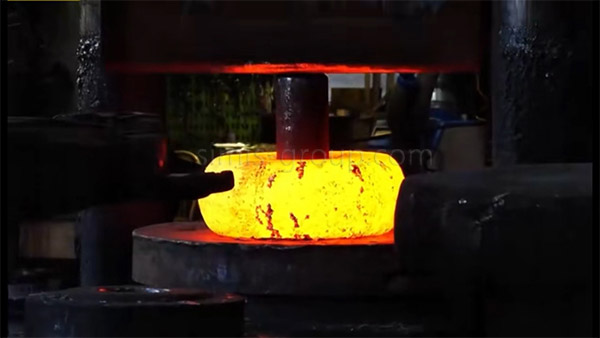
Upset the heated billet under a suitable hydraulic forging press to create a compact disc or preform. Punch or pierce the central opening, then remove the remaining web where necessary to obtain a complete through-hole. Adjust the preform outside diameter, bore and height for stable entry into the ring-rolling mill.
Upsetting and piercing are preparation for ring rolling, not an alternative description of the final rolling pass. Control concentricity, preform volume, surface condition and temperature so the ring can expand without excessive instability or machining allowance.
4. Radial–Axial Ring Rolling
Place the annular preform over the mandrel of the radial–axial ring rolling mill. As the ring rotates, the main roll and mandrel progressively reduce its radial wall thickness, causing the inner and outer diameters to increase. The axial rolls control the ring height and section profile during expansion.
Adjust roll feed, ring rotation, guiding and temperature according to the approved rolling schedule. Monitor outside diameter, wall thickness, height, circularity and surface defects. This is radial–axial ring rolling; it should not be confused with forming a ring solely by open- or closed-die pressing.
5. Controlled Cooling and Dimensional Checks
After rolling, transfer the hot ring using suitable handling equipment and apply the approved cooling practice. Air cooling, insulated cooling or another controlled route may be used depending on the alloy, section size and later heat-treatment plan.
Monitor distortion, ovality and the risk of cracking during handling and cooling. Record required process information and check that sufficient stock remains for subsequent turning and facing.
6. Material-Specific Heat Treatment
Apply material-specific normalizing, annealing, quenching and tempering, solution treatment or aging only where required by the specified grade and finished properties. A carbon-steel ring, alloy-steel bearing blank, stainless-steel ring and aluminum ring may each require a different treatment sequence.
Use the agreed temperature, soak time, cooling method and test requirements. Verify hardness or other mechanical properties when specified, and assess distortion before final machining.
7. Rough Machining and Precision Finishing
Remove scale and prepare the rolled ring for rough turning or other specified machining. Face the end surfaces and machine the inside and outside diameters to establish datum features and reduce the forging allowances. Additional grooves, holes, shoulders or gear features are produced only where specified in the drawing and supported by the selected machining route.
Maintain allowance for heat-treatment distortion and final sizing when the process sequence requires it. Check circularity, face runout and wall thickness during machining. As-rolled dimensions and CNC-finished tolerances must be specified separately.
8. Final Inspection and Surface Protection
Inspect the finished ring against the approved drawing and purchase specification, including material identity, outside and inside diameters, height, wall thickness, roundness, concentricity, runout, hardness and surface condition as applicable. Ultrasonic, magnetic-particle or liquid-penetrant testing may be specified by alloy, part criticality and customer acceptance criteria.
Apply corrosion protection, marking, packaging or other surface treatment only when required by the order. Release parts with the agreed dimensional records, material certificates and inspection reports. Seamless ring rolling does not by itself certify suitability for pressure-vessel, aerospace or other regulated service.
Ring Rolling Materials & Steel Alloy Grades
Steel for Custom Rolled Rings
SIMIS offer carbon steel, alloy steel, stainless steel and aluminum alloys for custom rolled rings. The selected grade must support the planned preforming and rolling temperatures, ring section, heat treatment and finished mechanical properties.
| Material category | Reference grades | Typical OEM ring components / review points |
|---|---|---|
| Carbon Steel | AISI 1045, 1050; EN C45 | General industrial rings, flanges, gear blanks and mechanical ring components; final strength and toughness follow the material and treatment specification. |
| Alloy Steel | AISI 4140, 4340; EN 42CrMo4 | Heavy-load bearing-ring blanks, wind-power or machinery flanges and high-duty rings; review hardenability, section size and heat treatment. |
| Stainless Steel | AISI 304, 316; 17-4PH | Pump, valve and chemical-equipment rings; confirm forging range, corrosion requirements and any solution/aging treatment. |
| Aluminum Alloys | 6061, 6082; 2024 and 7075 | Lightweight structural rings; alloy condition, forming temperature, final temper and section limits require separate approval. |
Seamless ring rolling can create favorable circumferential grain flow for suitable products, but strength and fatigue performance are determined by the specific alloy, reduction schedule, heat treatment, machining and acceptance tests. Material selection and part qualification should be based on the customer drawing and operating conditions.
Explore related material and finishing services: Steel Forging, Aluminum Forging, CNC Machining, Heat Treatment and Surface Treatment.