Custom Aluminum Forging Manufacturer in China
Aluminum Forging Processes & Manufacturing Capabilities
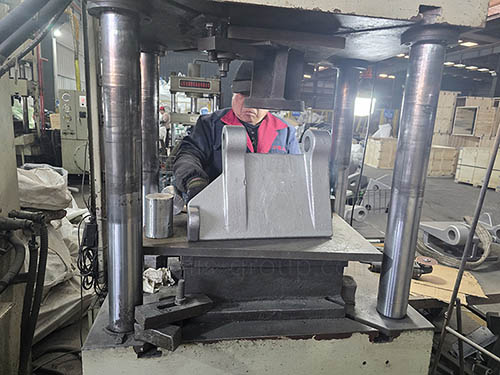
Aluminum Closed Die Forging
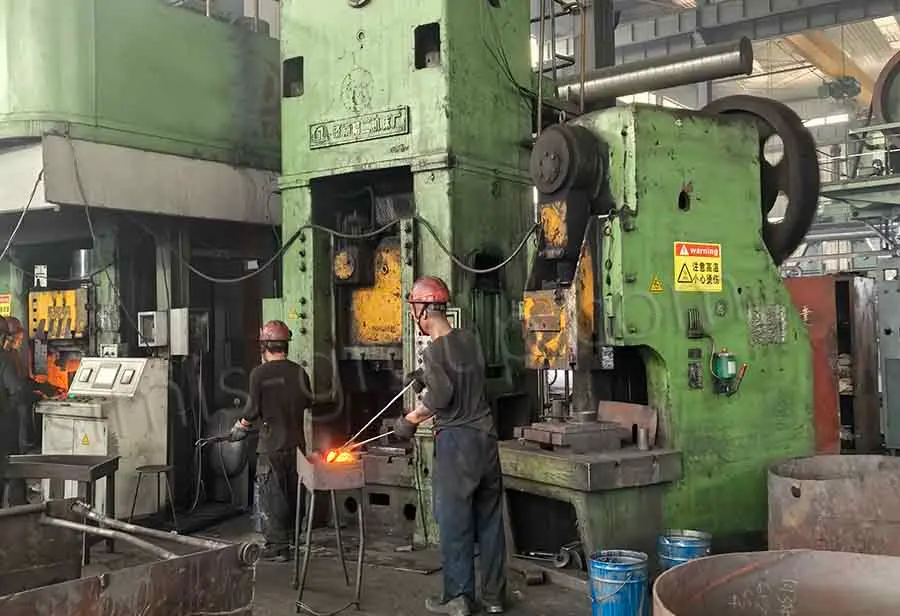
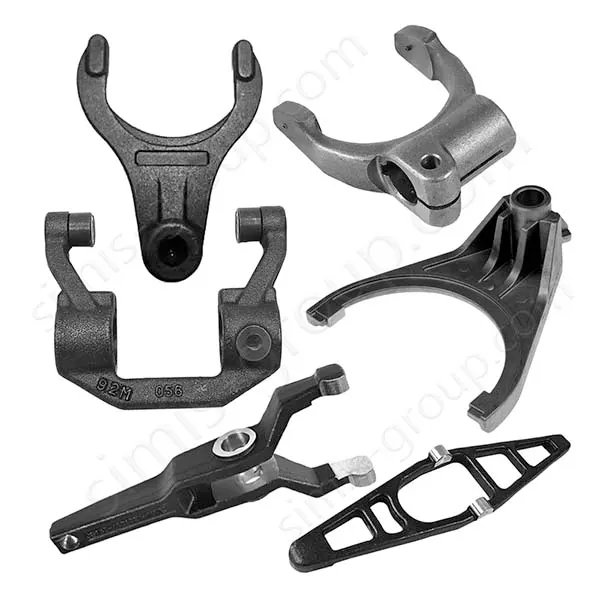
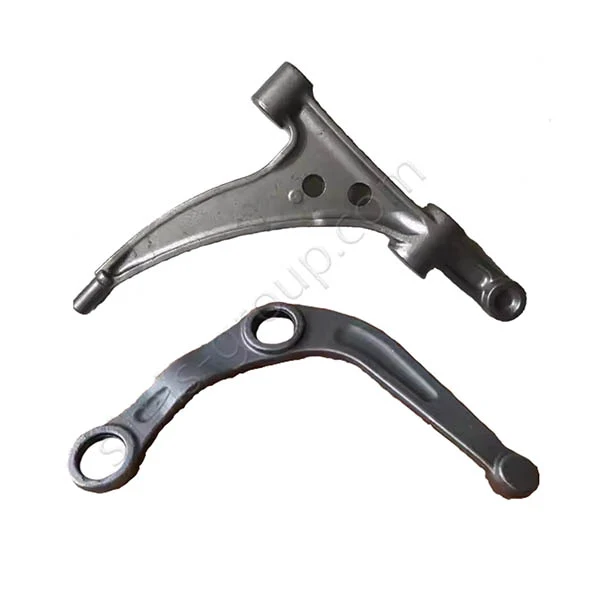
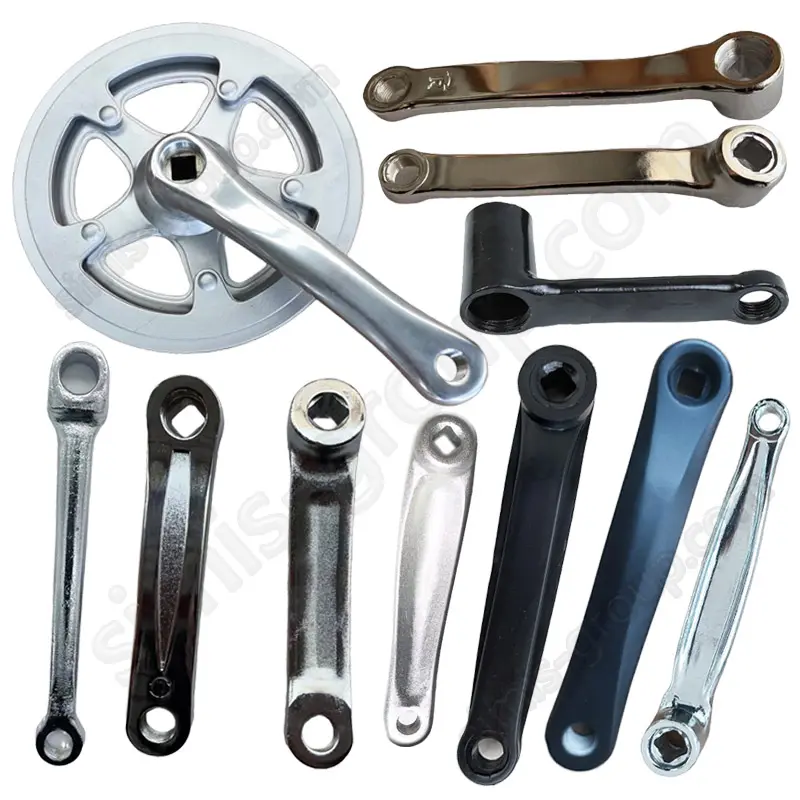
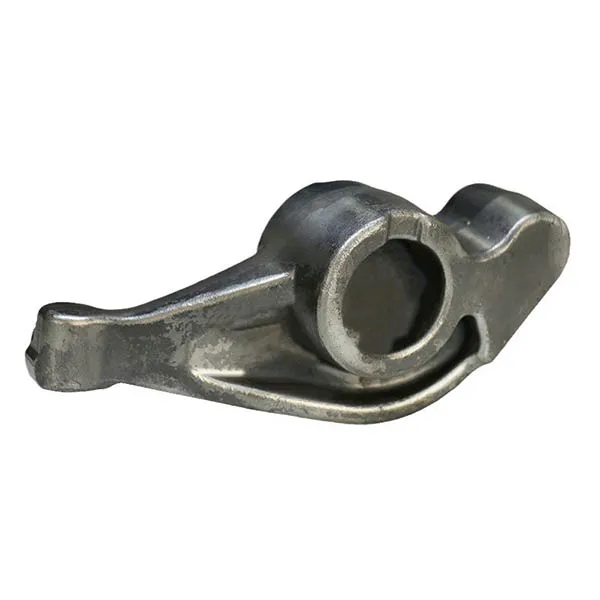
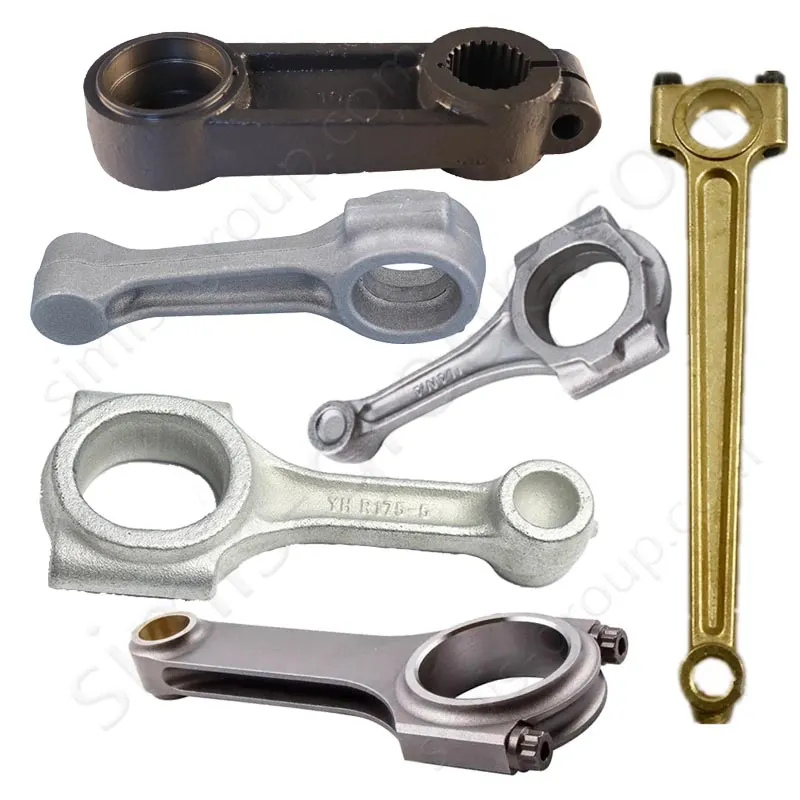
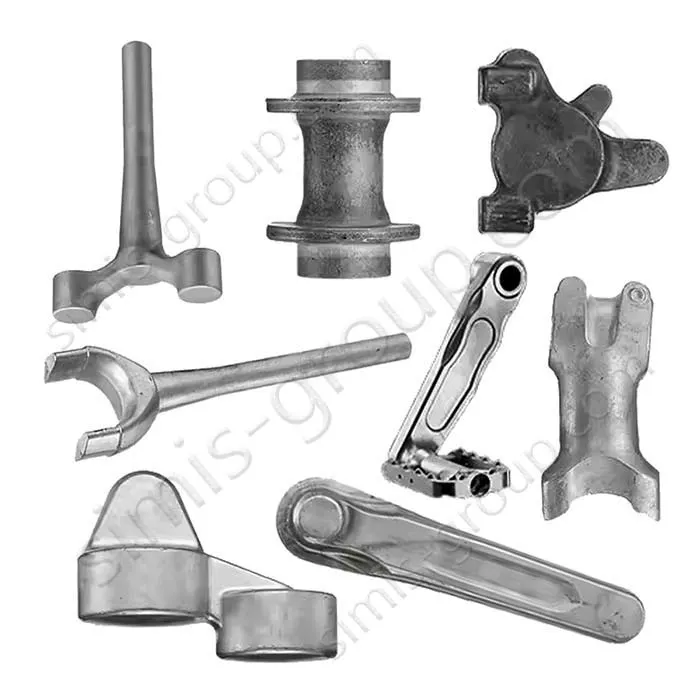
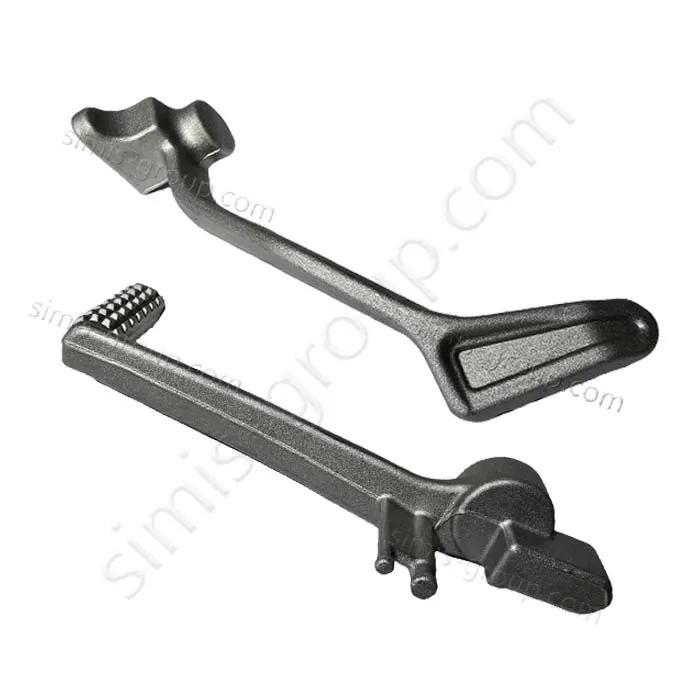
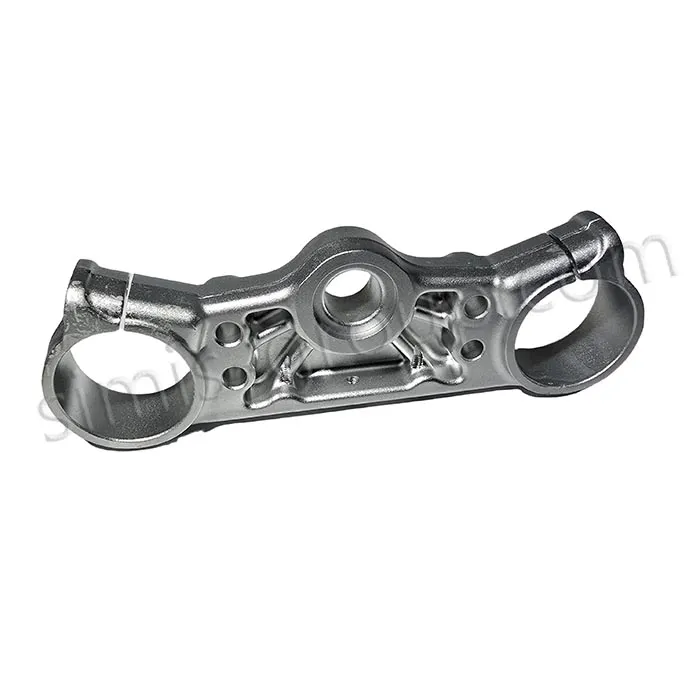
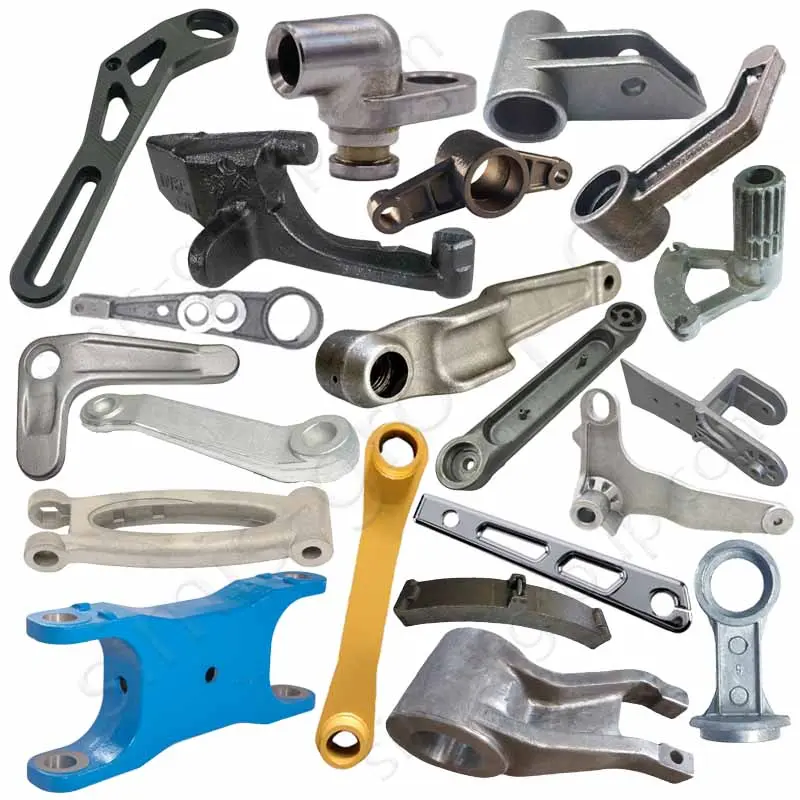
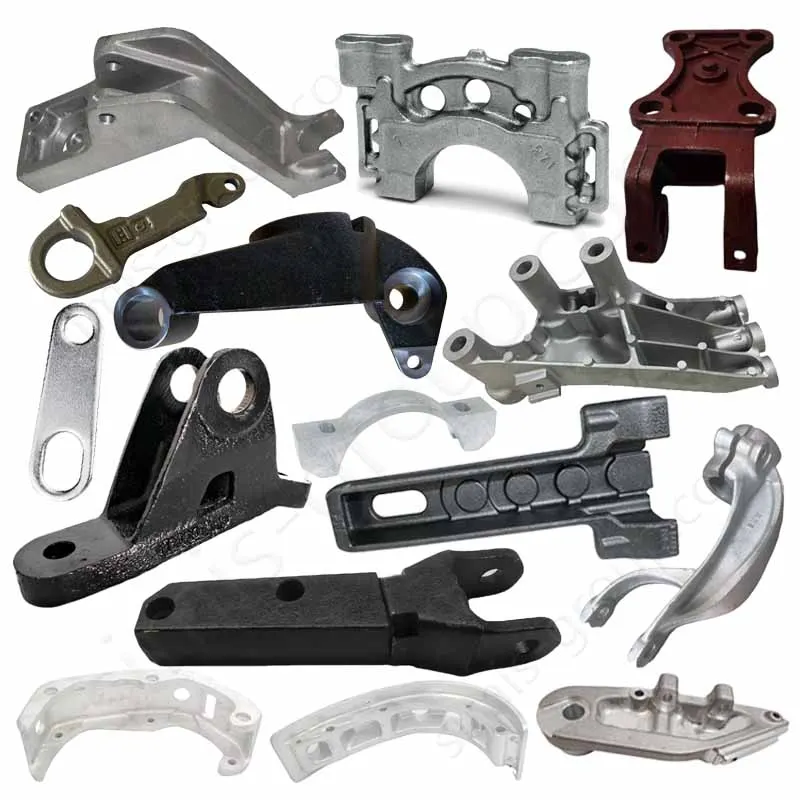
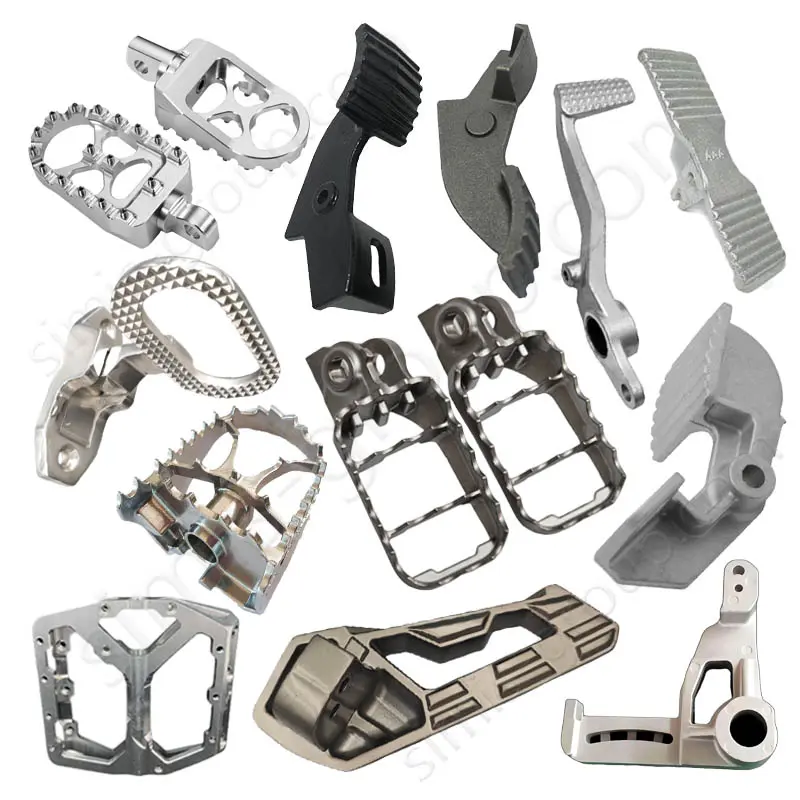
SIMIS provides custom aluminum closed-die forging for lightweight structural components such as bicycle crank arms, suspension parts, levers, brackets and other OEM forgings. We review the alloy grade, grain-flow direction, die design, production volume and final machining requirements before confirming the forming route.
Overlapping part-weight reference: 0.1–25 kg
Shared dimension reference: up to 600 × 400 × 200 mm
Closed-die press equipment: 1,600-, 2,500- and 4,000-ton presses
Machining allowance reference: 1–3 mm, subject to tooling and part design
Aluminum Ring Forging
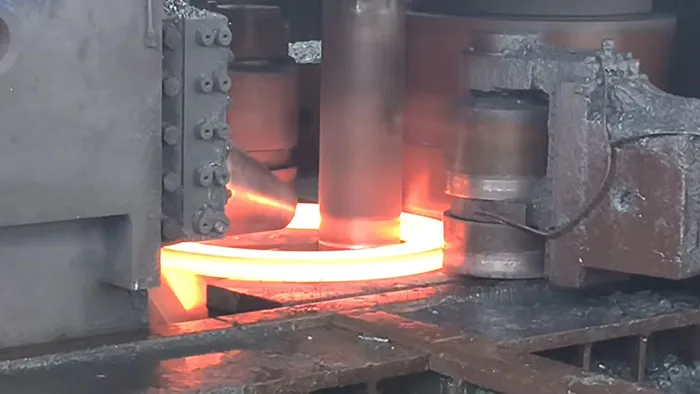
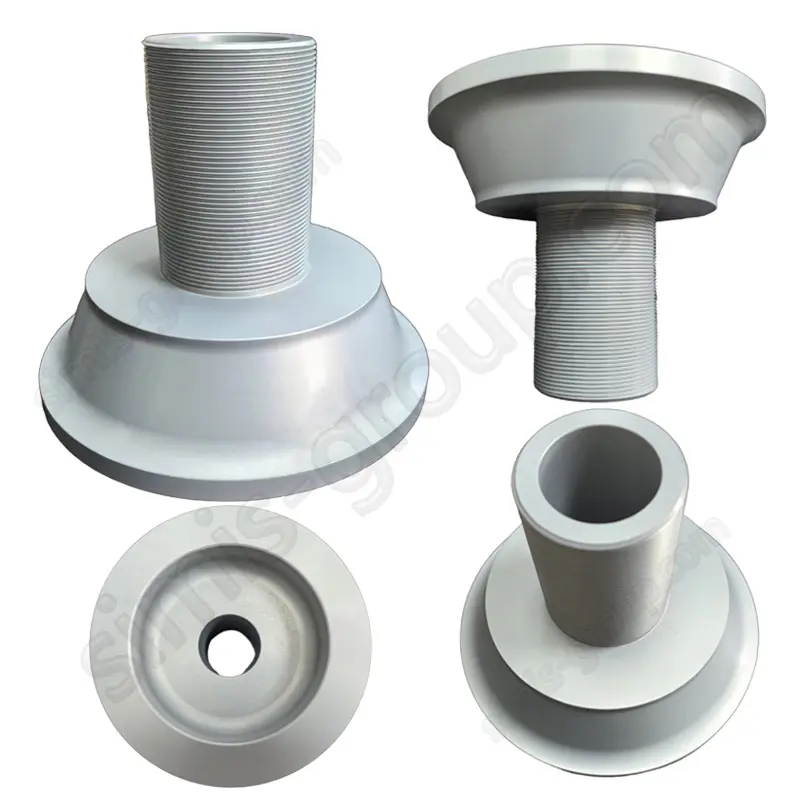
SIMIS evaluates aluminum ring rolling for seamless annular forgings used in machinery, bearing-related assemblies, flanges and lightweight rotating components. The forging plan considers the aluminum alloy, outer and inner diameters, wall section, ring height, heat-treatment condition and machining allowances.
Overlapping outer-diameter range: Ø300–Ø1,500 mm
Aluminum ring-height reference: 50–400 mm
Available route: ring rolling with subsequent heat treatment and CNC machining as specified
Aluminum Cold Forging
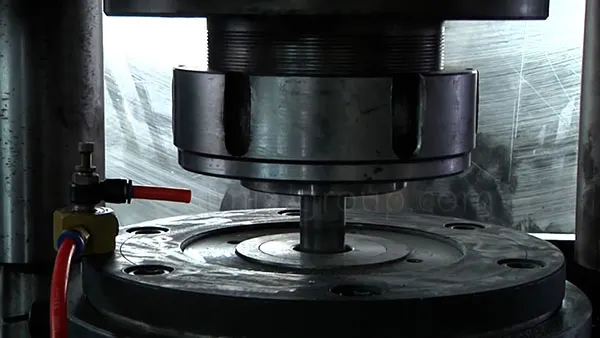
SIMIS supports aluminum cold forging and cold extrusion for suitable small, repeat-production parts, including levers, sleeves, connectors and precision component blanks. We assess alloy formability, billet condition, forming stages, tool life and production volume before recommending this route.
Overlapping part-weight reference: 0.01–2 kg
Maximum part dimensions: diameter up to 100 mm; length up to 200 mm
Cold-extrusion equipment: 300–1,200-ton presses
Applicable operations: cold extrusion, heading and subsequent CNC finishing where required
Forged Aluminum Heat Treatment
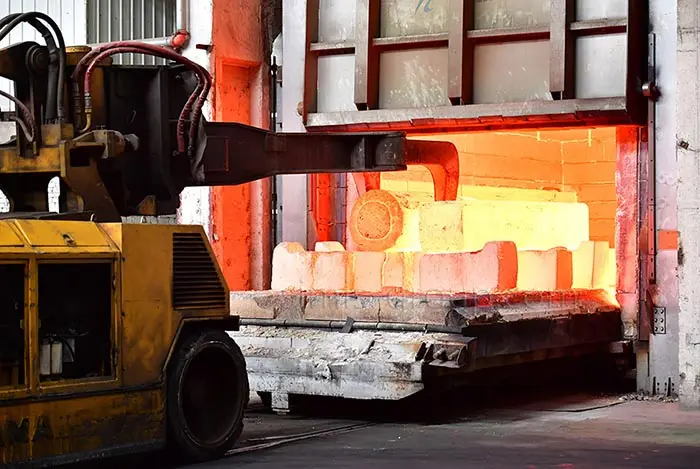
SIMIS supports alloy-specific heat-treatment planning for aluminum forgings where a specified strength and temper are required. For suitable heat-treatable grades, solution treatment, quenching and aging are selected according to the approved drawing and material standard. Dimensional distortion and critical machined features are considered when planning the treatment sequence.
Heat-treatable alloy families: selected 2xxx, 6xxx and 7xxx series
Common specified tempers: T4, T6 or appropriate overaged tempers, subject to alloy and applicable standards
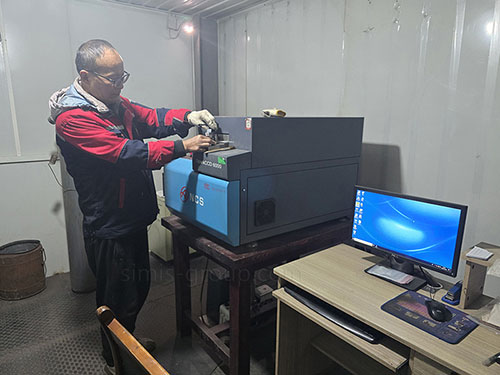
Required verification: specified hardness or mechanical properties, heat-treatment records and dimensional checks as agreed

Aluminum Forging CNC Machining
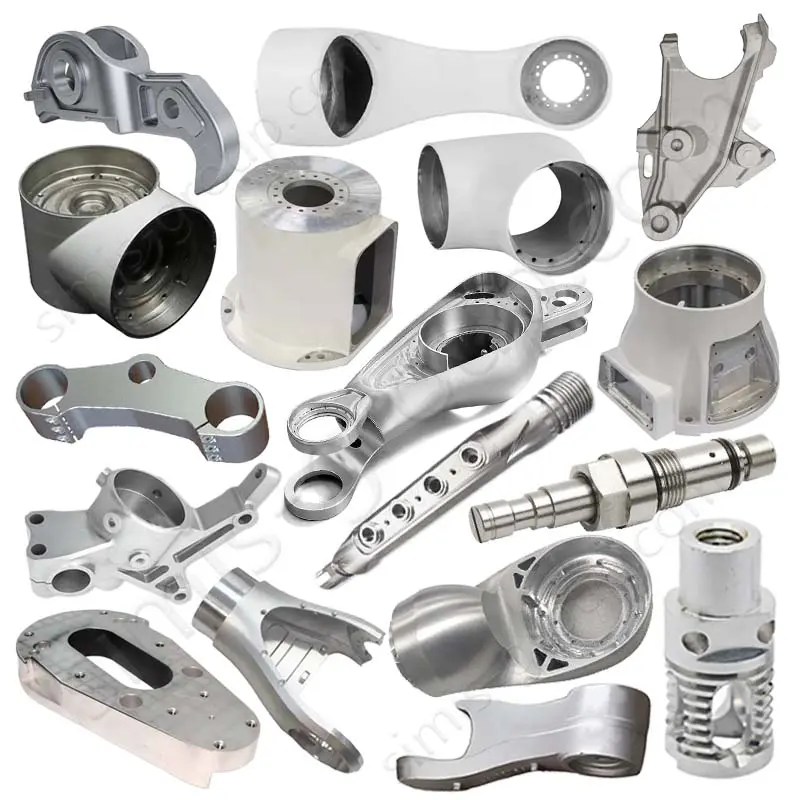
SIMIS offers CNC turning, milling, drilling, boring and finishing for forged aluminum components. Machining establishes bearing seats, threaded holes, sealing surfaces and other critical interfaces after forging and any required heat treatment. Tolerances and inspection methods are agreed against the customer drawing.
Turning reference: Ø10–Ø800 mm; machining length up to 1,500 mm
Vertical machining center travel: X 1,000 × Y 600 × Z 600 mm
Horizontal machining center: four-axis; 630 × 630 mm pallet
Aluminum Forging Surface Treatment
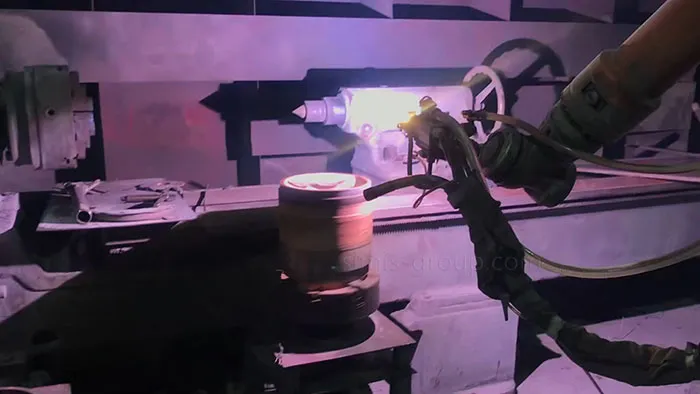
SIMIS coordinates finishing and protective surface treatment for forged aluminum parts through suitable production resources and specialist partners. The selected treatment depends on aluminum grade, required appearance, corrosion exposure, wear condition and dimensional fit. Coating requirements are agreed before processing.
Common finishes: deburring, blasting and polishing
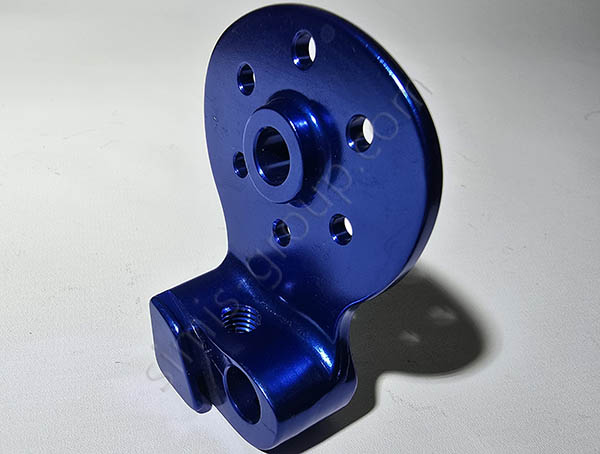
Protective treatments: Type II anodizing, hard anodizing or conversion coating where alloy and specification permit
Optional coatings: powder coating or painting; color, film thickness and tests as specified
Aluminum Alloy Grades for Custom Forging
Non-Heat-Treatable Aluminum Alloys Forging
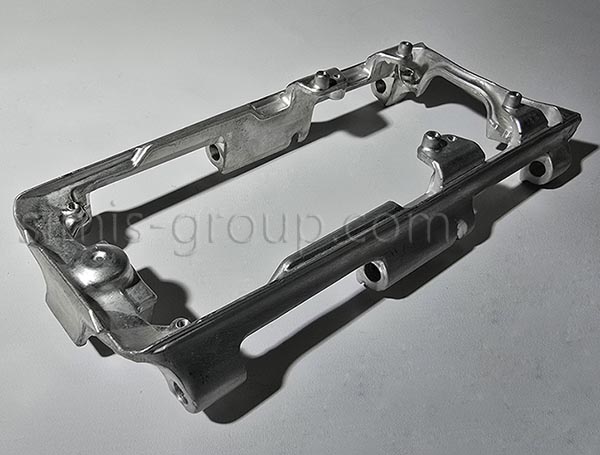
SIMIS evaluates suitable non-heat-treatable aluminum alloys for forged or cold-formed components that prioritize corrosion resistance, ductility or conductivity over precipitation-hardened strength. Selected commercially pure aluminum, 3xxx and 5xxx grades may be considered according to billet availability, geometry and forming feasibility. Not every grade is suited to every forging process.
Aluminum-Copper Alloy Forging
SIMIS evaluates heat-treatable aluminum-copper alloy forgings for specified lightweight structural and mechanical components. Suitable 2xxx-series grades, such as 2024 when available, may be considered for levers, brackets and other load-bearing parts. The approved alloy and temper, corrosion protection, forging method and required mechanical testing are reviewed before production.
Aluminum-Magnesium-Silicon Alloy Forging
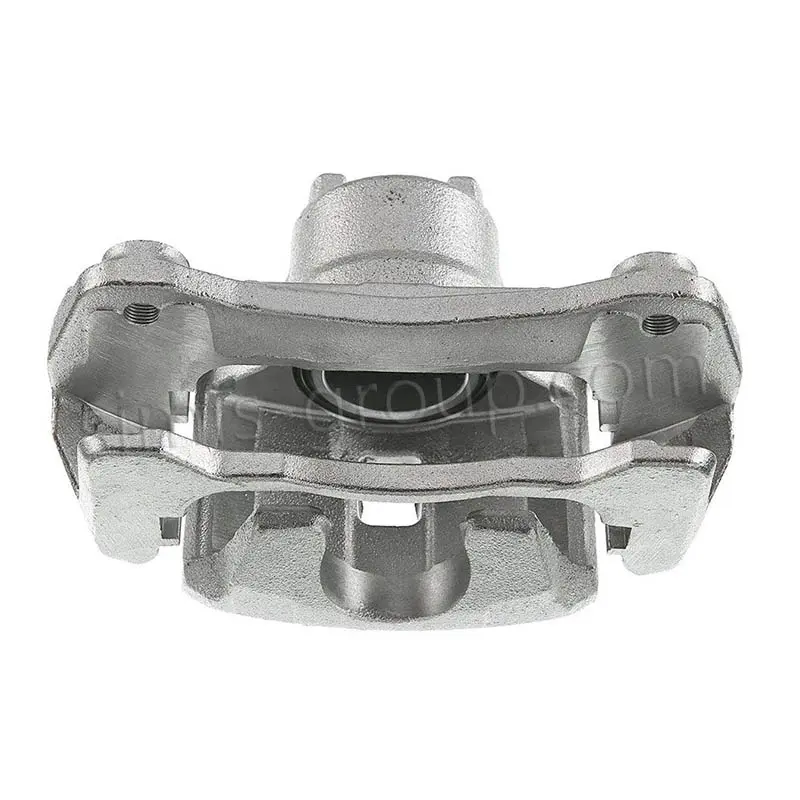
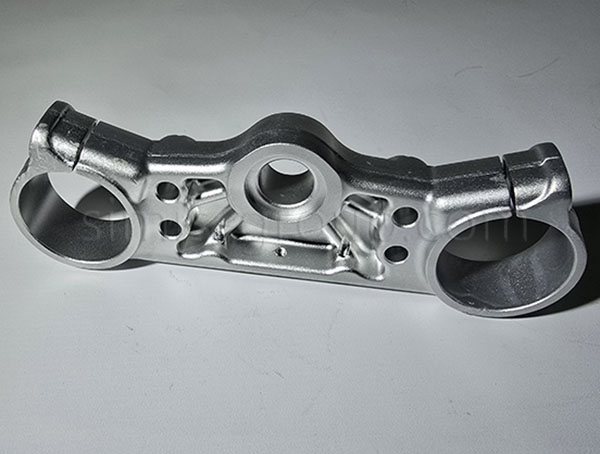
SIMIS supports or evaluates aluminum-magnesium-silicon alloy forgings for bicycle parts, automotive brackets, suspension-related components, machine fittings and other lightweight OEM products. The heat-treatable 6xxx family, including 6061 and 6082 subject to supply and tooling review, can be matched to the required strength, corrosion performance, machining features and final temper.
Aluminum-Zinc Alloy Forging
SIMIS evaluates high-strength aluminum-zinc alloy forgings for selected structural, mechanical and fatigue-sensitive components. Heat-treatable 7xxx-series grades, including 7075 where suitable, require confirmation of the forging route, material temper, section thickness and service environment. Corrosion and stress-corrosion requirements are considered alongside strength and machining specifications.
Industries Served by Our Aluminum Forging Factory
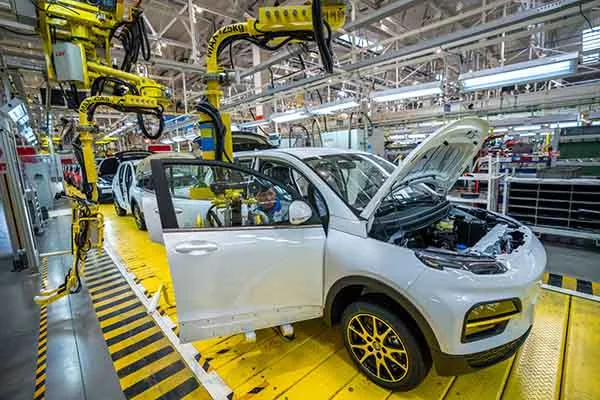
Custom Aluminum Forgings: From Drawings to Production
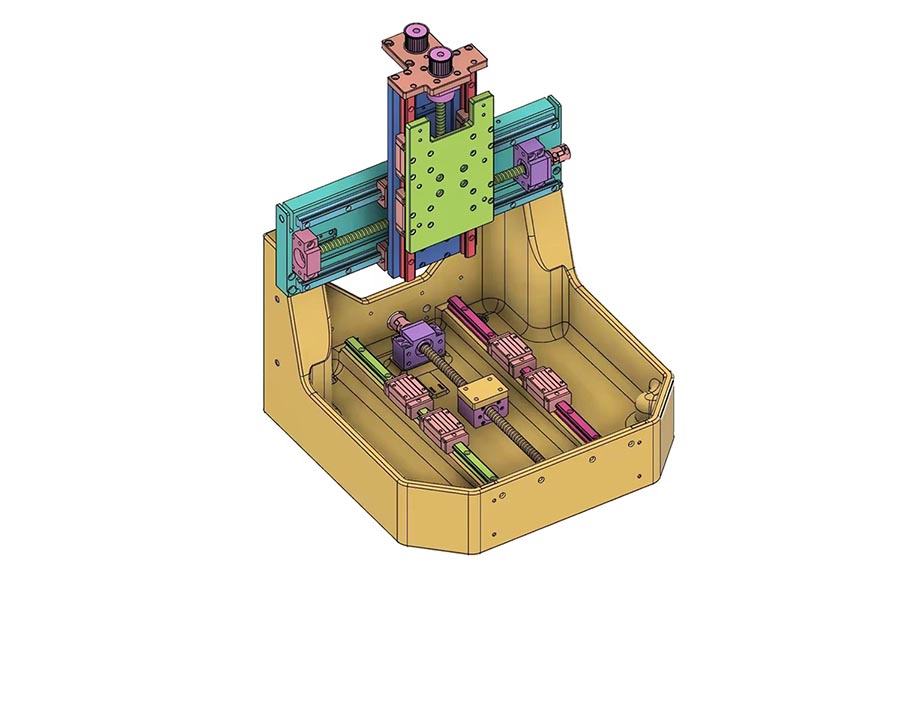
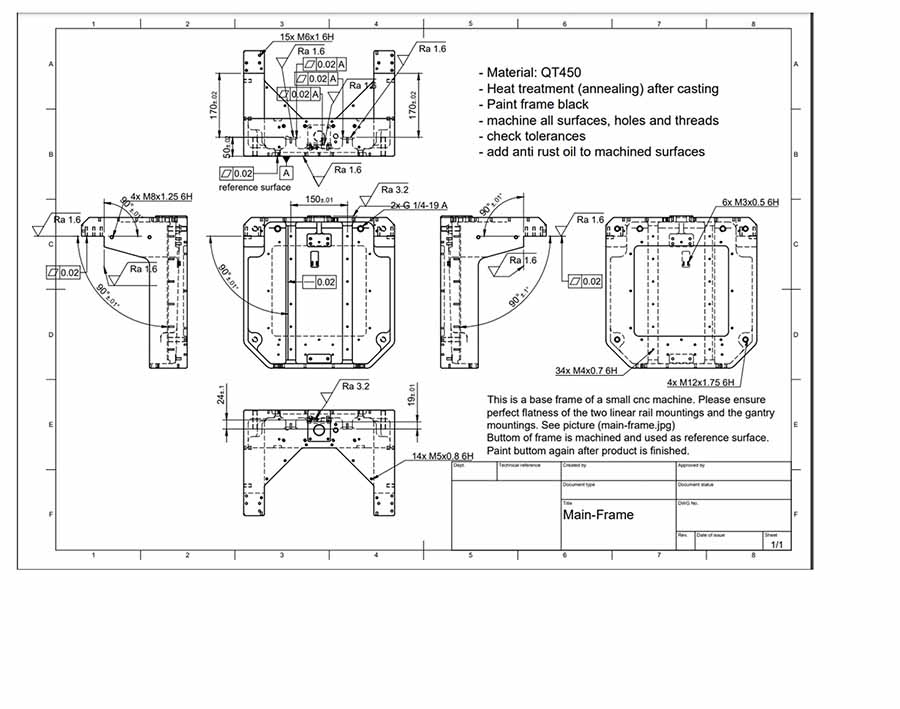
Engineering Review, Tooling & Sample Approval
1. Review Drawings and Application
Send 2D drawings or 3D CAD models with the part function, operating loads, critical interfaces, expected batch quantity and any fatigue or corrosion requirements. SIMIS reviews section transitions, ribs, holes, machining features and potential forging limitations. If only an existing sample is available, reverse-engineering requirements should be discussed separately.
2. Confirm Aluminum Alloy and Temper Requirements
Specify the required aluminum grade, applicable material standard and delivery temper, such as an approved 6xxx or 7xxx condition. Confirm any tensile or yield strength, elongation, hardness, fatigue-related or corrosion-resistance requirements. Material substitutions and alternative tempers are evaluated only with customer approval.
3. Select the Aluminum Forging Process
Assess closed-die forging, ring rolling or cold forging according to alloy formability, part geometry, size, production volume, load direction and tooling economics. The manufacturing route also accounts for expected grain flow, heat treatment and subsequent CNC machining. Production-line capability and any limitations are confirmed before tooling.
4. Plan Billets, Dies and Machining Allowances
Review billet size and condition, heating or lubrication requirements, die parting, draft angles, flash trimming, material flow and machining allowances. For structural aluminum forgings, attention is given to grain-flow direction, thin transitions and possible laps or folds. Heat-treatment distortion, critical datums and surface-finish requirements are included in the plan.
5. Produce and Evaluate Initial Samples
Where tooling and sample approval are included in the agreed order, initial forgings are checked for dimensional fit, surface discontinuities and material condition. Required heat treatment, machined features and specified hardness or mechanical tests are assessed against the approved drawing. Any necessary tooling or process changes are agreed before production release.
6. Approve Inspection and Acceptance Criteria
Define critical dimensions, approved alloy and temper, mechanical requirements, visible surface acceptance and any corrosion or finish specifications. The agreed quality plan may include dimensional inspection, material identification, tensile or hardness testing and specified non-destructive examination where applicable. Sampling, traceability and reports are determined by the approved order requirements.
Controlled Production, Inspection & Delivery
1. Confirm Production Readiness
After any required sample or first-article approval, confirm the released drawing revision, aluminum alloy and temper, billet supply, forging dies, heat-treatment plan, machining operations and production quantity. Inspection points and the agreed records are reviewed before batch production begins.
2. Monitor Forging, Heat Treatment and CNC Machining
Apply agreed controls to billet preparation, forging temperature or cold-forming conditions, die operation, trimming and heat treatment as applicable. For aluminum parts, relevant checks may include laps or cracks, dimensional change after aging, hardness and critical machined interfaces. Process control is tailored to the selected alloy and forging method.
3. Perform Final Inspection and Documentation
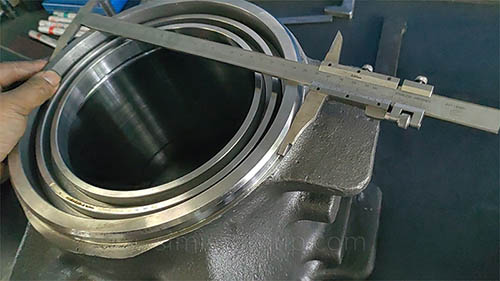
Inspect finished aluminum forgings against the released drawings and acceptance criteria. Depending on the order, documentation may include dimensional inspection, alloy certification, heat-treatment or temper records, hardness or tensile results, surface-coating checks and specified non-destructive testing. The inspection scope is agreed for each customer project.
4. Package and Dispatch Approved Forgings
Protect machined surfaces, threaded features and cosmetic or anodized finishes during handling, packing and transport. Agree on identification, corrosion or abrasion protection, packing method, shipment terms and required supporting documents before dispatch.
Need custom metal castings or forgings made to your drawings? Send SIMIS your 2D/3D files, material specifications, critical tolerances and estimated quantities. We can review manufacturing feasibility and discuss a suitable production approach for your project.


