Custom Truck & Automotive Castings and Forgings
OEM Metal Parts for Trucks & Automotive Equipment
SIMIS manufactures custom metal castings, forgings, CNC-machined parts and selected fabricated components for truck, automotive and related vehicle equipment OEMs. Drawing-based inquiries include engine and gearbox housings, brake discs and drums, steering knuckles, suspension arms, shafts, coupler yokes, towing fittings and mechanical parts for forklifts, motorcycles and bicycles. We assess the specified alloy, component geometry, loading, mating interfaces, annual quantity, machining scope, finish and inspection requirements before recommending a production route. Vehicle safety-related components must be evaluated against the OEM's approved drawings, validation plans and applicable qualification requirements; manufacturing an individual metal part does not establish vehicle-level compliance. Send 2D drawings or 3D CAD models with critical dimensions and the intended production quantity for a project-specific quotation.
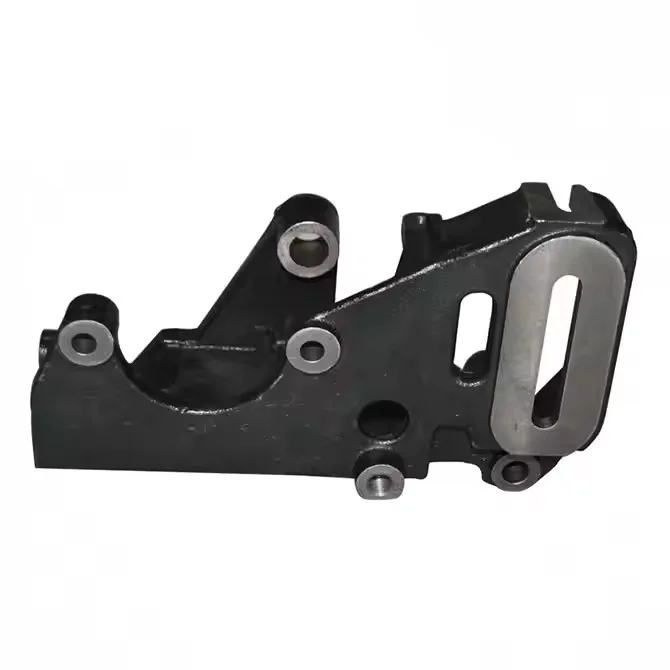
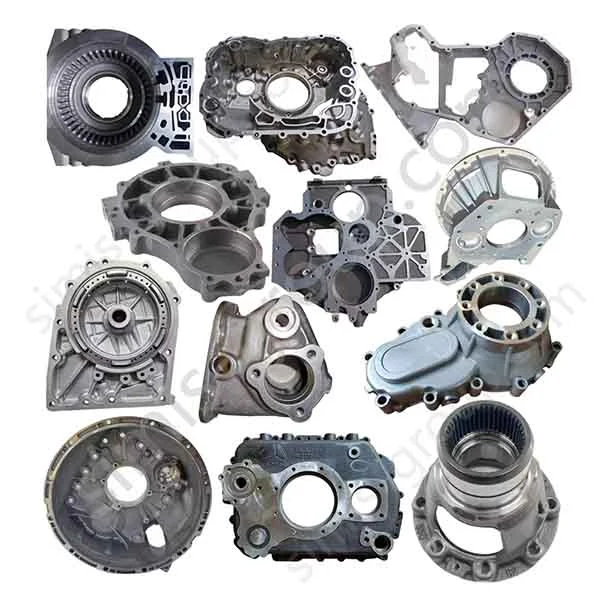
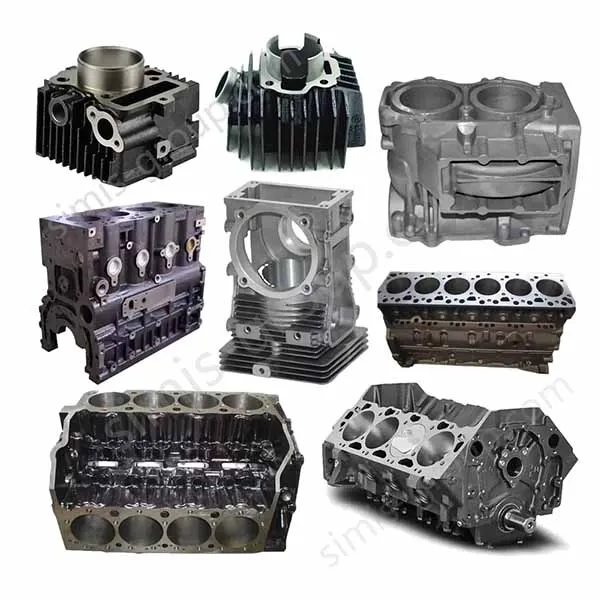
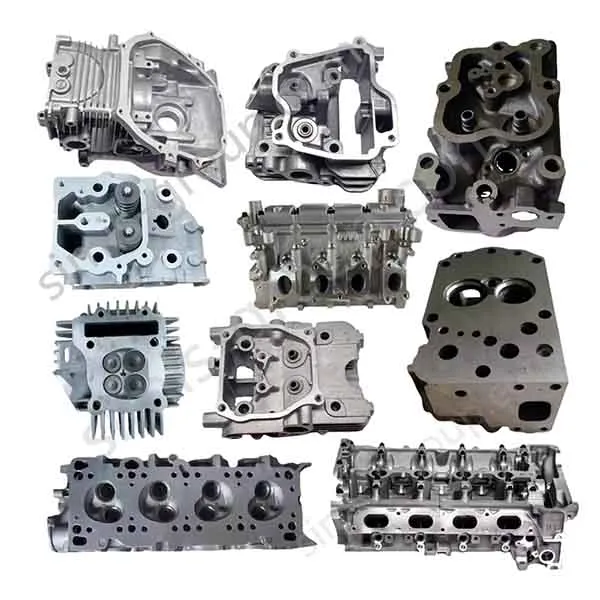


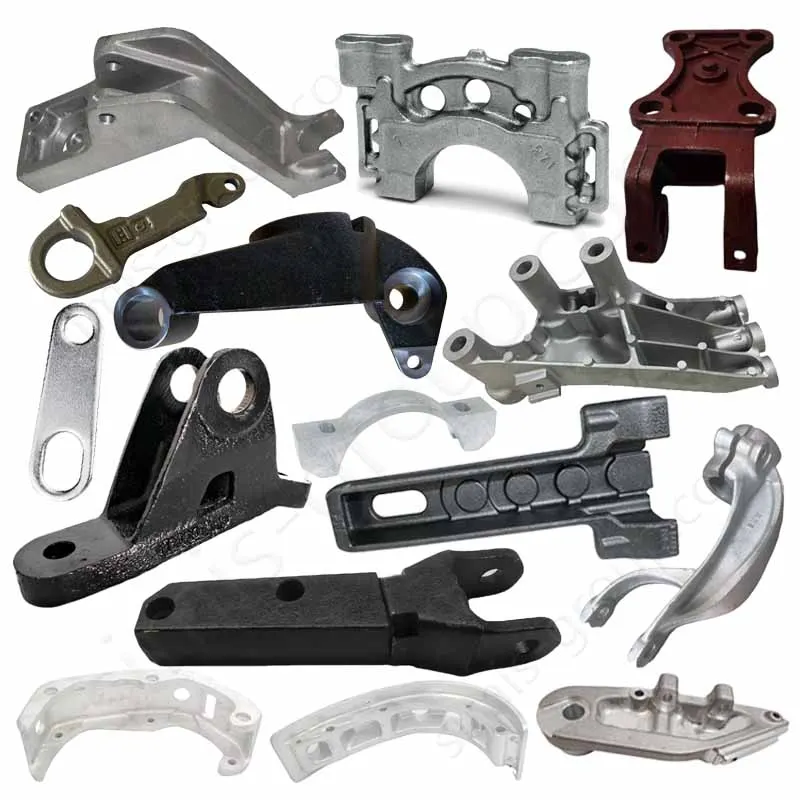
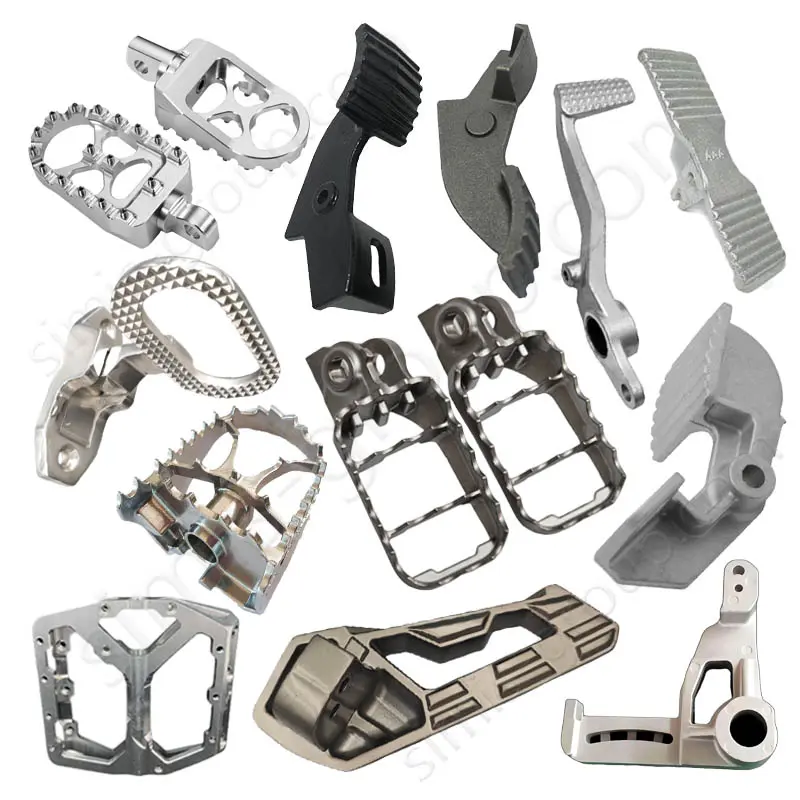
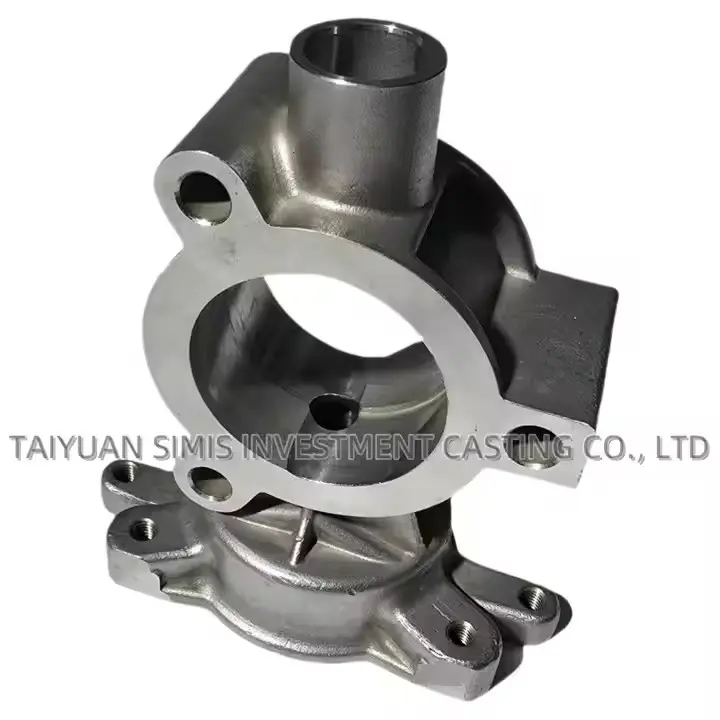
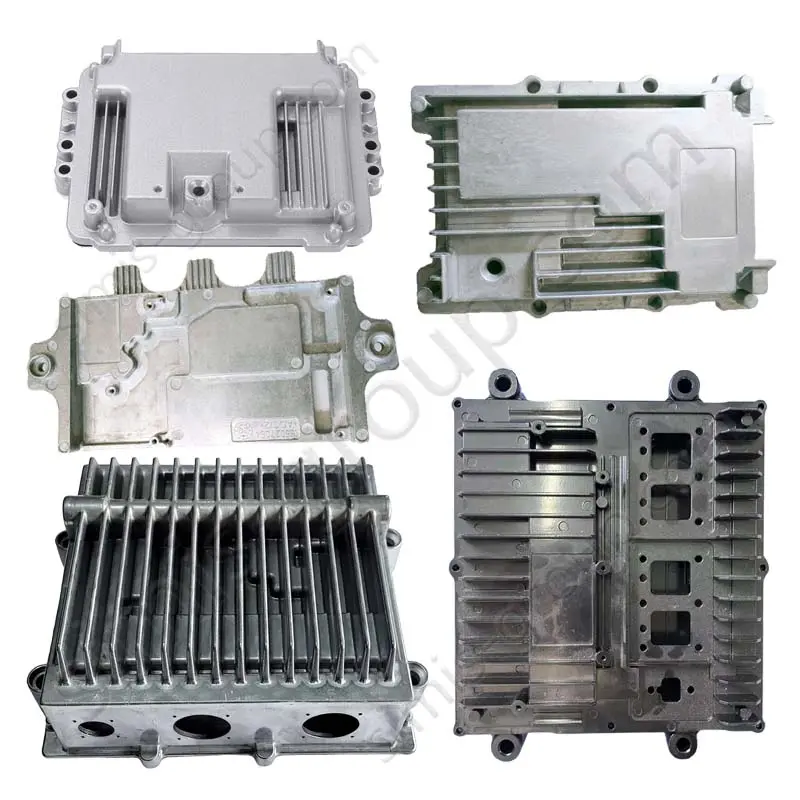
Custom Truck & Automotive Components & Applications
1. Engine Blocks, Cylinder Heads & Rotating Components
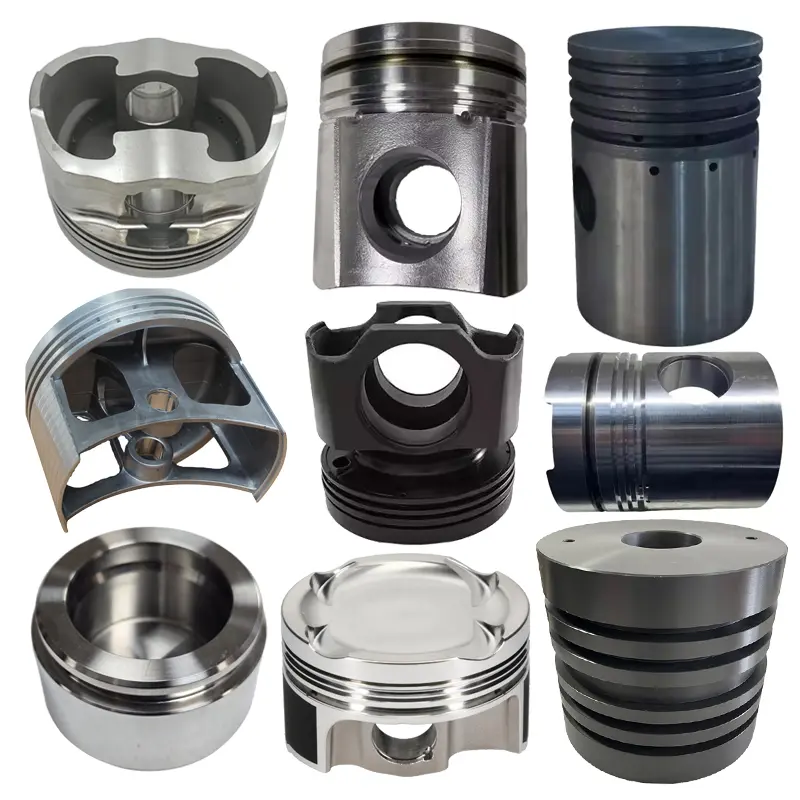
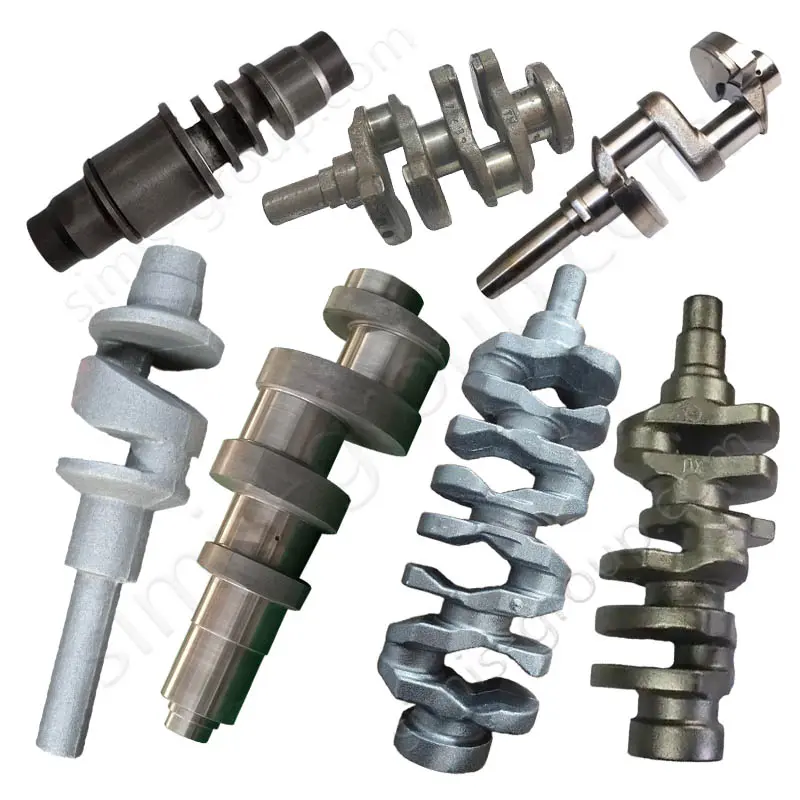
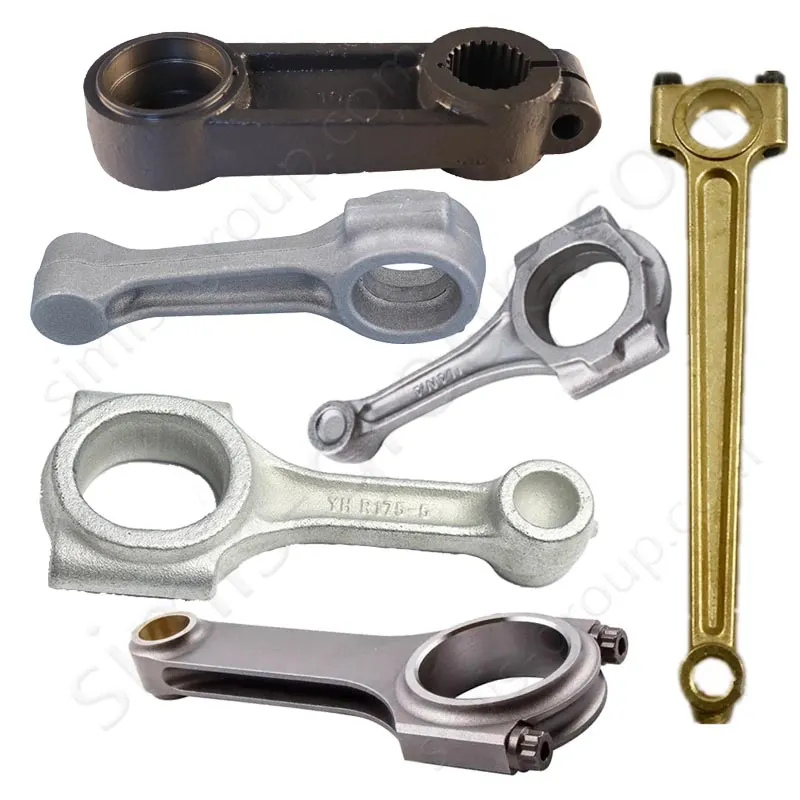
Engine OEMs may require custom cylinder blocks, cylinder heads, flywheel housings, crankshafts and connecting rods. Iron or aluminum casting may be assessed for complex blocks and housings with cores, coolant jackets or oil passages. Steel forging and subsequent machining are potential routes for selected crankshafts and rods, while pistons require a design-specific cast or forged aluminum route rather than being treated as universally forged.
Drawing review focuses on main-bearing alignment, cylinder-bore locations, deck flatness, sealing faces, dynamic loading, material condition and internal passage cleanliness. Engine operating performance and fatigue acceptance require the OEM-defined inspection and validation program.
2. Suspension Arms, Mounts & Axle Components
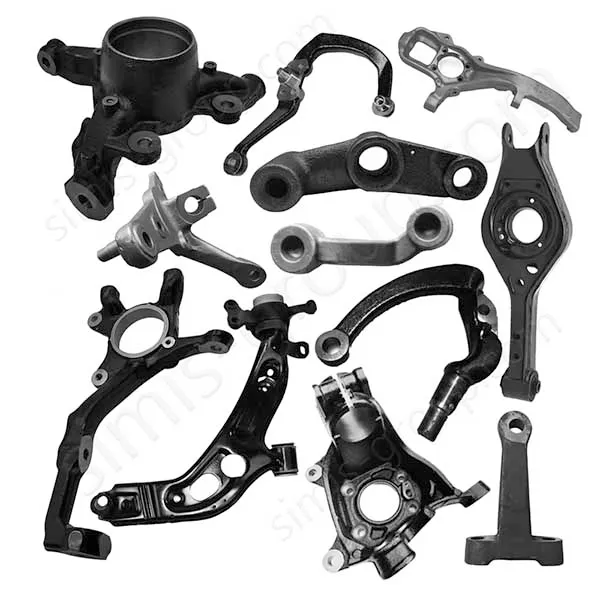
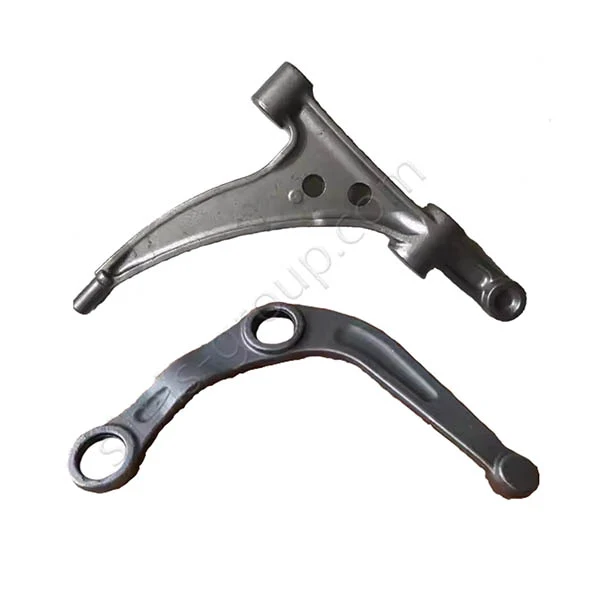
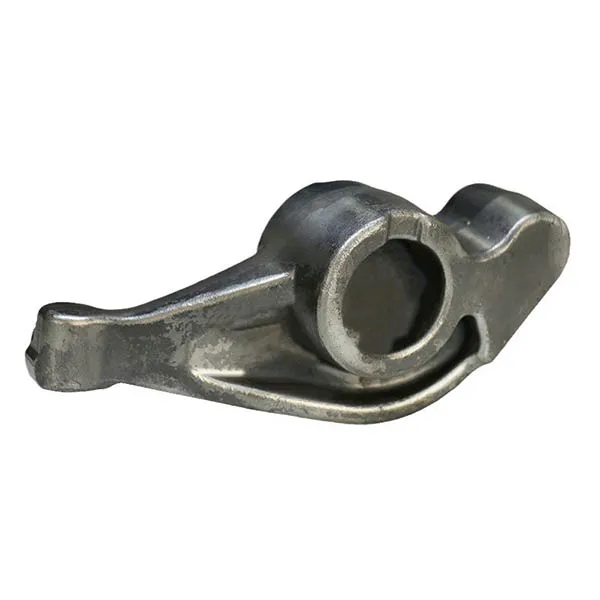
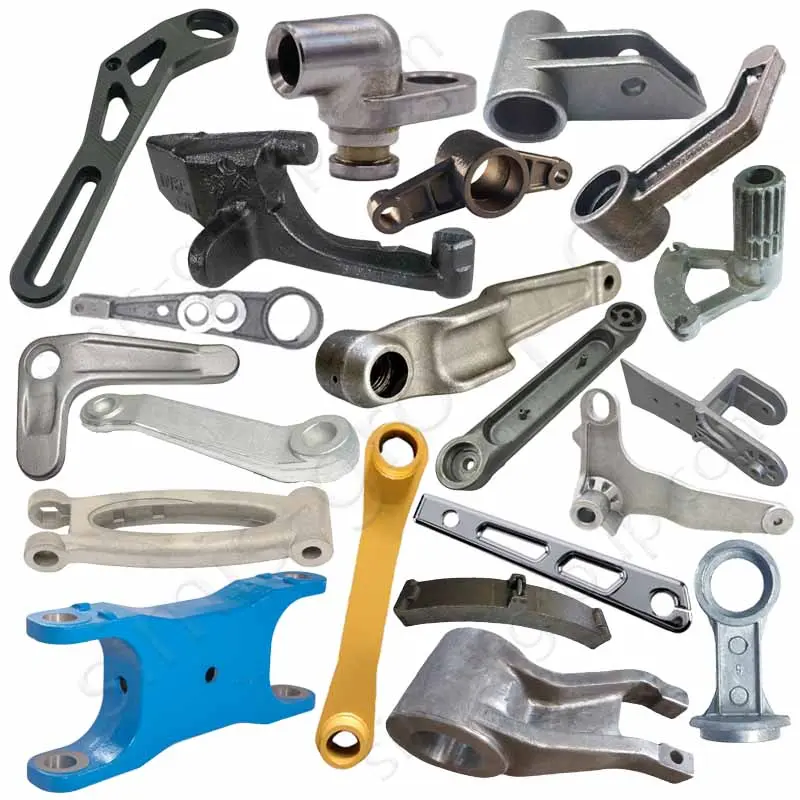
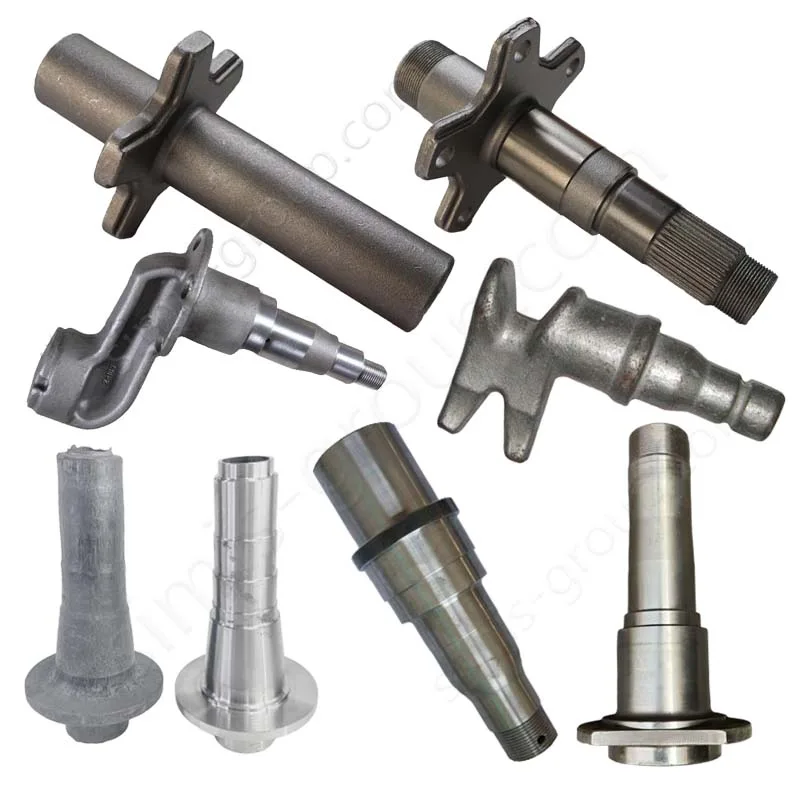
Commercial vehicles, passenger cars and selected forklift equipment use control arms, shock mounting brackets, air spring bases and axle spindles. Ductile iron or aluminum castings can suit certain formed housings or supports; steel or aluminum forgings may be considered for specified load-bearing arms, spindles and linkages. The correct method depends on geometry, load case and customer material specification.
Important characteristics include bushing-eye alignment, ball-joint mounting features, bearing or pin fits, bracket hole locations, strength and fatigue requirements. A manufacturing quotation should distinguish the metal part from complete suspension assemblies and should not imply that vehicle roadworthiness testing is included.
3.Brake Discs, Drums, Calipers & Brackets
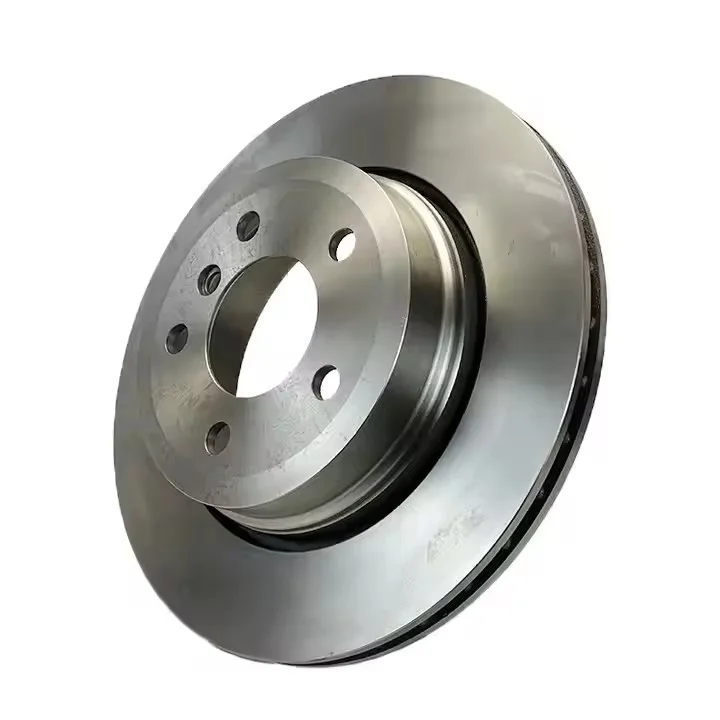
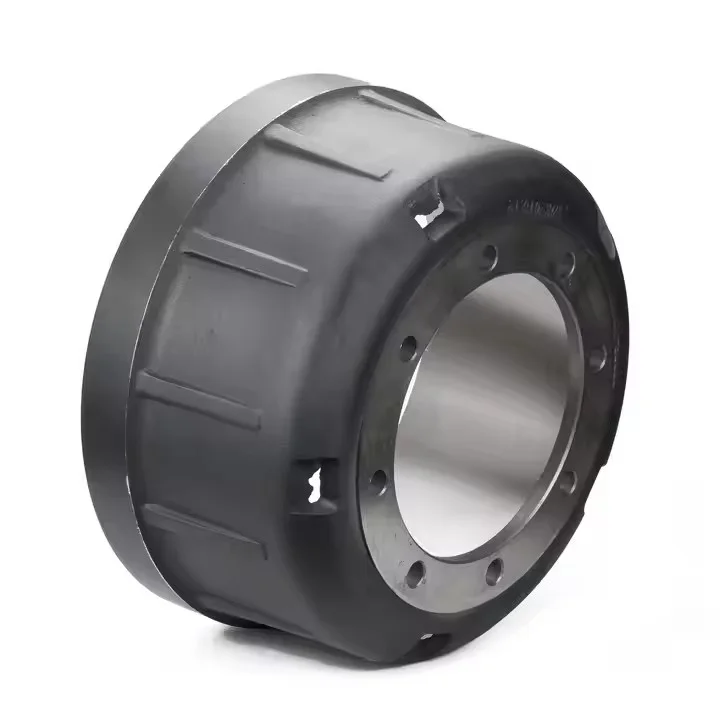
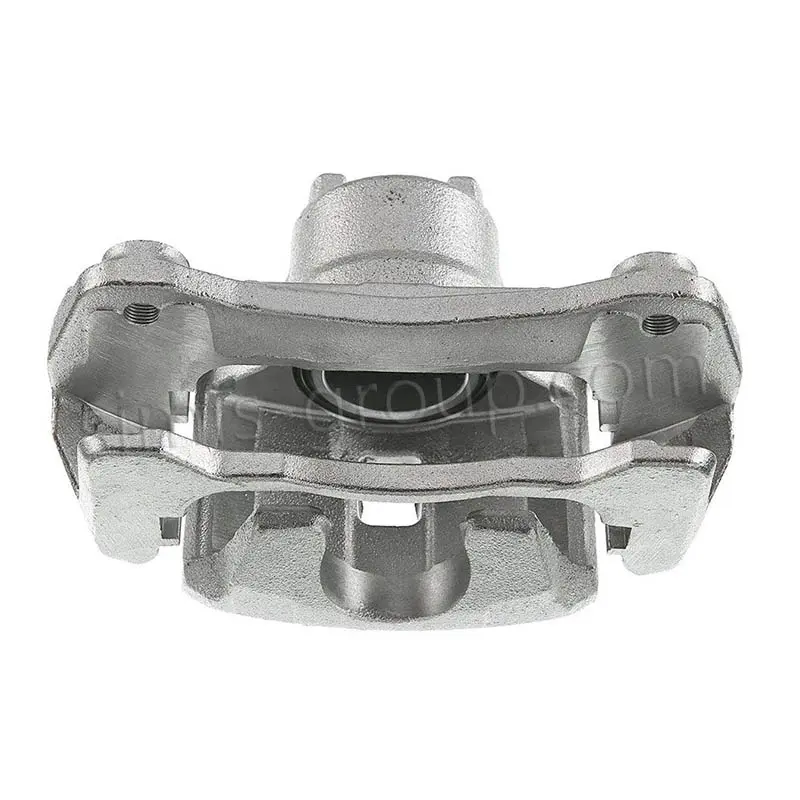
Brake-system components may include brake discs, brake drums, caliper bodies and mounting brackets. Gray iron casting is a common route for many discs and drums; ductile iron or aluminum casting can be evaluated for selected caliper designs, while steel forgings or machined blanks may suit particular bracket and pin components. Brake discs and drums should not be listed as standard forged products without a specific design basis.
The drawing should define friction-surface dimensions, rotor or drum runout, thickness variation, bore fit, caliper piston bores, fluid passage integrity and applicable material and thermal requirements. Any balancing, pressure testing, friction testing or brake-system approval must be explicitly scoped and verified against the purchaser's acceptance plan.
4. Chassis Mounting, Towing & Frame Hardware
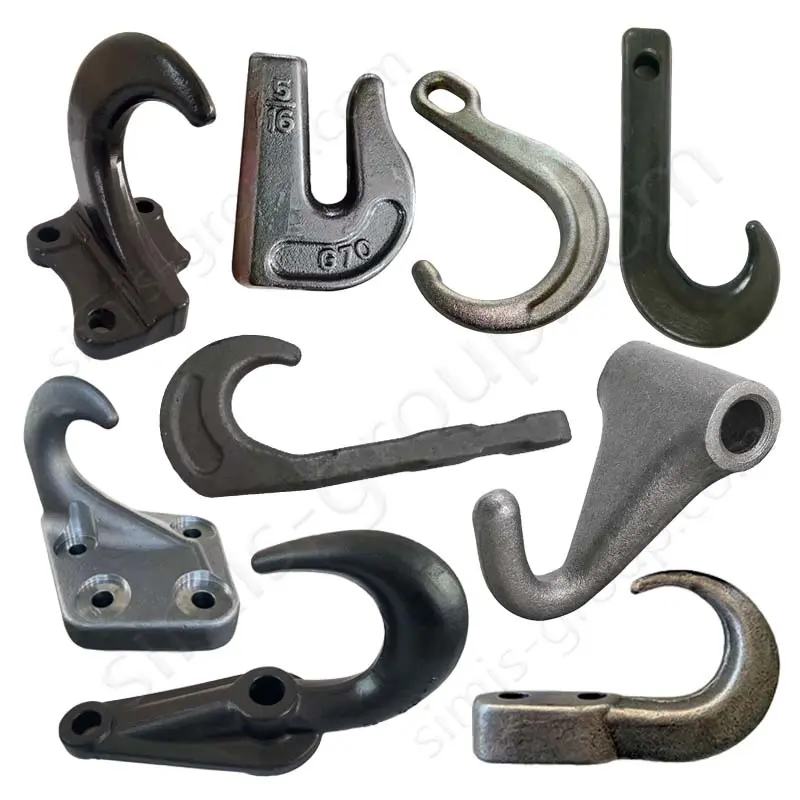
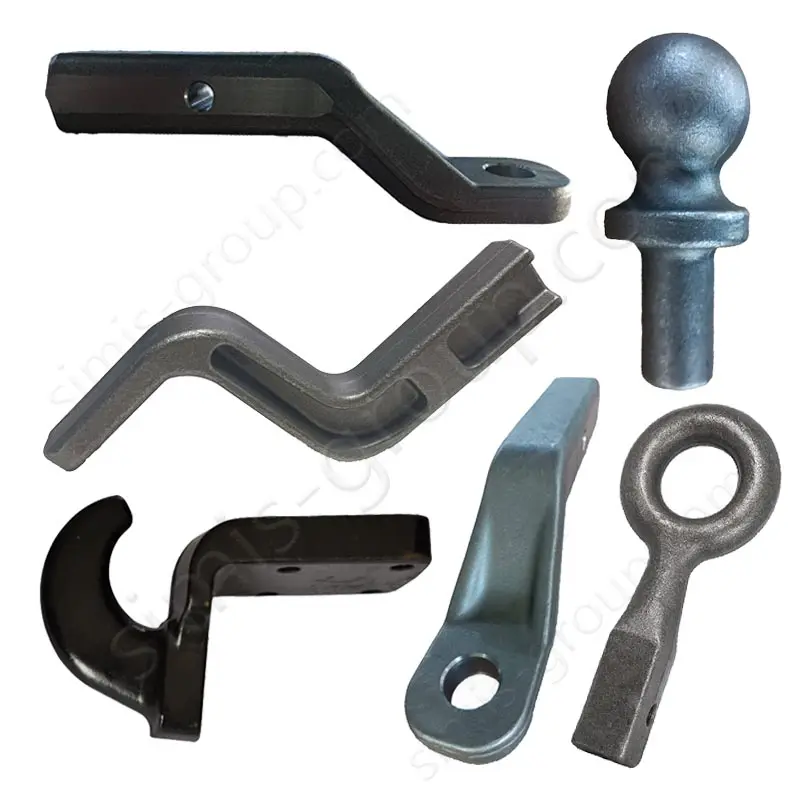
Heavy-duty trucks and utility vehicles need attachment hardware such as tow hooks, trailer hitch ball mounts, support brackets and load-transfer fittings. Steel closed-die forging may suit selected towing and attachment components with complex local loading; cast steel, ductile iron, machined plate or fabricated steel may suit other brackets and housings where the approved design permits.
Longitudinal frame rails and large crossmembers are more typically fabricated or formed from structural stock, not routinely forged as finished assemblies. Manufacturing review covers towing load paths, attachment-hole geometry, weld details where specified, corrosion protection, material traceability and project-specific mechanical or proof-load tests.
5. Gearbox, Clutch & Driveline Components
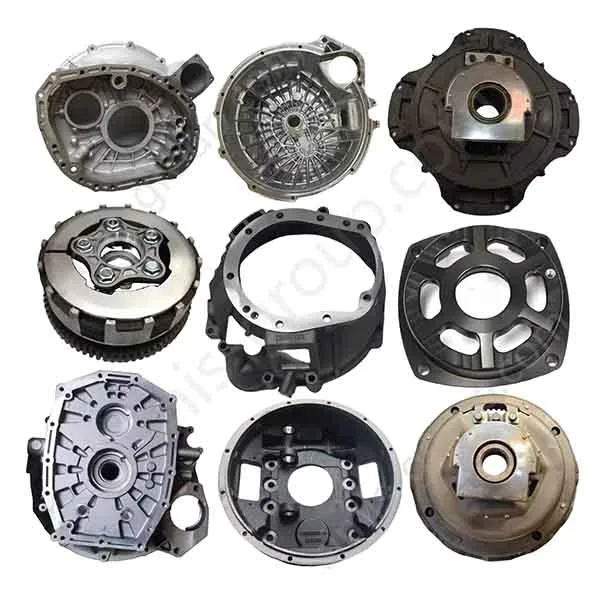
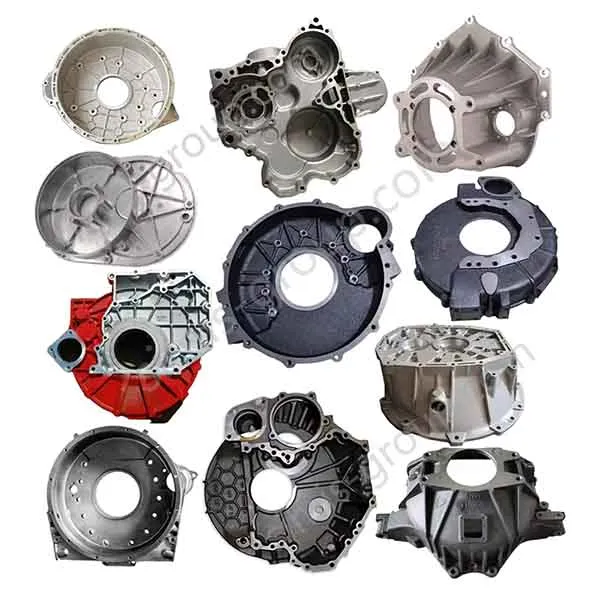
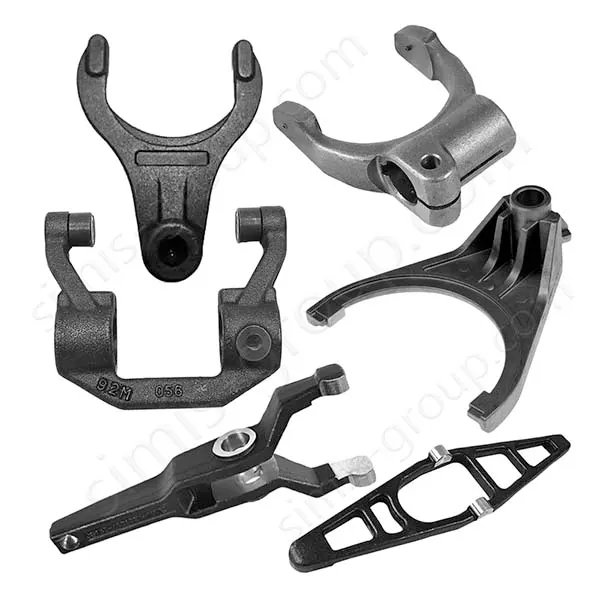
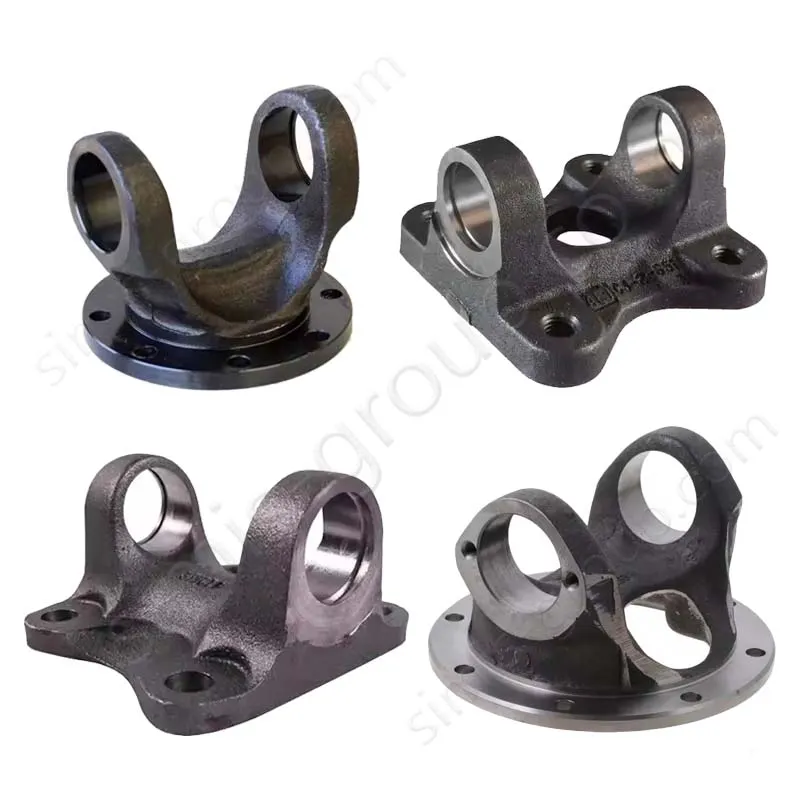
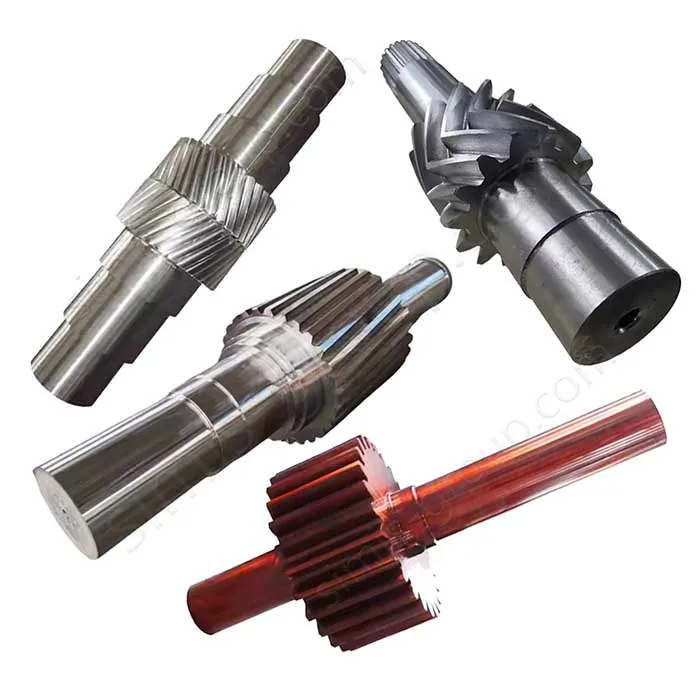
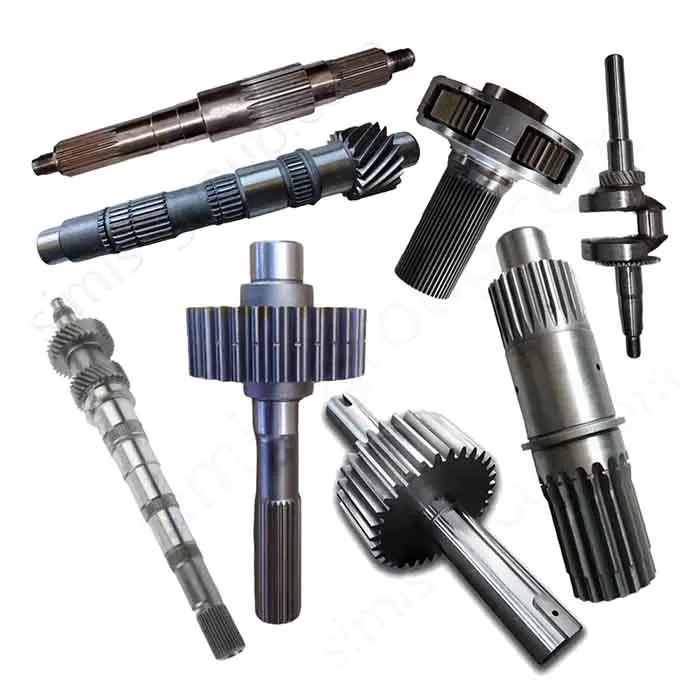
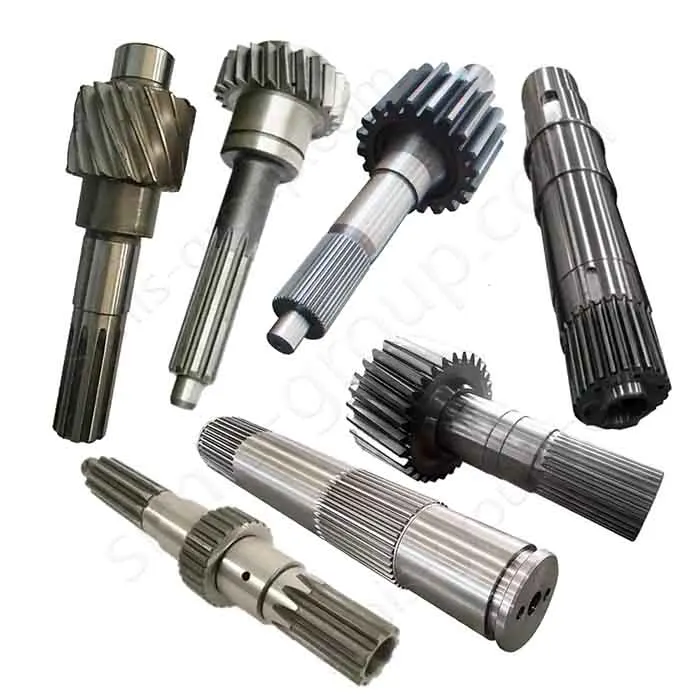
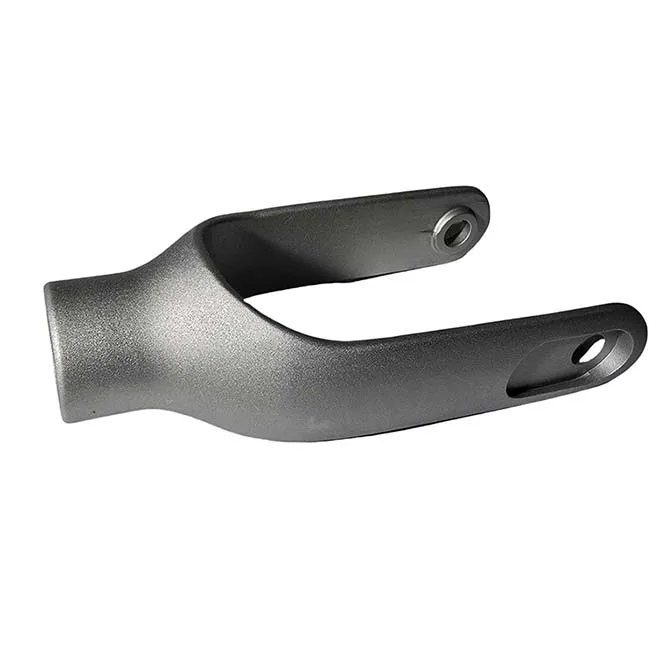
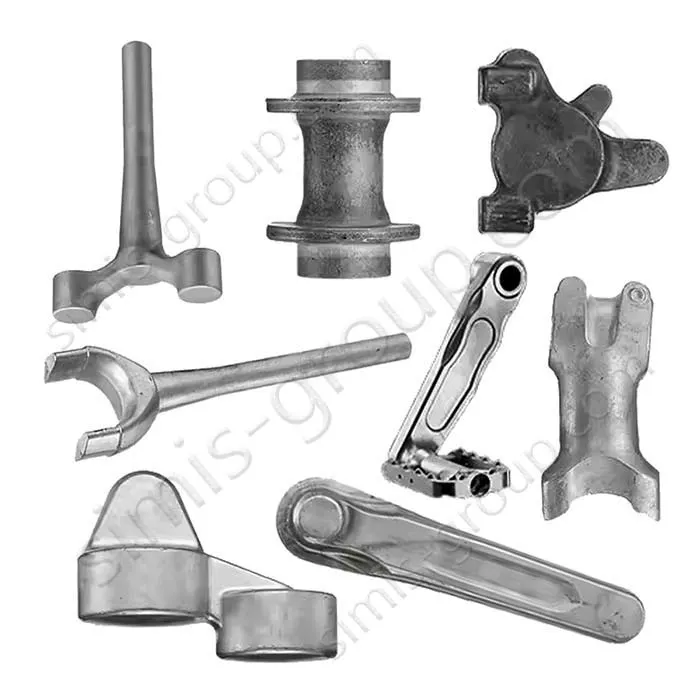
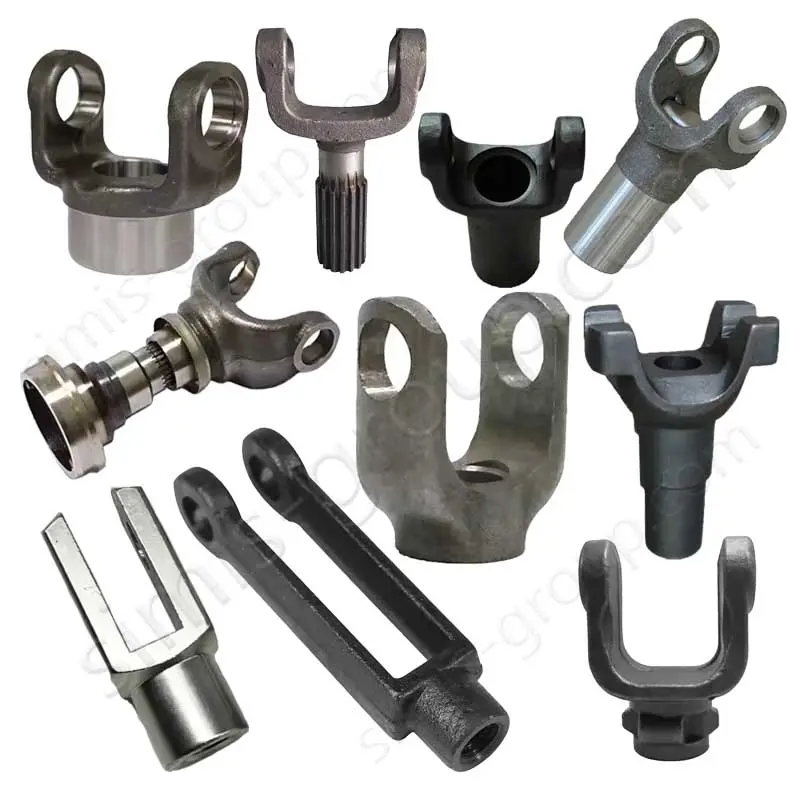
Powertrain projects may call for gearbox housings, clutch housings, clutch shift forks, splined transmission shafts, flange yokes and universal joint forks. Cast iron or aluminum casting can form intricate enclosure geometry, while alloy-steel forging followed by turning, milling or spline finishing can suit torque-transmitting parts.
Key drawing features include bearing-bore position, gear-centre spacing, bolt patterns, gasket faces, spline class, concentricity, runout and heat-treated hardness where specified. Shaft and gear design calculations, lubrication design and endurance testing remain dependent on the OEM drivetrain specification.
6. Exhaust, Turbocharger & Air-Management Parts
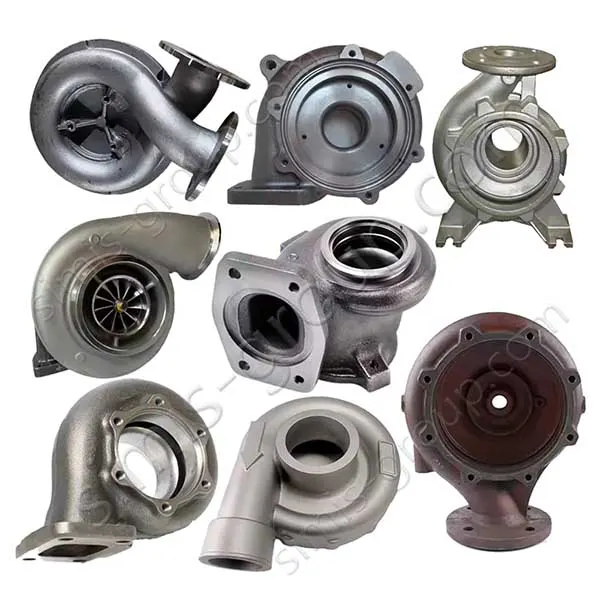
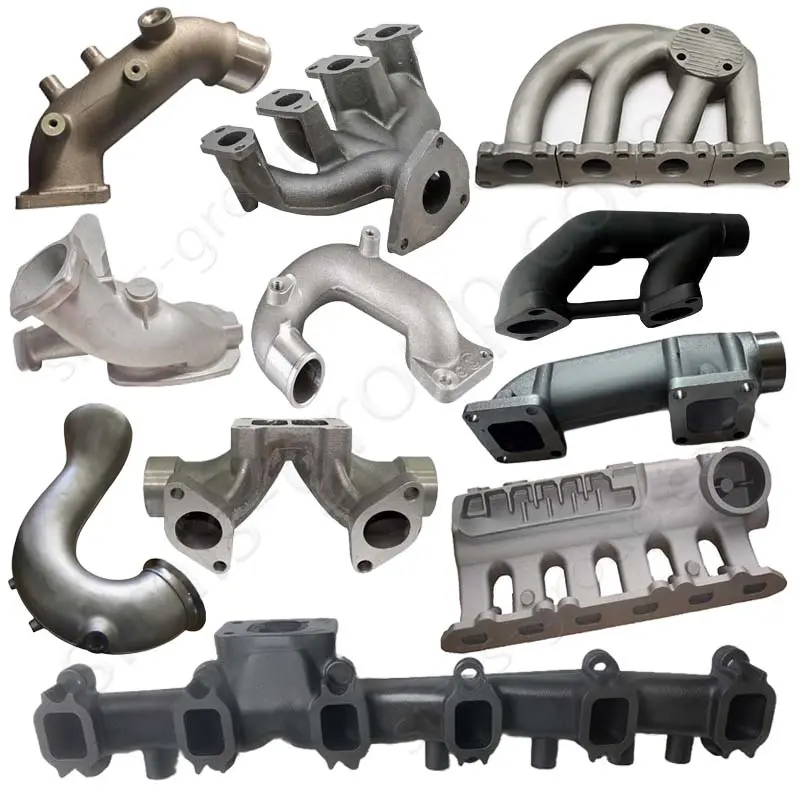
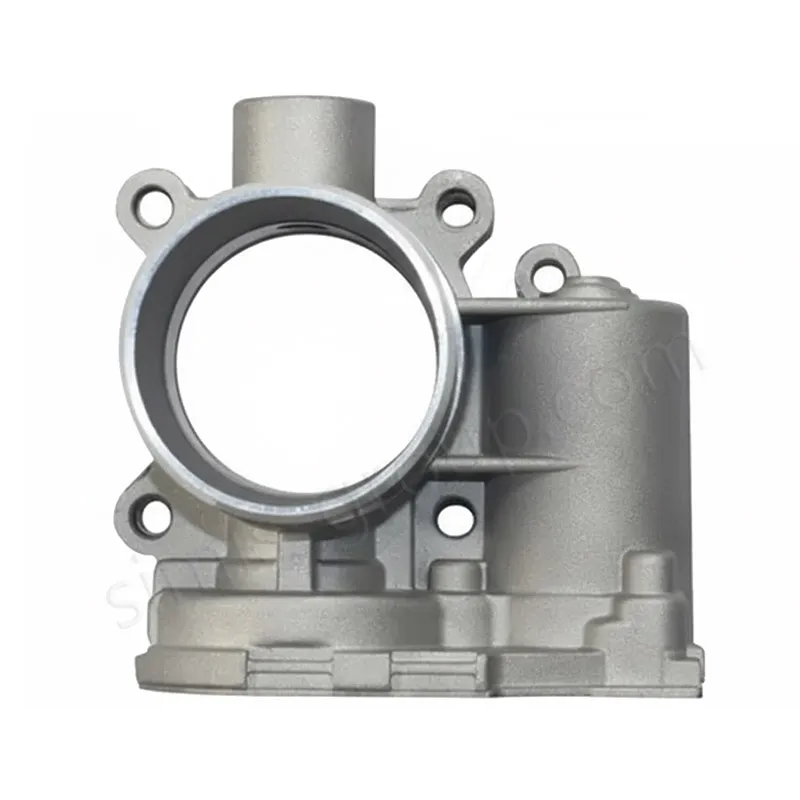
Engine air and exhaust applications can include intake and exhaust manifolds, turbocharger turbine housings, EGR valve housings and throttle housings. Cast iron and selected heat-resistant alloys may be evaluated for hot-gas castings, while aluminum casting is often suitable for customer-defined intake or throttle-body housings. Exhaust tubing, mufflers and headers are commonly fabricated or formed, rather than treated as routine forgings.
Projects should specify exhaust-gas temperature and exposure, flange flatness, passage geometry, wall sections, machining stock, joint interfaces and any leakage requirements. Emissions compliance, turbocharger performance and complete-system thermal endurance need separate OEM validation.
7. Steering Knuckles, Tie Rod Arms & Control Parts
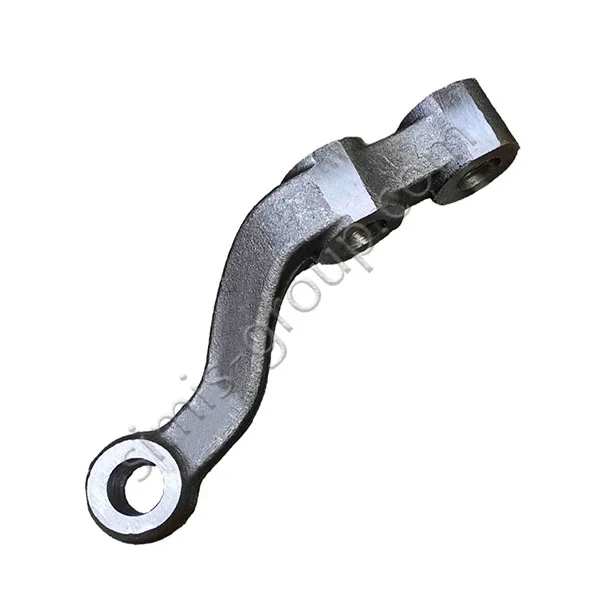
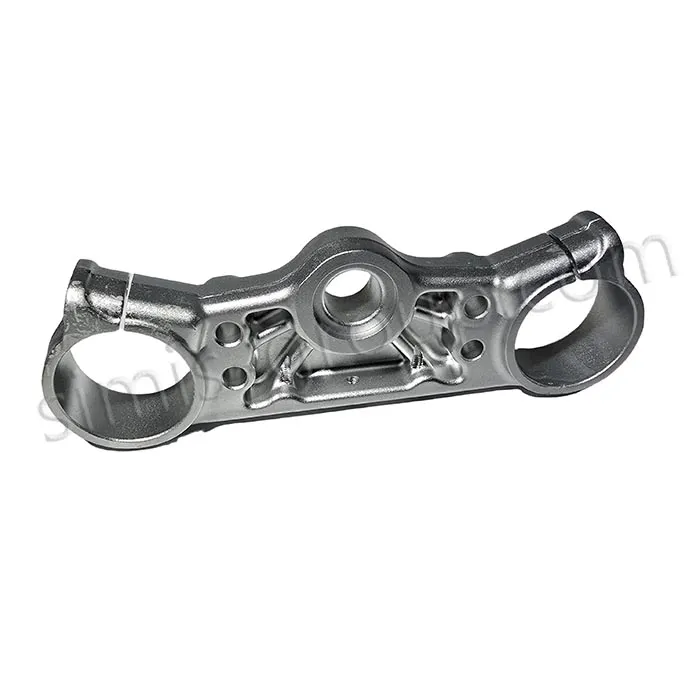
Steering assemblies use metal parts such as steering knuckles and arms, tie rod arms, steering supports and linkage connectors. Steel forging can be appropriate for certain heavily loaded steering and linkage parts; ductile iron or aluminum castings may be acceptable for other approved designs. CNC machining establishes ball-joint seats, taper bores, fastener locations and steering-axis interfaces.
Engineering checks should establish mounting datums, joint taper geometry, hardness, surface condition, fatigue-critical transitions and required material documentation. For related motorcycles and bicycles, stems, forks and bicycle linkage components can be reviewed under their own drawings and test requirements; automotive steering approval is not implied by a generic casting or forging certificate.
Materials for Truck & Automotive Metal Parts
Gray Iron, Ductile Iron & Alloy Cast Iron
Gray cast iron is a common material for selected brake rotors, brake drums, engine blocks and rigid housings where castability, vibration damping and machinability are valued. Ductile iron may be considered for axle-related supports, brackets and other components requiring specified strength and ductility. Iron casting routes depend on wall thickness, cores and part size.
Confirm the exact iron grade, microstructure or mechanical-property requirements, thermal duty, machinable stock and critical dimensions. Alloy cast irons may suit specific elevated-temperature parts, but material selection must follow the vehicle program rather than assuming all grades are interchangeable.
Carbon, Alloy, Cast & Stainless Steels
Carbon and alloy steels are candidates for crankshafts, shafts, steering arms, yokes and towing fittings when the specified strength, toughness and heat treatment justify steel forging. Steel casting, machined bar or fabricated plate may be more appropriate for selected mounts and housings. Stainless steels may be used for particular exhaust fittings and corrosion-exposed hardware.
Purchase specifications should identify steel grade, delivery condition, hardenability, machinability, weldability if relevant, and acceptance criteria for mechanical properties and dimensional inspection. A steel component is not automatically fatigue-qualified or approved for a safety-critical vehicle application.
Cast, Forged & Machined Aluminum Alloys
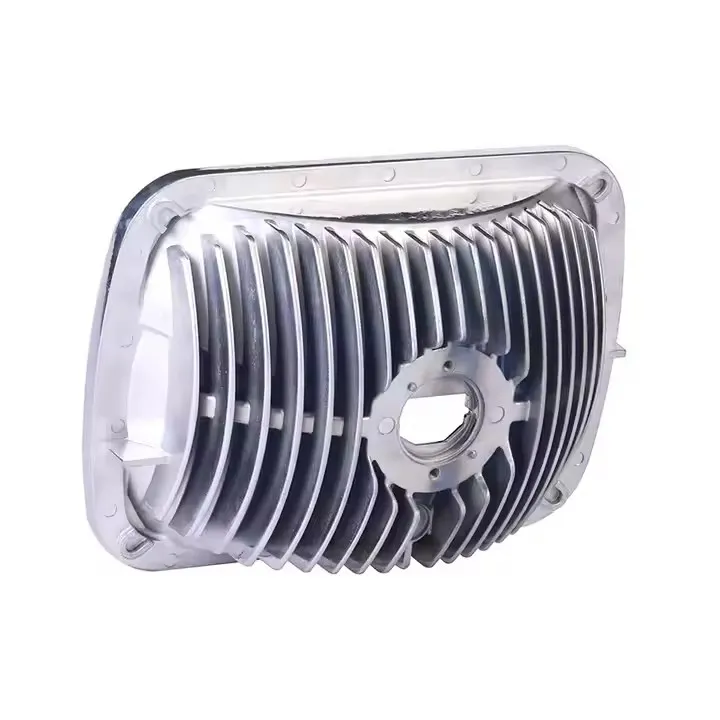
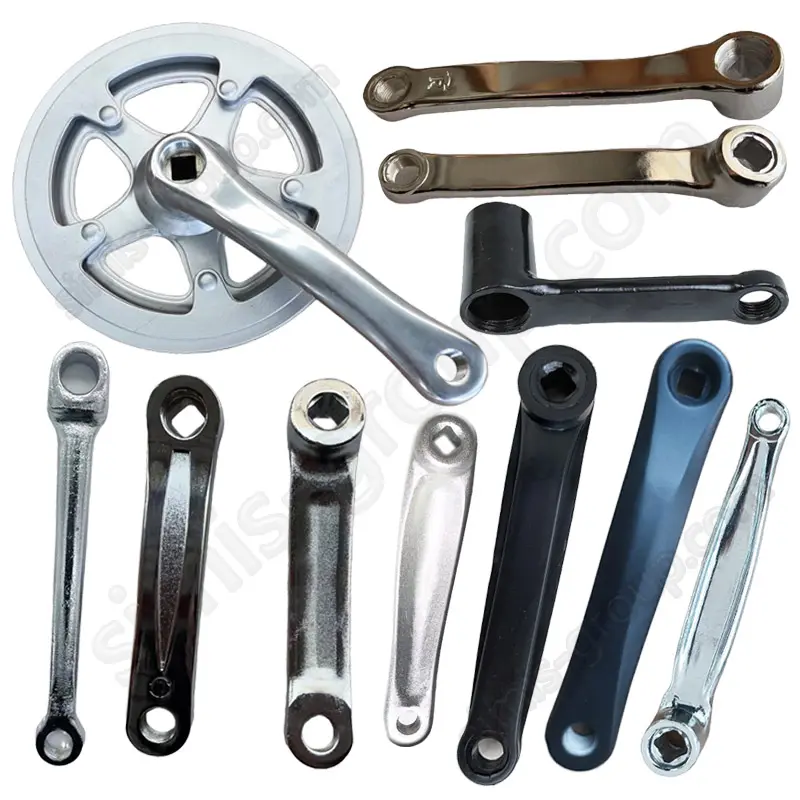
Aluminum alloy castings can be considered for transmission cases, clutch covers, throttle bodies, electronic-control housings and other weight-sensitive vehicle components. Aluminum casting may use pressure die casting or another route suited to part geometry and volume. Aluminum forging may suit selected suspension parts, motorcycle fittings or bicycle crank arms, subject to OEM requirements.
Define the actual alloy and temper, porosity acceptance, dimensional stability, bearing and threaded interfaces, thermal expansion, surface finish and any heat treatment. High structural performance cannot be inferred from the term “aluminum” without the grade, manufacturing condition and validated design.
Copper Alloys & Customer-Specified Metals
Bronze and brass may be suitable for selected vehicle bushings, bearing interfaces, hydraulic fittings, connectors and mechanical wear parts. Copper-alloy casting and machining can be evaluated where part shape and specified composition make them appropriate; wrought copper forms may instead be preferable for current-carrying terminals or busbars.
The order should identify conductivity or wear requirements, mating material, operating temperature, surface condition and any coating. Magnesium, titanium and other special-purpose vehicle materials require separate manufacturability and supplier-scope confirmation and are not presented here as standard SIMIS production options.
Engineering Review, Manufacturing & Quality Control
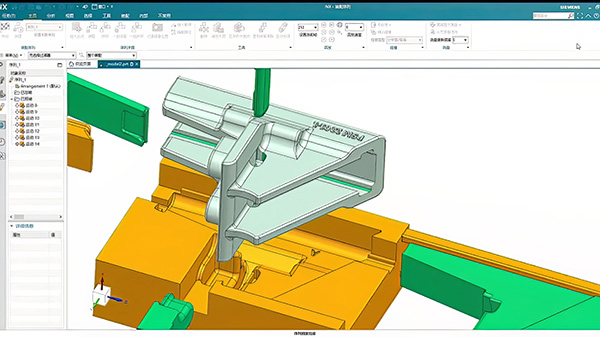
3D Drawings
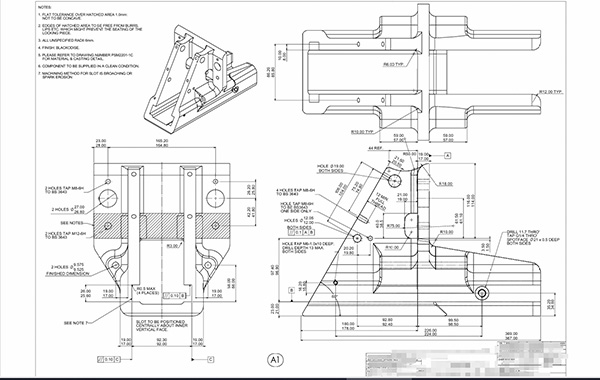
Processing Drawings
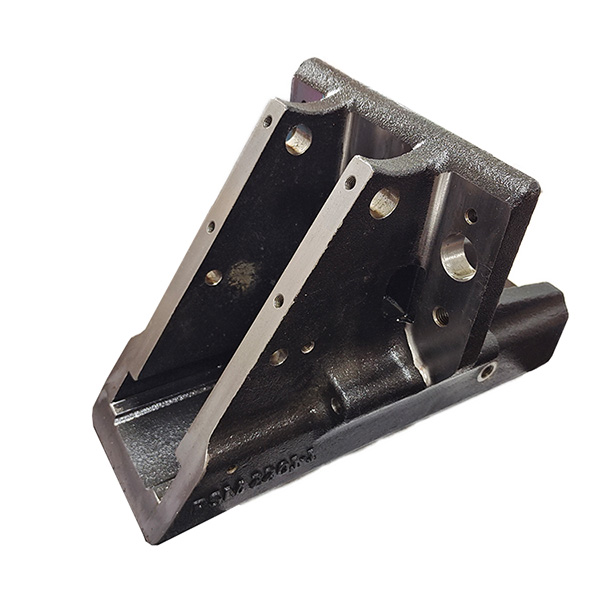
Sample
1. Review OEM Drawings and Vehicle Application
Start with the customer's 2D drawings, 3D CAD models or an approved sample and any associated component specification. Confirm whether the part belongs to an engine, brake, steering, suspension, chassis, transmission, exhaust or auxiliary system. Identify interfaces with adjacent assemblies, fit datums, annual demand and whether the drawing includes special or safety-related characteristics.
Where applicable, the review covers load direction, expected vibration, operating temperature, corrosion exposure, fluid-contact surfaces and inspection-critical dimensions. Manufacturing feasibility can be assessed against the supplied requirements, but the vehicle OEM retains responsibility for design validation and end-use regulatory approval.
2. Confirm Material, Process & Acceptance Requirements
Select a proposed route based on the part, not only the industry name. Iron casting may suit a specified brake rotor or engine housing; aluminum casting may suit a gearbox case; steel closed-die forging may be appropriate for a crankshaft, tow hook or knuckle. Sheet fabrication may be more suitable for frame panels or guards. Discuss casting allowance, final machining, heat treatment and finishing before finalizing the scope.
Confirm the approved alloy and grade, condition, required material documentation, critical GD&T, sample quantities, and inspection or test standards. For brake, steering, towing or other safety-related components, the RFQ should specify any required customer qualification, special process approval or supplier certification; none is assumed to apply universally.
3. Plan Tooling, Prototypes & Process Controls
Casting and forging projects may require tooling review covering draft, parting direction, core arrangement, metal flow, wall transitions, expected shrinkage and machining allowance. CNC projects need datum selection, fixture access and tool paths; fabricated components require form and joint planning. The resulting tooling and sample sequence is defined by geometry, quantity and approved commercial scope.
Initial articles can be used to review casting soundness in relevant areas, forging flash or transition regions, machinability, assembly access and coating compatibility. Sample lead time is quoted for each program instead of applying a fixed 30–45 day promise to every casting, forging or machine part.
4. Inspect Samples and Verify Critical Characteristics
Sample acceptance should be based on the drawing and inspection plan, including appropriate dimensional measurement of bores, tapers, bolt patterns, sealing faces, runout, parallelism, true position and surface finish. Gauges, CMM inspection, visual checks or trial-fit arrangements are selected according to component size and specified tolerances. Brake friction surfaces and transmission bearing seats warrant different inspection priorities.
Material composition, hardness, tensile properties, NDT, leakage or pressure testing, coating evaluation and other examinations are included only when specified and suitable. Fatigue, crash, braking, emissions and whole-vehicle performance validation are not established through routine dimensional checks on isolated metal components.
5. Control Repeat Production and Engineering Changes
After sample and specification approval, the manufacturing plan identifies controlled processes, work instructions, inspection points, tooling maintenance and customer-agreed records. Production attention may include core location and casting consistency, forging temperature and die condition, heat-treatment control, machining datums, deburring, cleanliness, protective finish and packing of functional interfaces.
Drawing revisions, proposed alloy changes and deviations affecting critical dimensions should be reviewed and approved through the applicable customer process. Where required by the OEM, production part approval documentation, traceability or statistical controls must be specifically agreed; a supplier cannot claim IATF 16949 certification or PPAP approval without supporting evidence.
6. Final Inspection, Traceability & Shipment
Final release follows the approved acceptance criteria and sampling or designated 100% inspections. Depending on the component, review dimensional records, material identification, hardness or other specified properties, visual condition, coating coverage, burr removal, protected machined faces and shipment marking. Rotor faces, precision tapers, splines and bearing bores require appropriate packaging to prevent transit damage.
Inspection reports, material certificates, heat-treatment records, NDT results or customer formats can be provided when included in the order. Refer to the SIMIS quality control page and agree on any third-party witness requirements in advance. The supplied paperwork should describe tests actually performed and must not be represented as vehicle-system approval.
Truck & Automotive Parts Manufacturing Processes
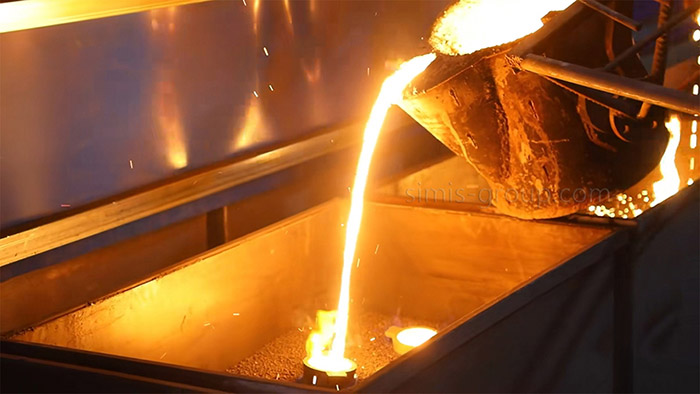
Casting for Engine, Brake & Transmission Parts
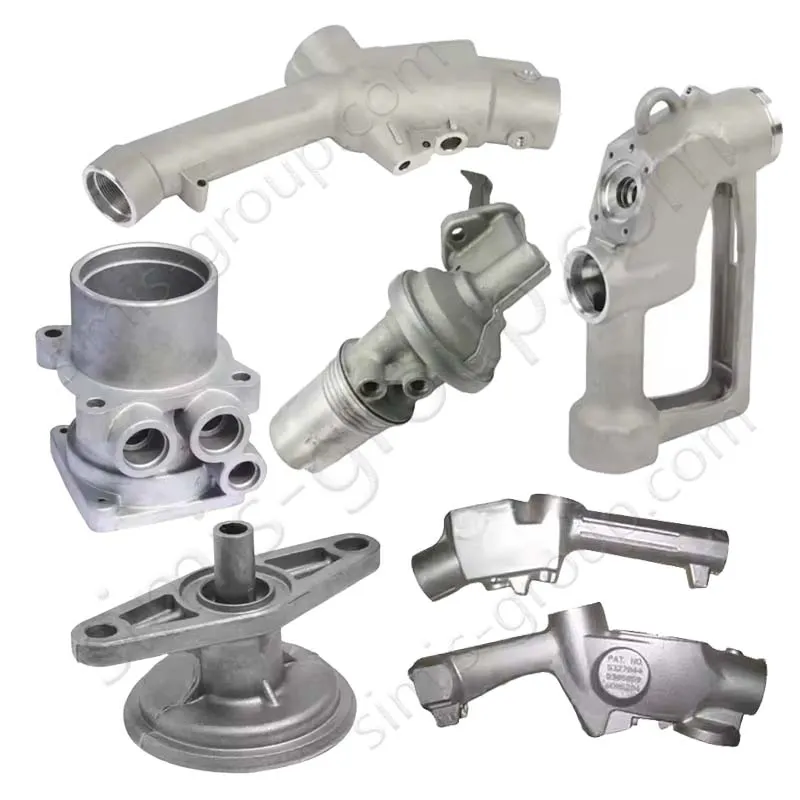
Iron casting may produce customer-specified engine blocks, brake discs, drums and mechanical housings; aluminum casting may suit gearbox covers, throttle housings and other lightweight equipment parts. Routes such as sand casting and pressure die casting are chosen according to alloy, wall geometry, core requirements, batch quantity and intended supply condition.
Casting plans should address shrinkage, feeding, porosity sensitivity, machining allowance and inspection locations. Critical bores and sealing surfaces often require subsequent CNC machining.
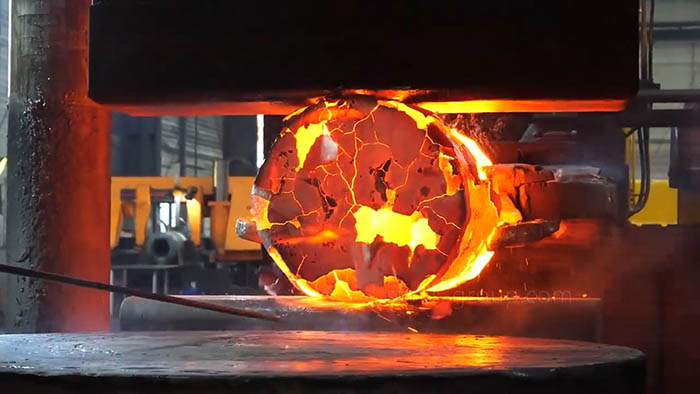
Forging for Shafts, Knuckles & Towing Fittings
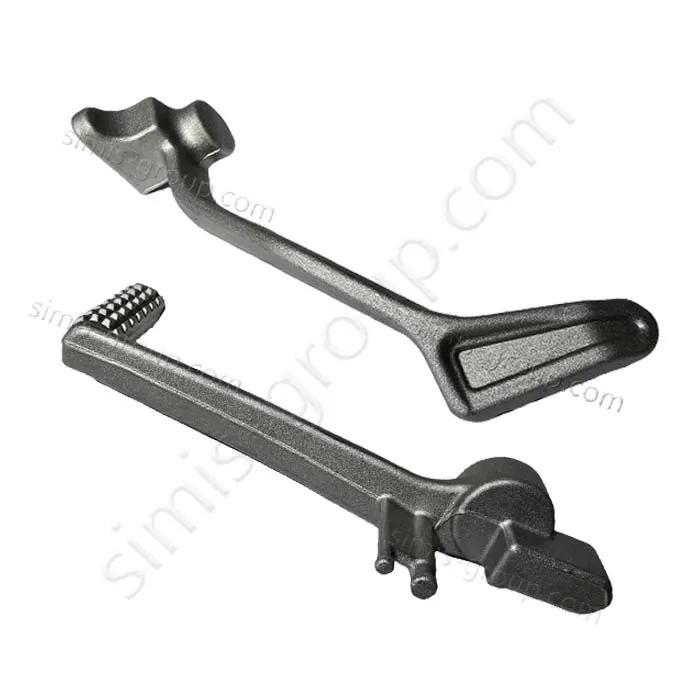
Steel forging can be evaluated for crankshafts, connecting rods, selected steering knuckles, yokes and towing hardware requiring specified mechanical properties. Closed-die forging may suit repeat-production shapes, with CNC machining used for splines, bores, tapers and mating faces. Selected aluminum suspension and bicycle parts may follow an appropriate aluminum-forging route.
Forging feasibility depends on die geometry, grain-flow considerations, heat treatment, finish dimensions and volume. Forging alone does not prove component fatigue life or approval for vehicle service.
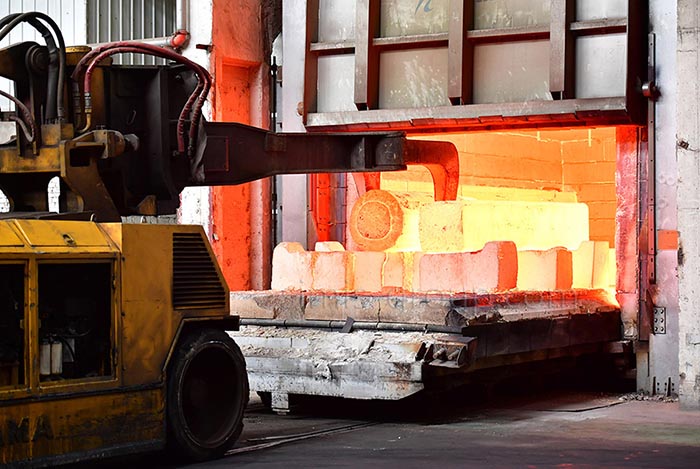
Heat Treatment for Drivetrain & Load-Bearing Parts
Heat treatment may be specified for alloy-steel shafts, gears, forged linkages, connecting rods and selected castings to obtain approved hardness, strength or wear properties. Appropriate cycles depend on grade, section size and the required final condition; surface hardening may be considered for suitable contact areas when requested.
Planning should account for distortion of bearing fits, tapers, splines and sealing faces. Material properties and case depth, where relevant, must be verified to the agreed drawing and inspection specification.
CNC Machining of Vehicle Metal Components
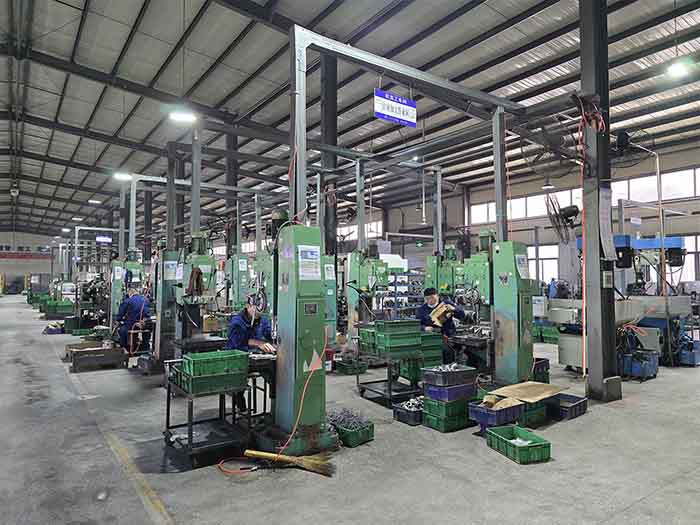
CNC machining can finish casting and forging blanks with bearing bores, cylinder decks, caliper cavities, bolt patterns, threads, spline interfaces and sealing faces. For gearbox housings and shafts, datum selection and workholding are particularly important to bore alignment, true position and runout.
Machining and inspection should follow customer-defined tolerance zones, surface roughness and cleanliness requirements. Deburring and protection of functional edges or fits are included in the agreed process plan.
Sheet Metal Fabrication for Vehicle Brackets
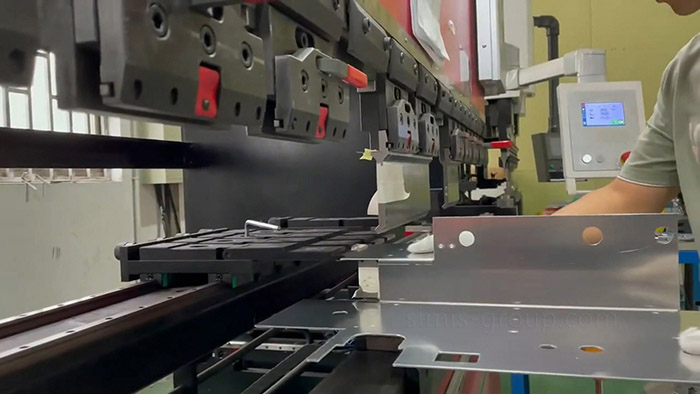
Sheet metal fabrication may suit body mounting brackets, battery or electronics supports, guards, covers, storage enclosures and selected chassis attachments. Cutting, forming, stamping and welding options depend on plate thickness, bend geometry, specified steel or aluminum grade and order quantity.
Manufacturability review covers bend radii, hole locations, weld access, distortion, joining details and the final protective finish. Large vehicle panels and complete chassis assemblies should not be represented as normal closed-die forgings.
Surface Treatment & Corrosion Protection
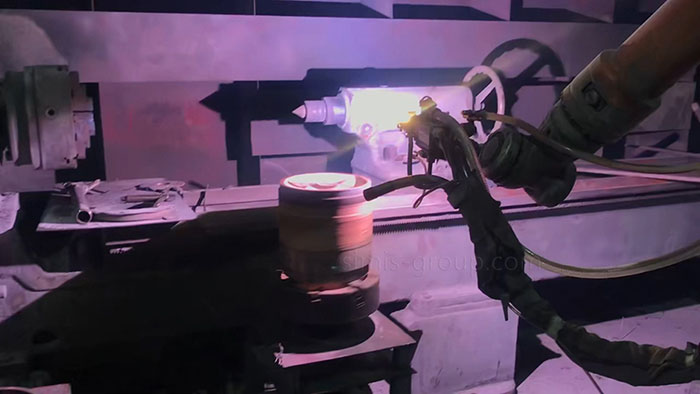
In the car and truck industries, surface treatments are used on many parts. This includes brake components, exhaust systems, and suspension parts. These treatments boost corrosion resistance, wear resistance, and durability. They protect parts from weather and driving factors. This helps cut down on maintenance and makes the parts last longer. Ultimately, this ensures reliable performance in all driving conditions.


