Custom Steel Forging Manufacturer in China
Steel Forging Processes & Manufacturing Capabilities
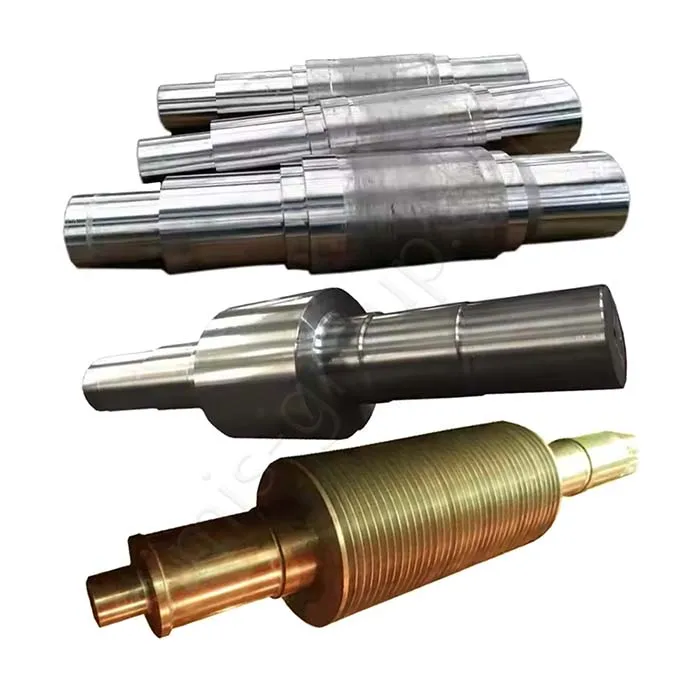
Steel Open Die Forging
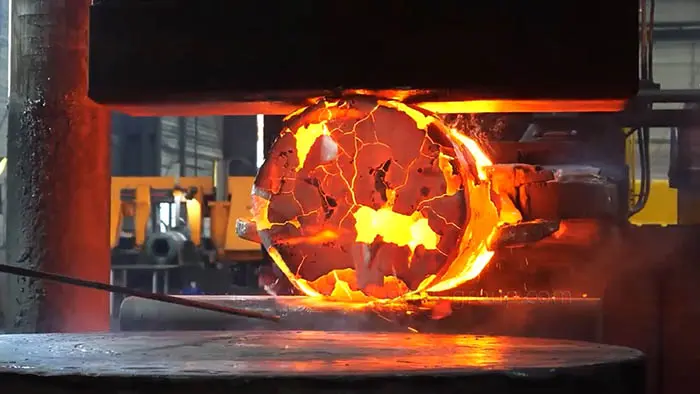
SIMIS supports custom open-die steel forgings for large shafts, rollers, discs, blocks and heavy machinery components. We review the specified carbon, alloy or stainless steel grade, section size, forging reduction, heat treatment and machining allowances before selecting the manufacturing route. Rough-machined or finished forgings can be discussed according to your drawings.
Forging weight reference: 10–1,500 kg
Maximum dimensions: diameter up to 1,200 mm; length up to 4,000 mm
Main press equipment: 2,000-ton and 4,000-ton hydraulic presses
Steel Closed Die Forging
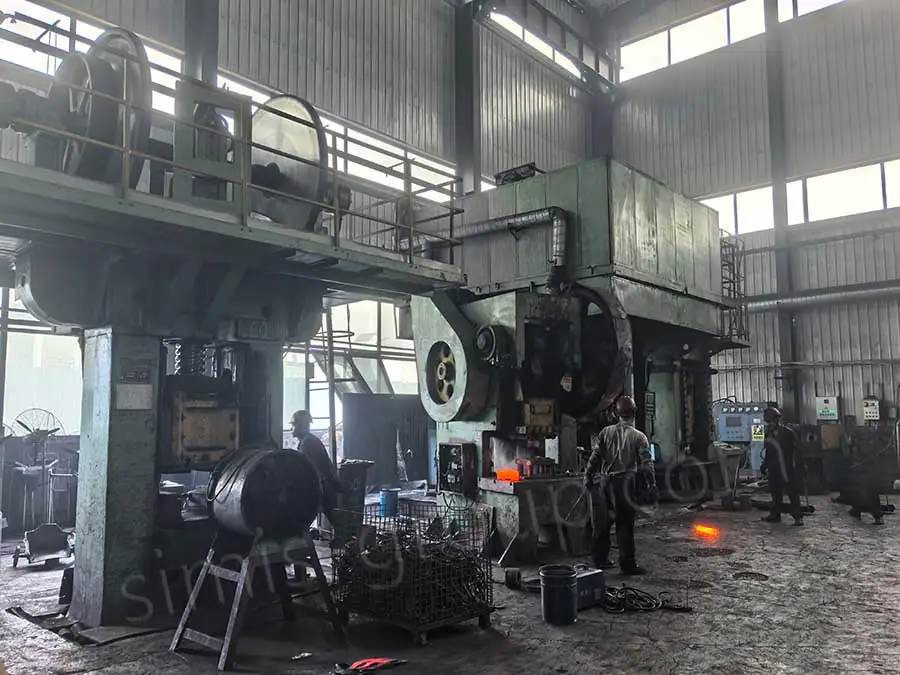
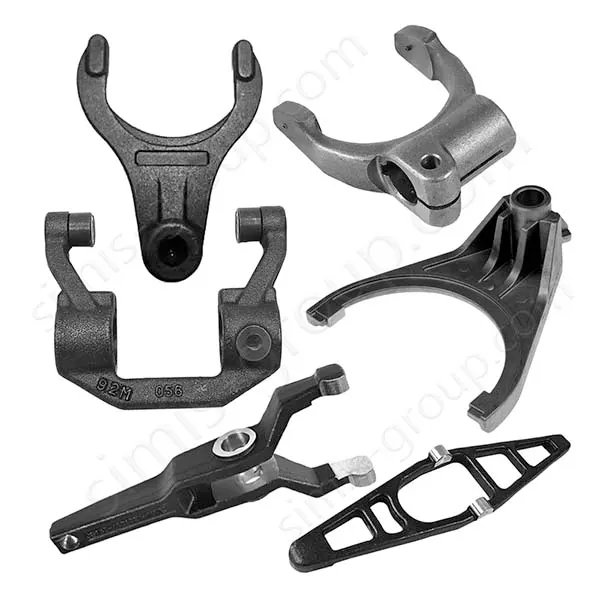
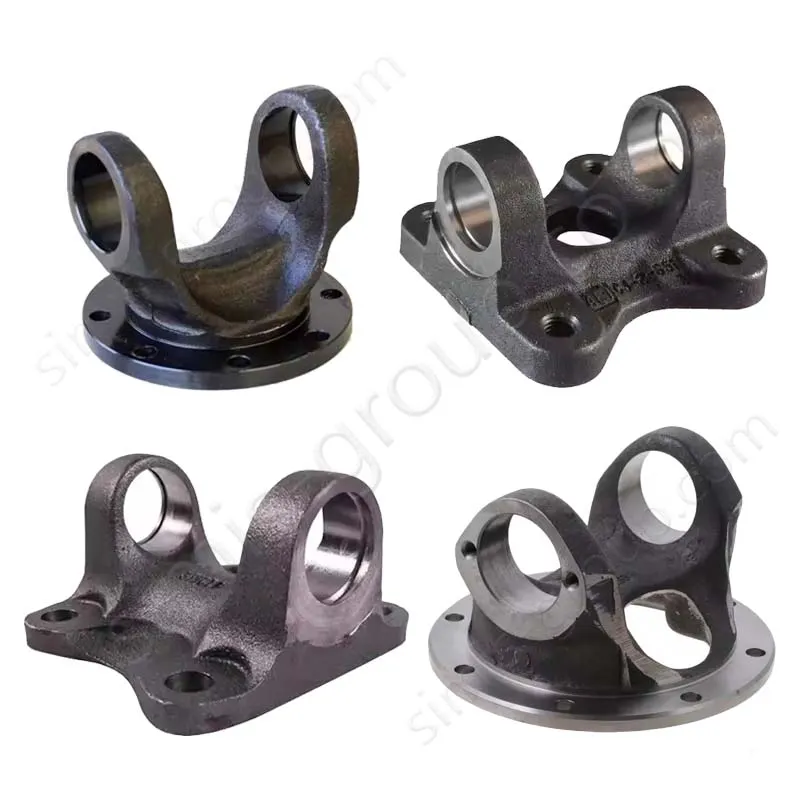
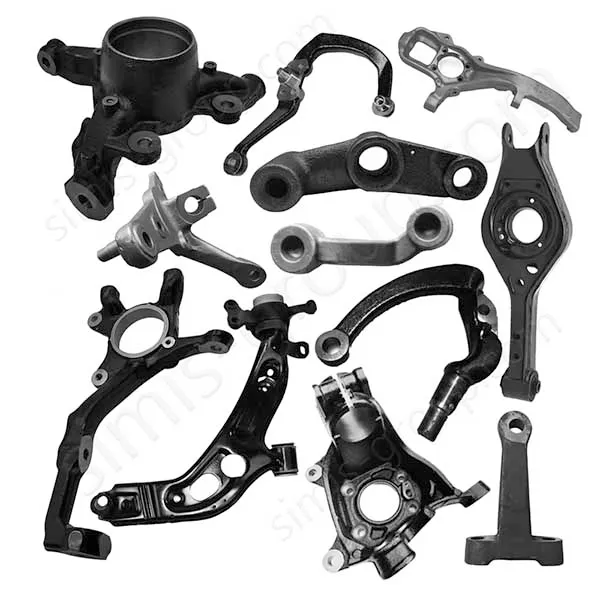
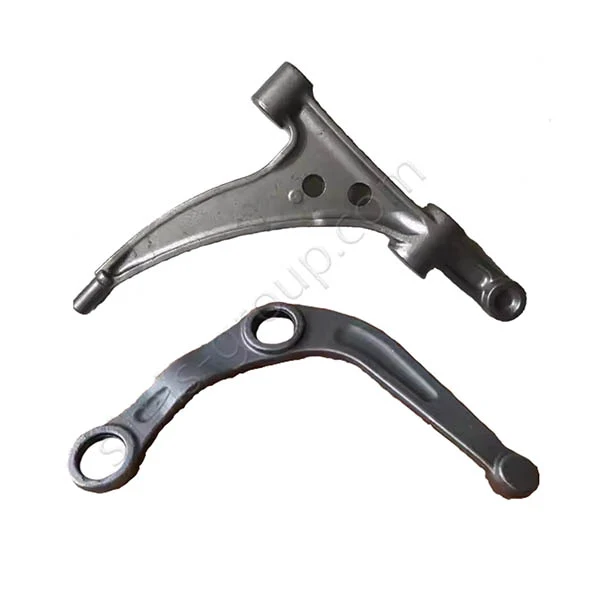
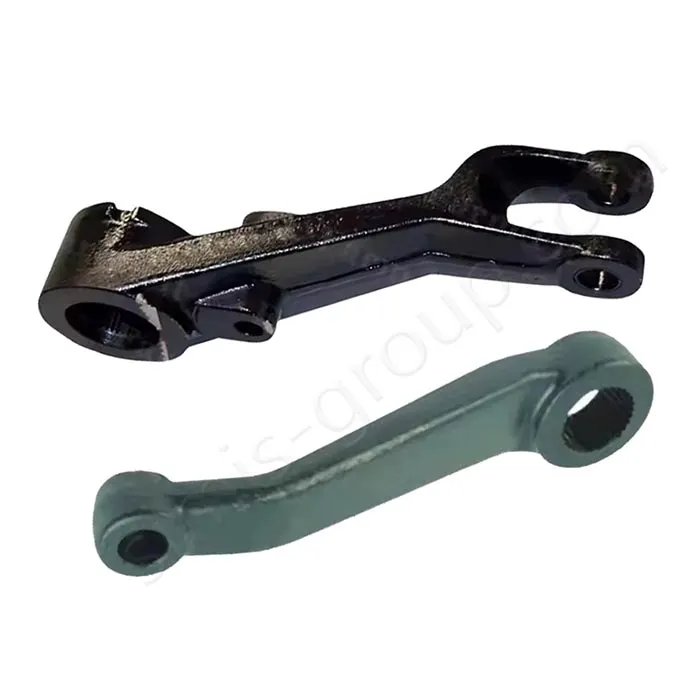
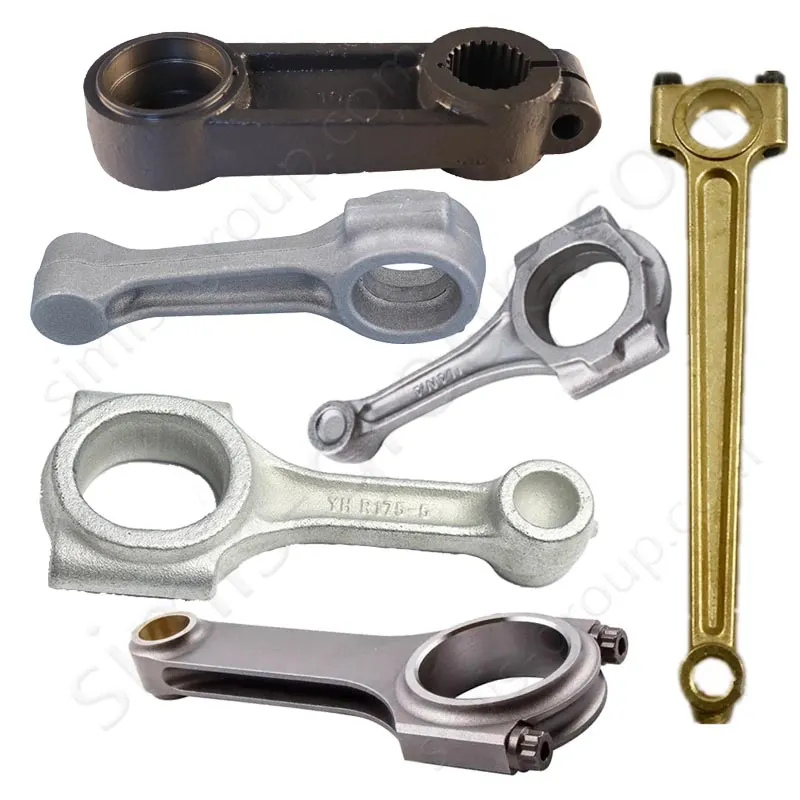
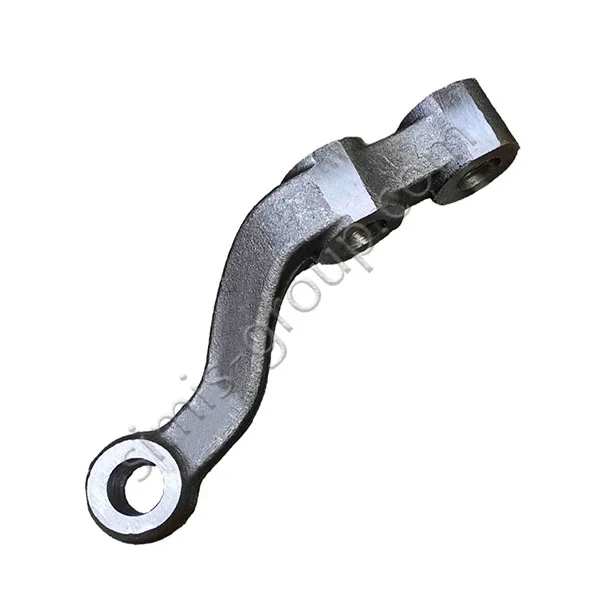
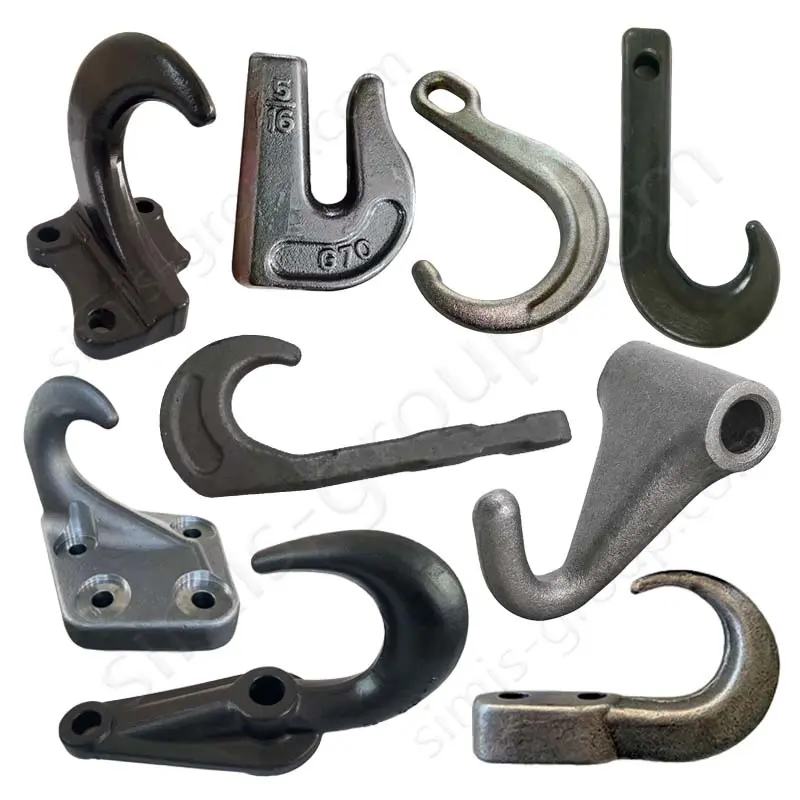
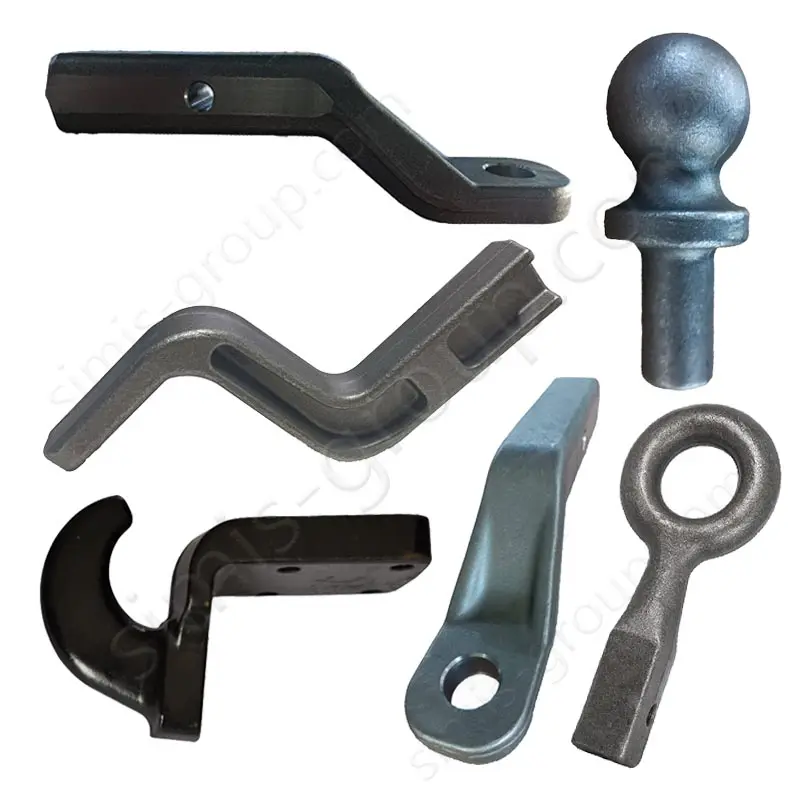
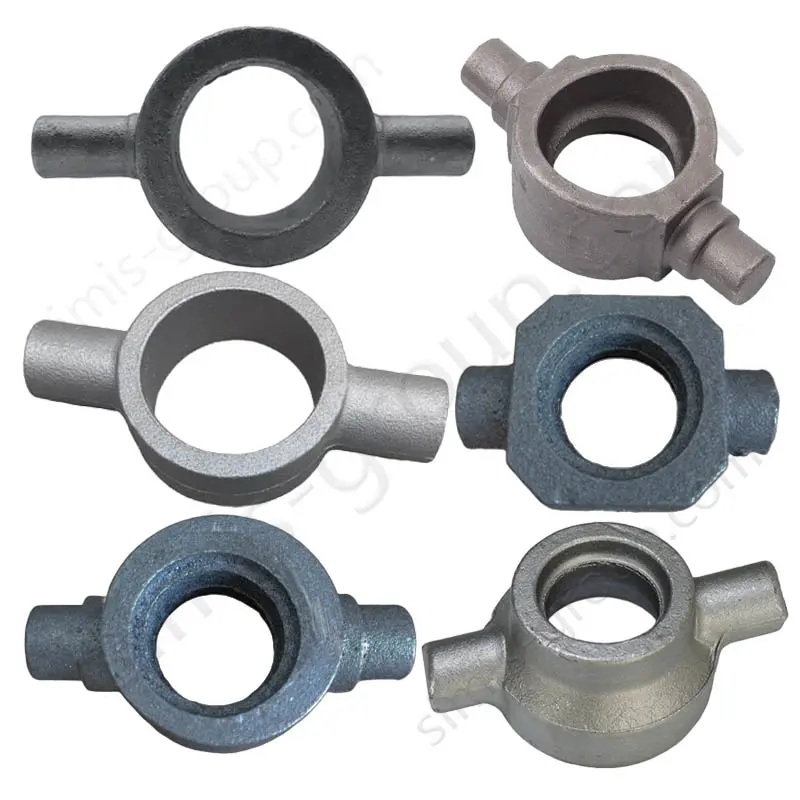
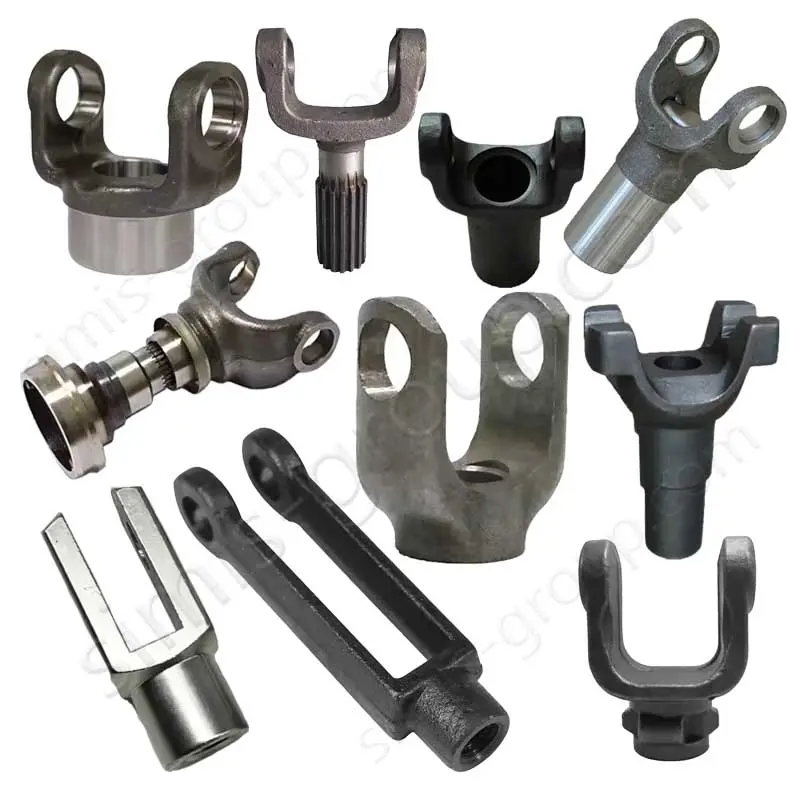
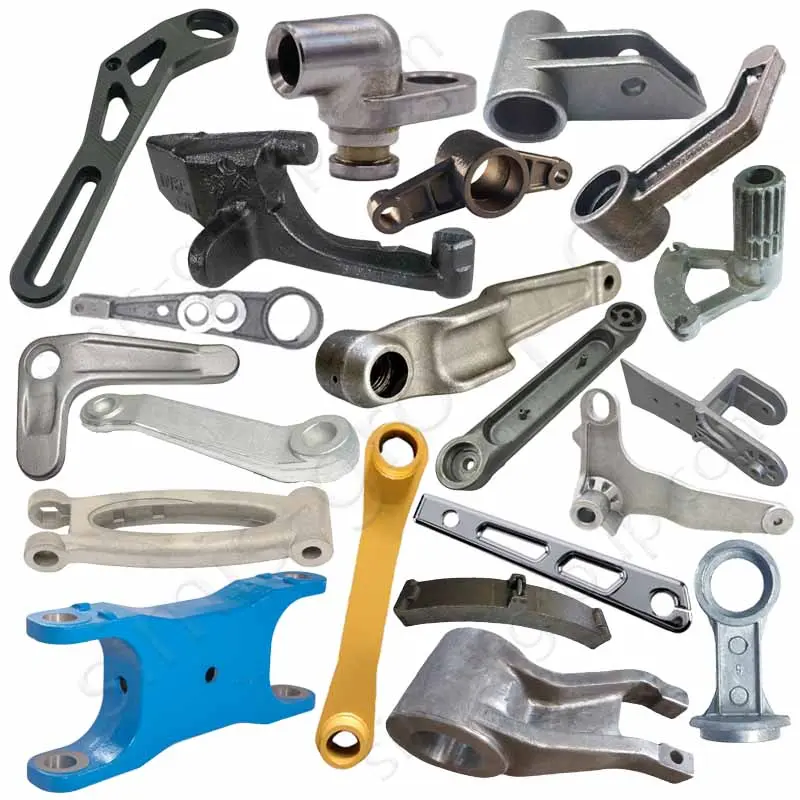
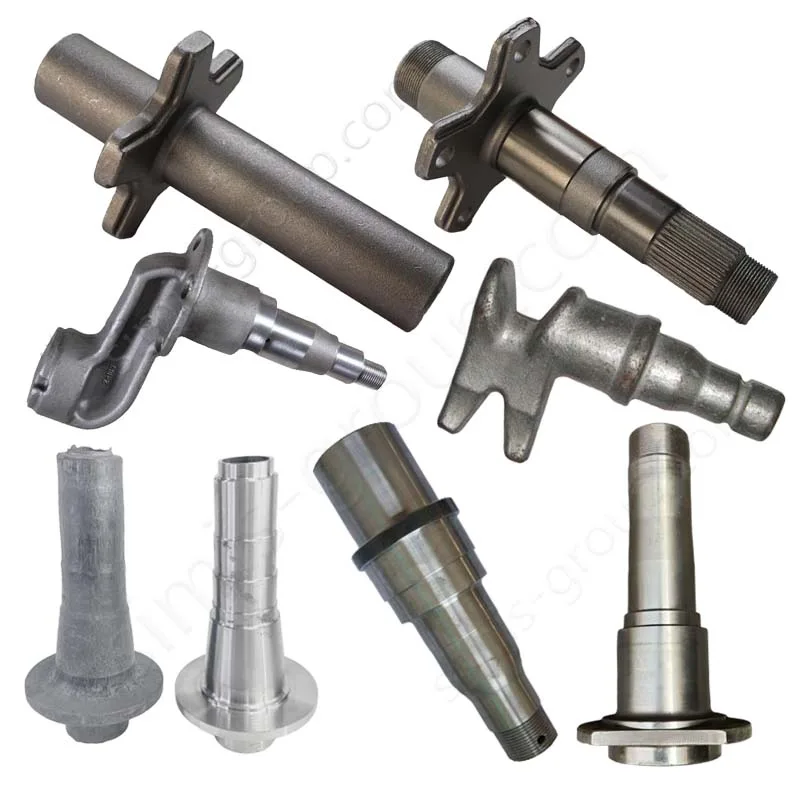
SIMIS provides closed-die steel forging for repeat-production components such as steering knuckles, connecting rods, yokes, levers and suspension parts. The process is selected according to the required steel grade, part geometry, production quantity and mechanical performance. Die design, flash trimming, heat treatment and CNC machining are reviewed before tooling approval.
Forging weight: 0.1–100 kg
Maximum forged dimensions: 600 × 400 × 200 mm
Forming equipment: 1,600-, 2,500- and 4,000-ton closed-die presses
Machining allowance reference: 1.5–5 mm, subject to part and tooling design
Steel Ring Rolling Forging
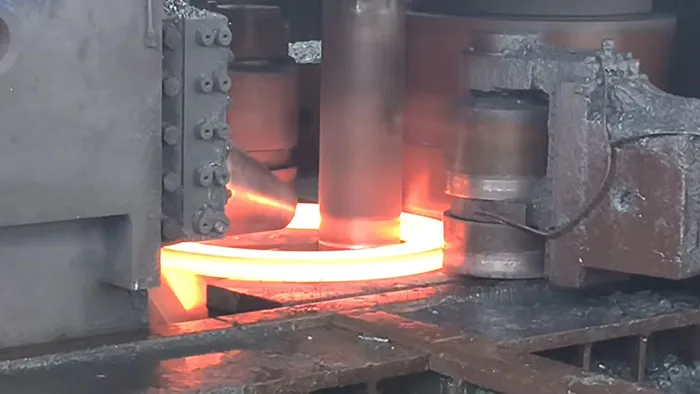
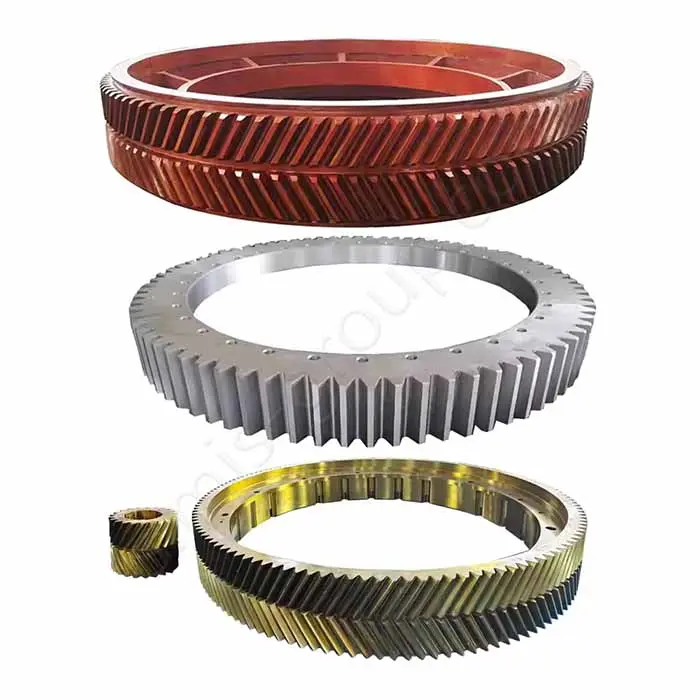
SIMIS supports ring rolling for seamless steel rings used in bearing, gear, flange and industrial rotating assemblies. We assess the steel grade, outside and inside diameters, wall section, height, heat-treatment condition and subsequent machining. The selected ring-rolling route is confirmed against the part drawing and production-line capacity.
Outside-diameter range: Ø300–Ø2,500 mm
Maximum ring height: 400 mm
Single-piece weight: 10–1,500 kg
Steel Cold Forging
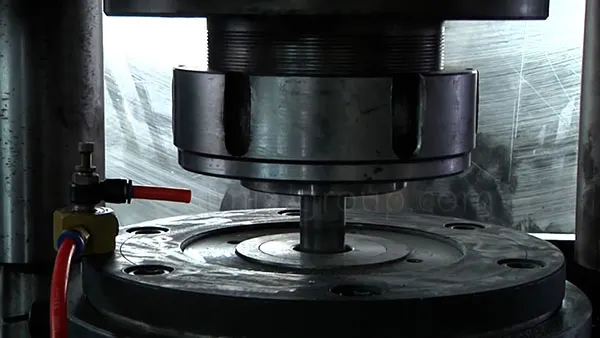
SIMIS supports cold forging and extrusion for suitable low- and medium-carbon steel components in repeat production, including pins, sleeves, fastener blanks and precision transmission parts. We review material formability, forming stages, die life, required dimensions and any subsequent heat treatment or machining before confirming the route.
Part weight: 5 g–3 kg
Maximum dimensions: diameter up to 100 mm; length up to 200 mm
Forming equipment: 300–1,200-ton cold-extrusion presses; multi-station cold heading
Steel Heat Treatment
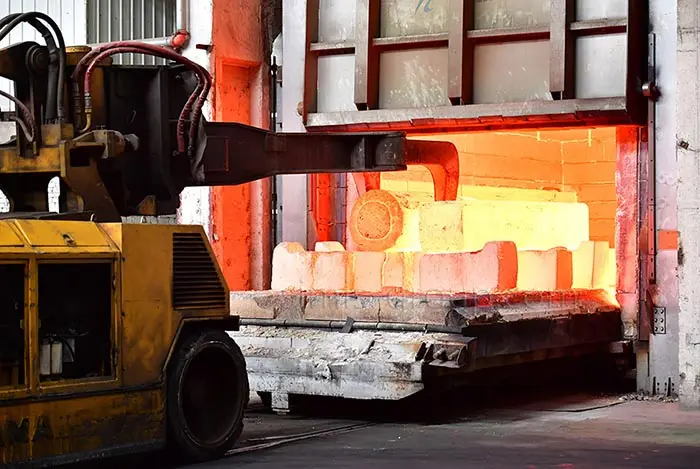
SIMIS coordinates heat treatment for steel forgings to achieve the specified mechanical properties and machining condition. The route is selected according to the approved steel grade, forging section and customer requirements. Heat-treatment cycles and testing are agreed before production, particularly for load-bearing or fatigue-sensitive components.
Annealing and normalizing: selected to suit structure, hardness and machinability requirements
Quenching and tempering: applied where the specified steel grade and strength/toughness requirements call for it
Stress relief and surface hardening: evaluated when appropriate for the component and equipment

Steel CNC Machining
SIMIS offers CNC turning, milling, boring, drilling and finishing for forged steel components such as shafts, rings, yokes and flanges. Machining establishes the specified bores, bearing seats, threads, mating faces and geometric tolerances after forging and any required heat treatment. Critical characteristics are inspected against the approved drawing.
CNC turning reference: Ø10–Ø800 mm; machining length up to 1,500 mm
Vertical machining center travel: X 1,000 × Y 600 × Z 600 mm
Horizontal machining center: four-axis; 630 × 630 mm pallet
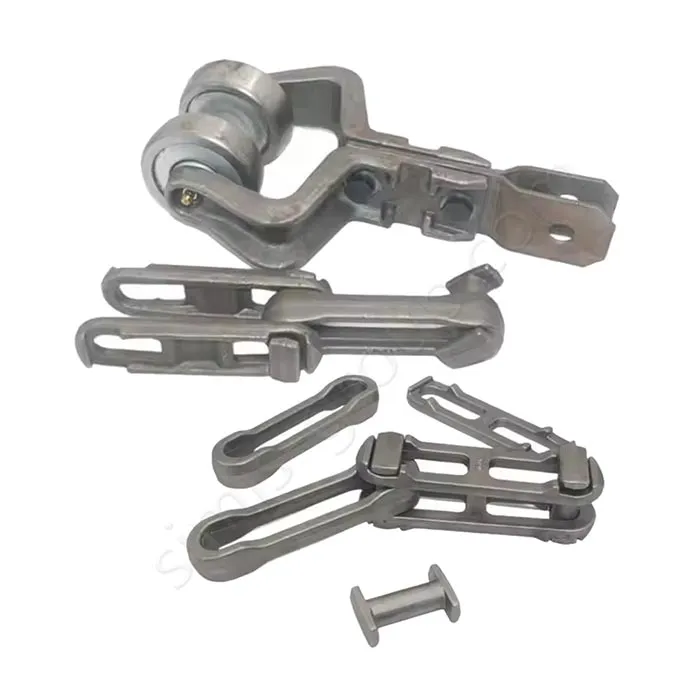
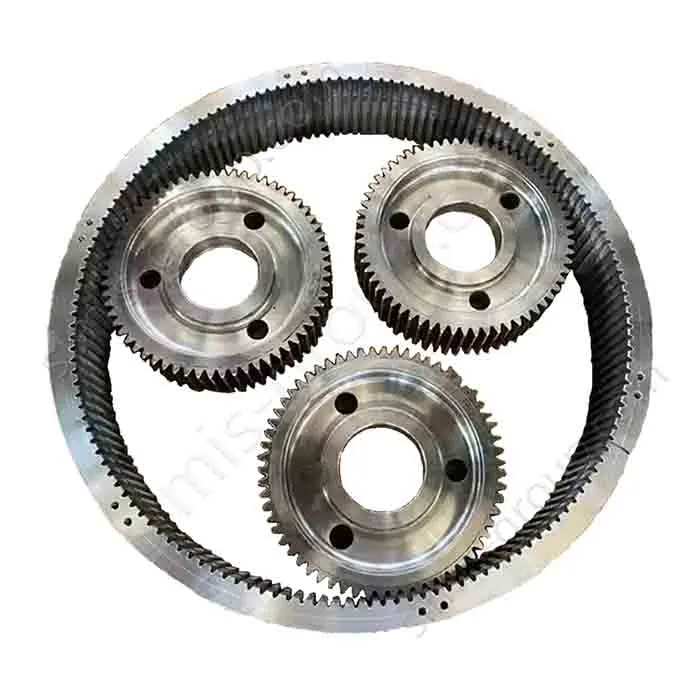
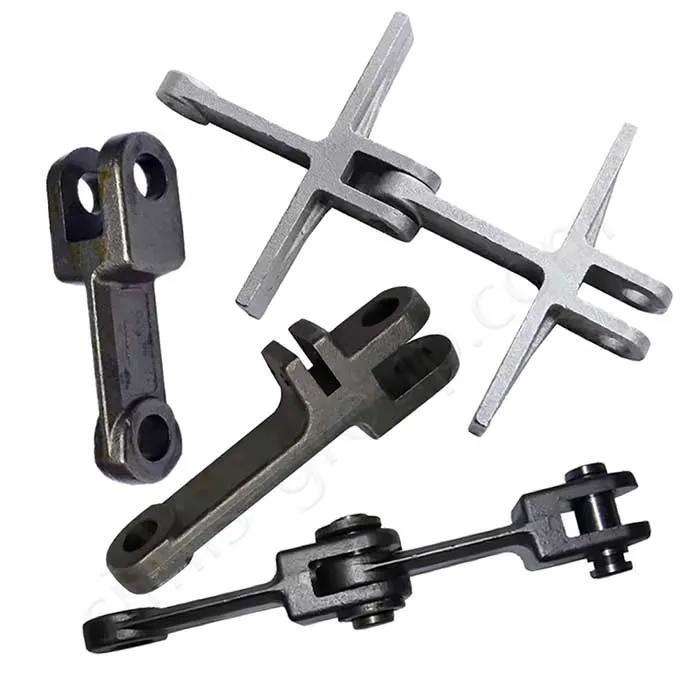
OEM Custom Steel Forgings & Components
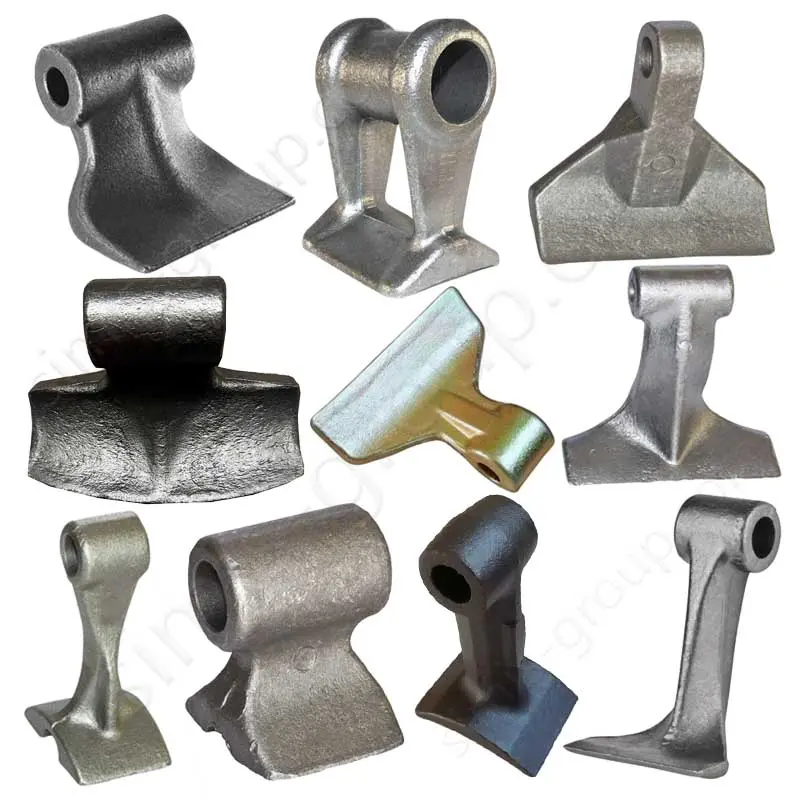
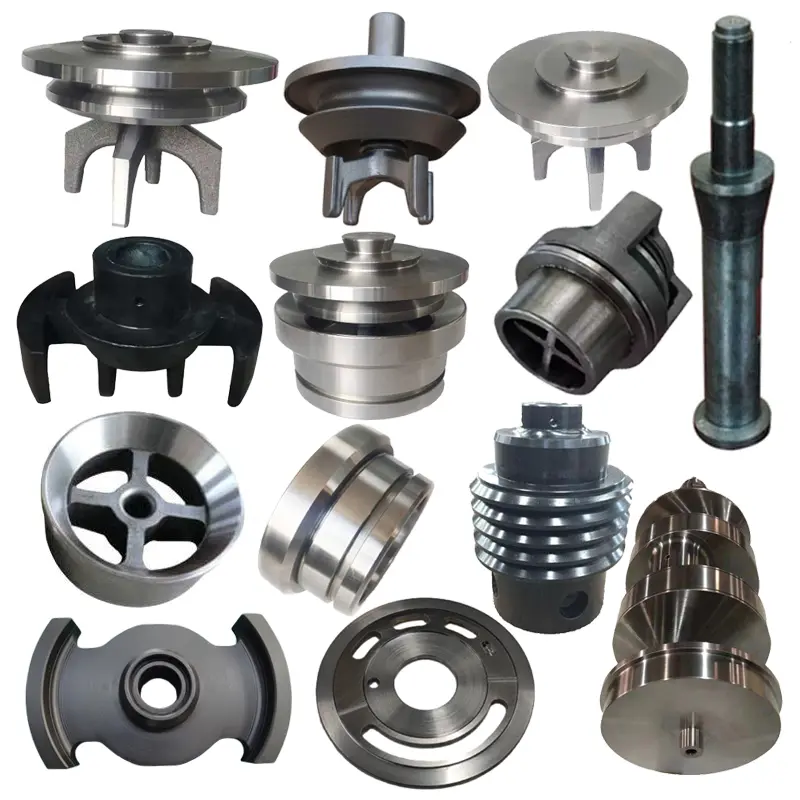
Carbon, Alloy & Stainless Steel Forging Materials

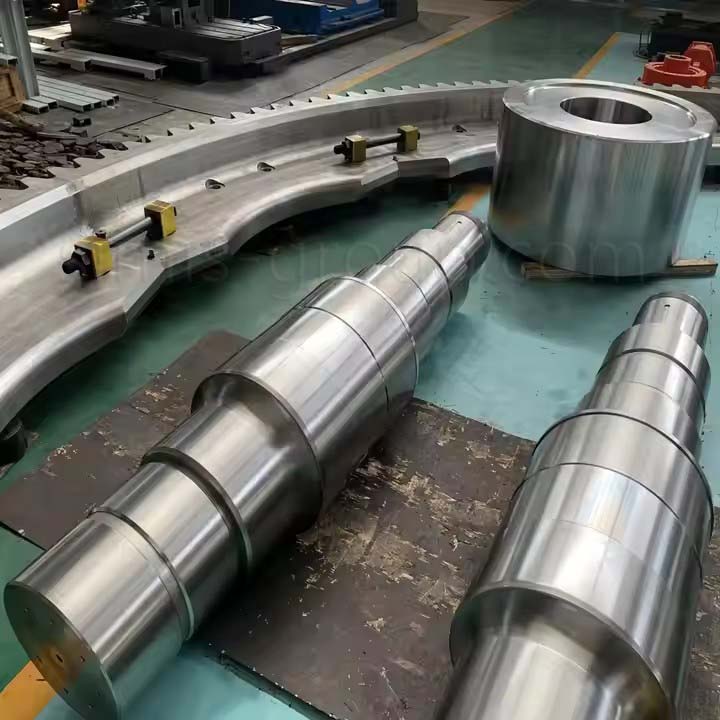

Carbon Steel Forging
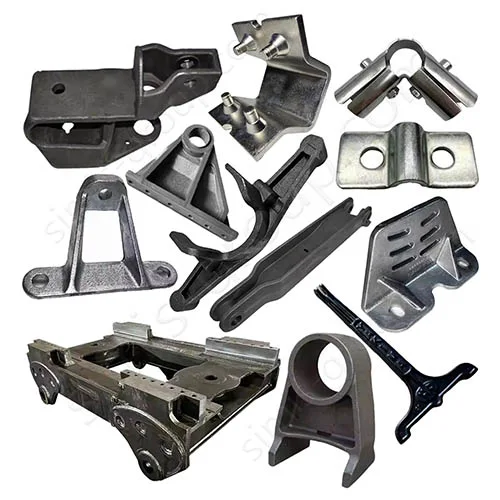
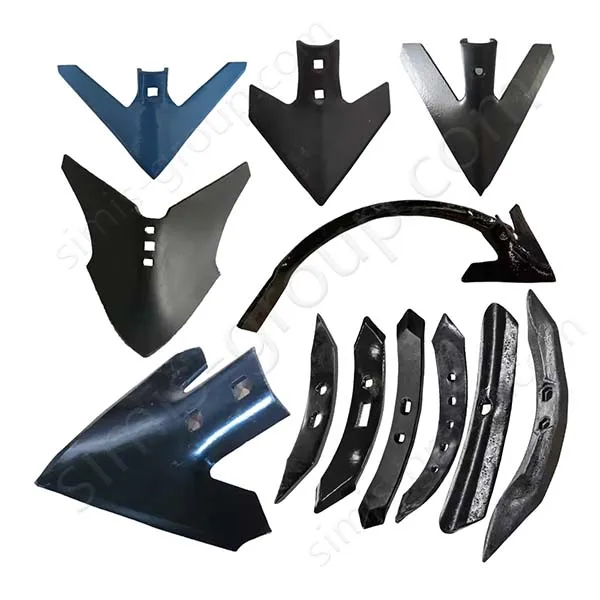
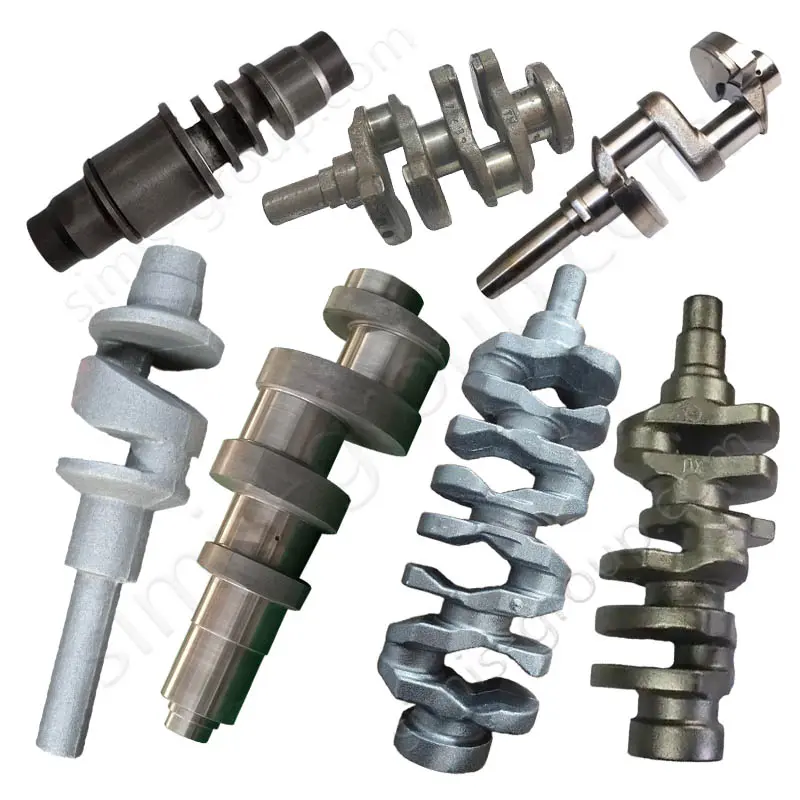
SIMIS provides custom carbon steel forgings for shafts, crankshafts, connecting rods, brackets, agricultural machinery parts and general industrial components. We review the specified carbon steel grade, forging route, section thickness and required strength or hardness. Normalizing, quenching and tempering, and CNC machining are arranged as required by the approved drawing.
Stainless Steel Forging
SIMIS evaluates stainless steel forgings for flanges, valve components, shaft parts, fittings and other industrial components requiring specified corrosion resistance. Material selection covers suitable austenitic, martensitic or other stainless grades subject to the forging process and approved supply route. We confirm material condition, heat treatment, machining and any testing requirements before quotation.
Alloy Steel Forging
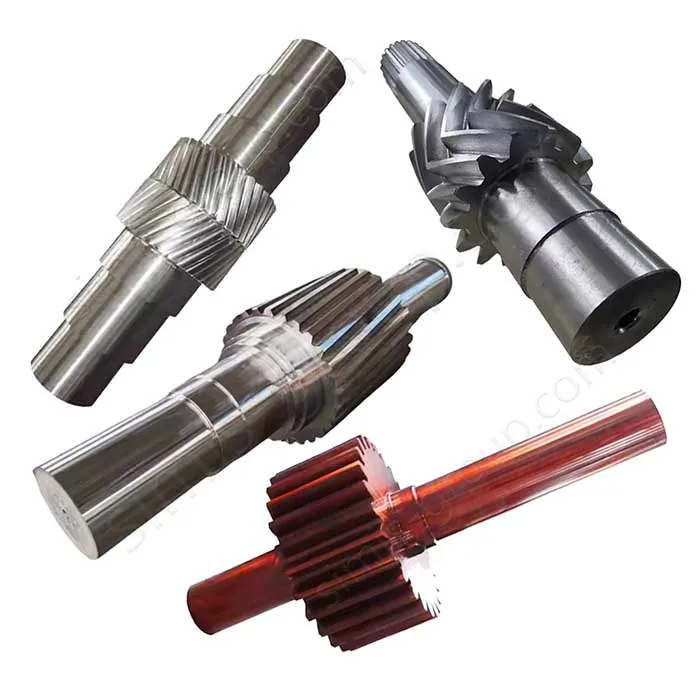
SIMIS manufactures or evaluates alloy steel forgings for gears, drive shafts, pinions, axle components and other load-bearing OEM parts. Chrome-molybdenum and nickel-chrome-molybdenum steel families can be considered according to customer specifications. We assess the grade, forging method, heat treatment, mechanical properties, fatigue-related requirements and finished machining features.
Special Purpose Forged Steel
SIMIS can review customer-specified specialty steel forging projects, including selected tool steels, bearing steels and other grades with demanding wear, strength or service requirements. Material availability, forgeability, heat-treatment route and inspection requirements must be confirmed before accepting the order. Specialty or highly regulated applications are evaluated individually rather than treated as standard catalogue capabilities.
Industries Served by Our Steel Forging Factory
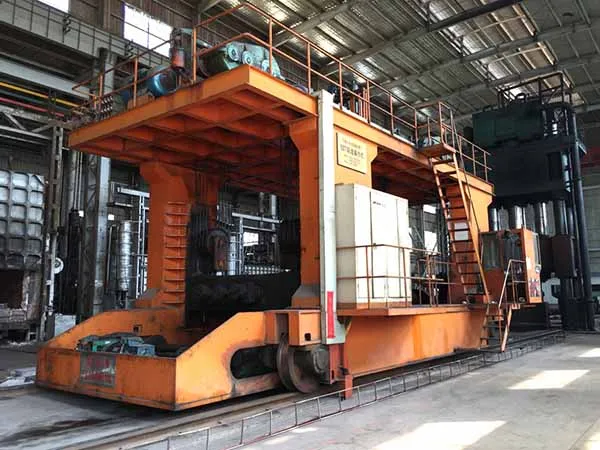
Custom Steel Forgings: From Drawings to Production
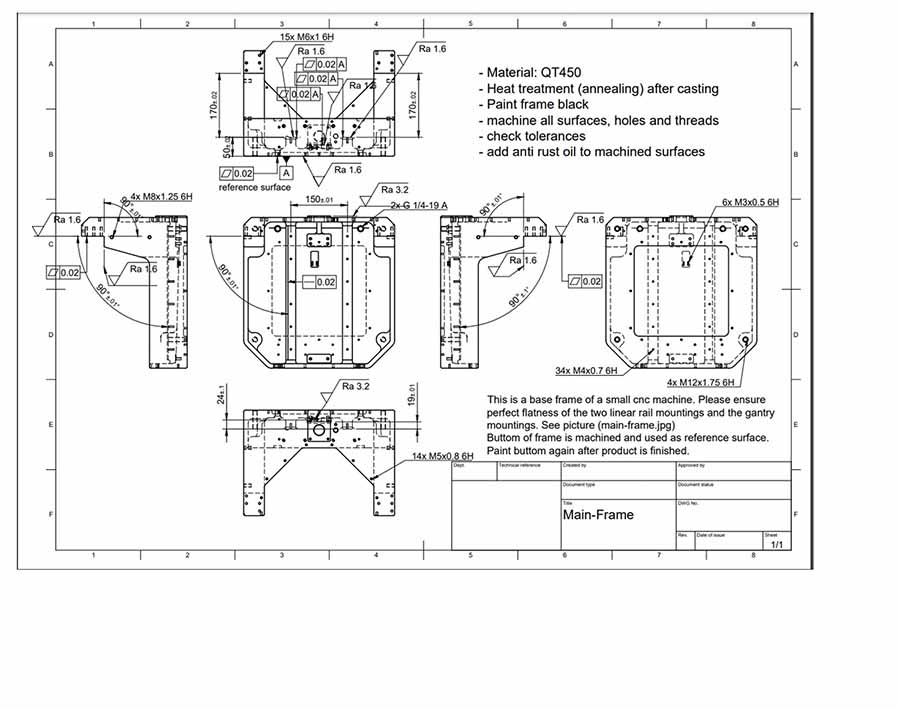

Engineering Review, Tooling & Sample Approval
1. Review Drawings and Application
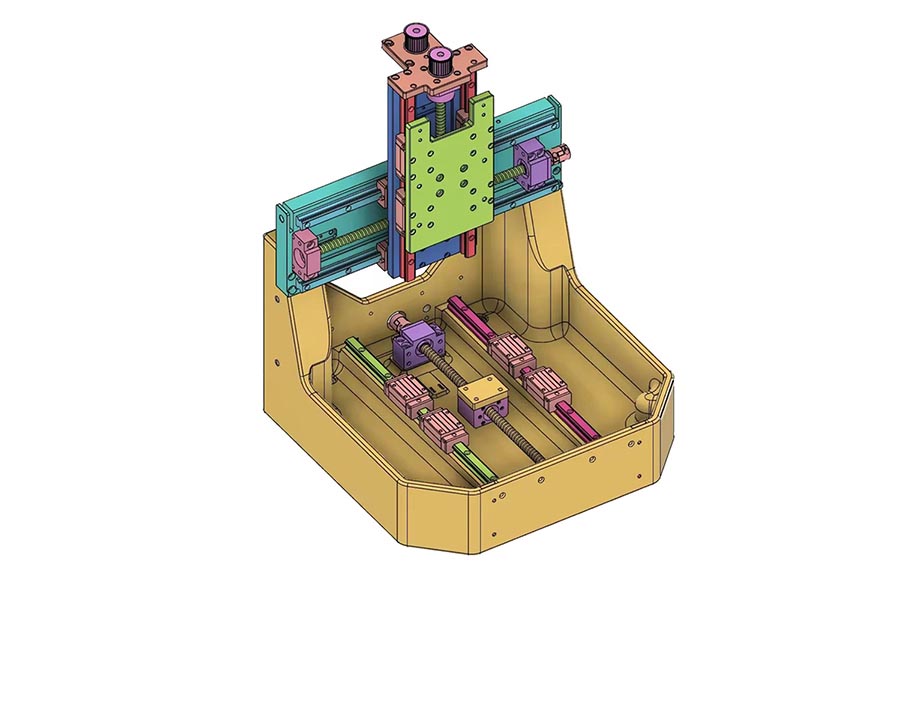
Send 2D drawings or 3D CAD models with the component function, operating loads, critical interfaces, target dimensions and expected production quantity. SIMIS reviews geometry, section transitions, forging direction, possible undercuts, machining allowances and the suitability of the proposed forging route. If only a physical sample is available, reverse engineering requirements are discussed separately.
2. Confirm Steel Grade and Mechanical Requirements
Specify the carbon, alloy, stainless or specialty steel grade and applicable standard, together with required tensile or yield strength, hardness, impact toughness, fatigue-related requirements and service temperature where relevant. Heat-treatment condition and any grain-flow or material-traceability requirements are also reviewed. Material substitutions require customer approval.
3. Select the Forging Process
Assess open-die forging, closed-die forging, ring rolling or cold forging according to part geometry, steel grade, size, quantity, mechanical requirements and tooling economics. We consider forming feasibility, production-line capacity, draft and flash requirements, and the amount of CNC machining needed before confirming the proposed process.
4. Plan Billets, Dies and Machining Allowances
Review billet dimensions, heating and deformation sequence, die or ring preform design, parting line, forging reduction, trimming and controlled cooling. Grain-flow direction, section transitions and machining datums receive particular attention on load-bearing parts. Tooling and machining allowances are finalized against the approved drawings and production route.
5. Produce and Evaluate Initial Samples
Where tooling and sample approval form part of the agreed order, initial forgings are evaluated for dimensions, surface condition, material identification and the fit of critical machined features. Required heat treatment and specified hardness, mechanical or non-destructive testing are included in the sample plan. Necessary corrections are agreed with the customer before production release.
6. Approve Inspection and Acceptance Criteria
Establish acceptance limits for critical dimensions, material chemistry, heat-treatment condition, mechanical properties and surface discontinuities. Depending on the component, the quality plan may specify tensile or impact tests, hardness checks, ultrasonic testing, magnetic particle inspection or penetrant testing. Sampling frequency, traceability and reports are defined by the approved order specification.
Controlled Production, Inspection & Delivery
1. Confirm Production Readiness
Following the required sample or first-article approval, confirm the released drawing revision, steel grade, billet identification, approved forging route, tooling condition, heat-treatment schedule, machining plan and order quantity. Critical inspection characteristics and any agreed traceability records are reviewed before batch production.
2. Monitor Forging, Heat Treatment and Machining
Apply agreed controls to billet heating, forging deformation, cooling, trimming, heat treatment and CNC machining as applicable. Relevant checks may include material identity, dimensions, surface condition, hardness, critical bores and bearing interfaces. Process controls are adapted to the selected steel grade, part geometry and manufacturing method.
3. Perform Final Inspection and Documentation
Inspect finished steel forgings against the released drawing and approved quality plan. Depending on the order, documentation may include dimensional inspection, material certificates, heat-treatment records, tensile or impact results, hardness measurements and specified non-destructive examination reports. No test or report is assumed mandatory unless required by the agreed specification.
4. Package and Dispatch Approved Forgings
Protect machined surfaces, threads, bearing seats and corrosion-sensitive steel parts during handling, packing and transport. Confirm part identification, preservation method, packaging, shipment terms and required documents with the customer before dispatch.
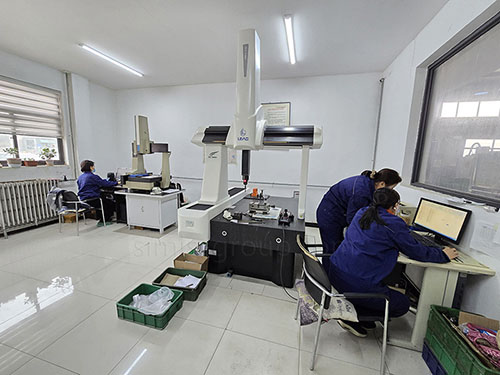
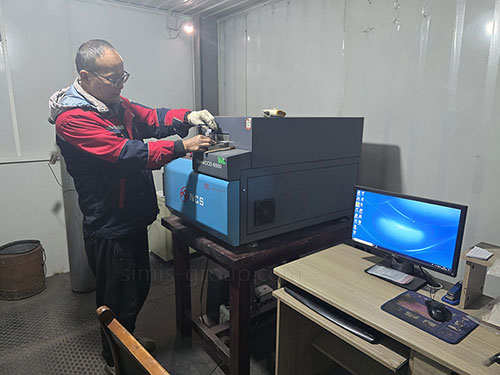
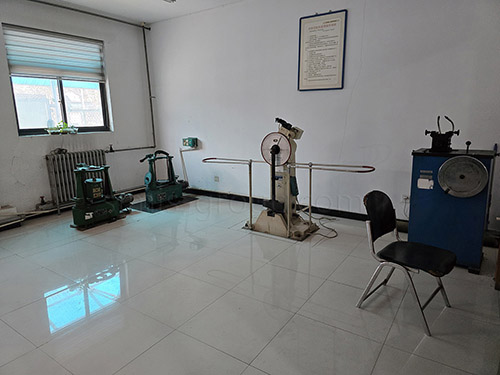
Need custom metal castings or forgings made to your drawings? Send SIMIS your 2D/3D files, material specifications, critical tolerances and estimated quantities. We can review manufacturing feasibility and discuss a suitable production approach for your project.


