Custom Gravity Permanent Mold Casting in China
Custom Gravity Permanent Mold Casting Services & Foundry Capabilities
SIMIS Gravity Casting Manufacturing Capabilities
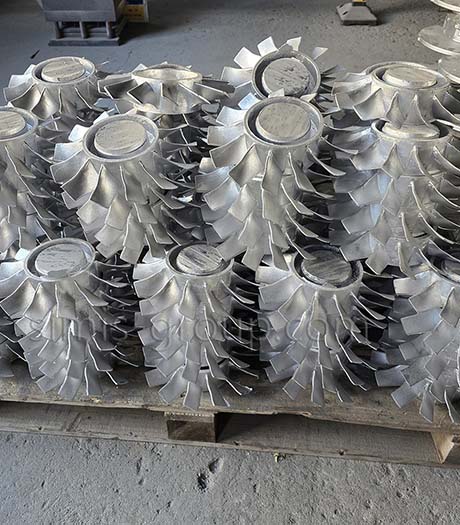
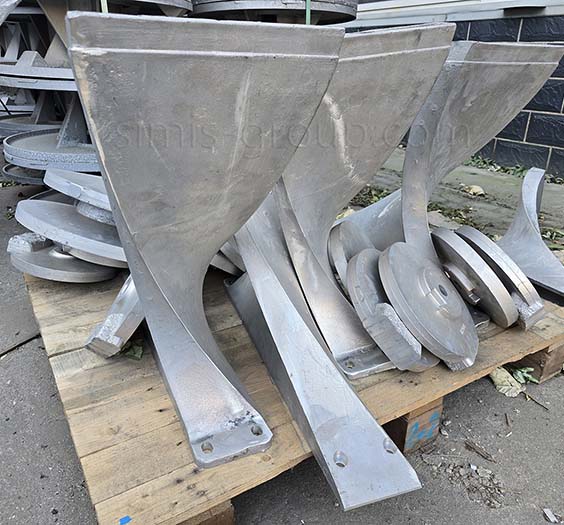
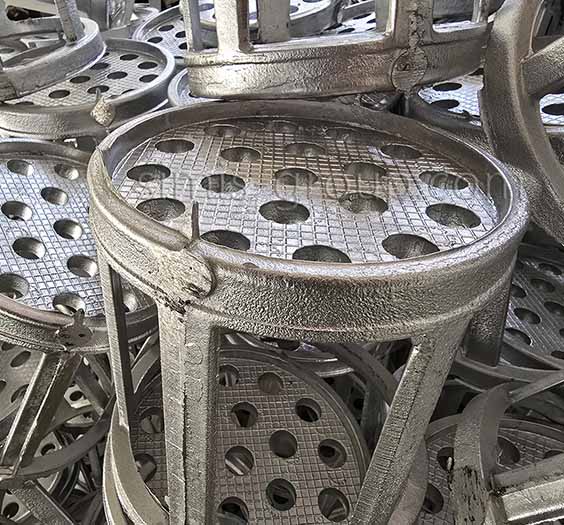
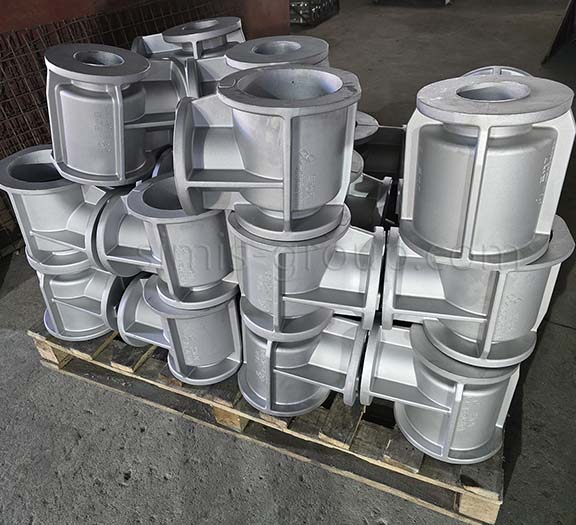
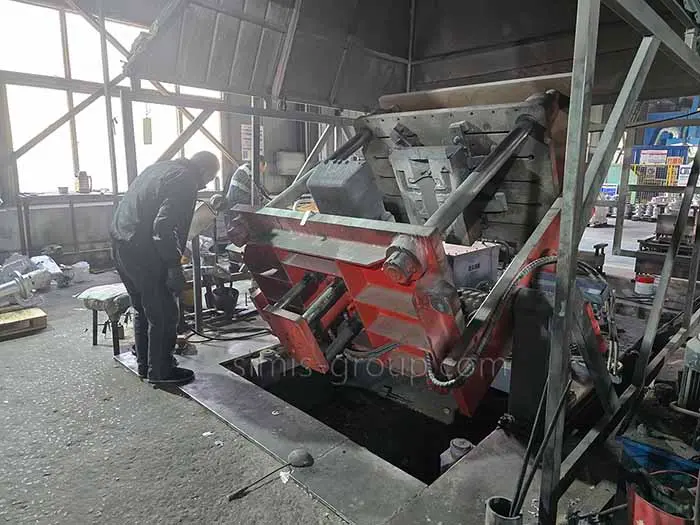
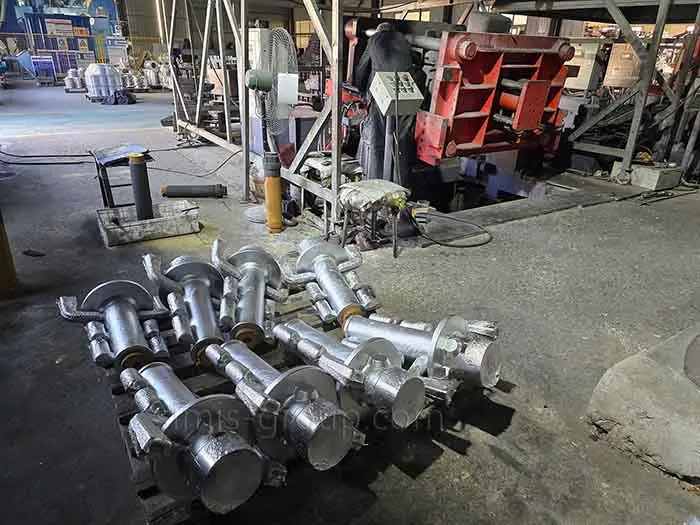
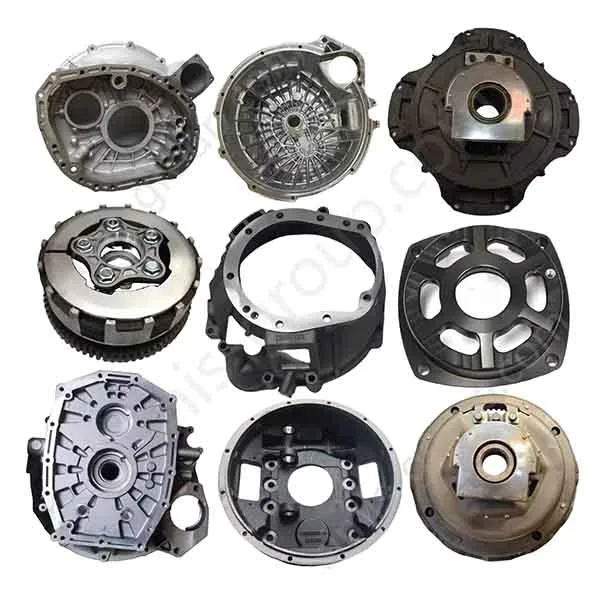
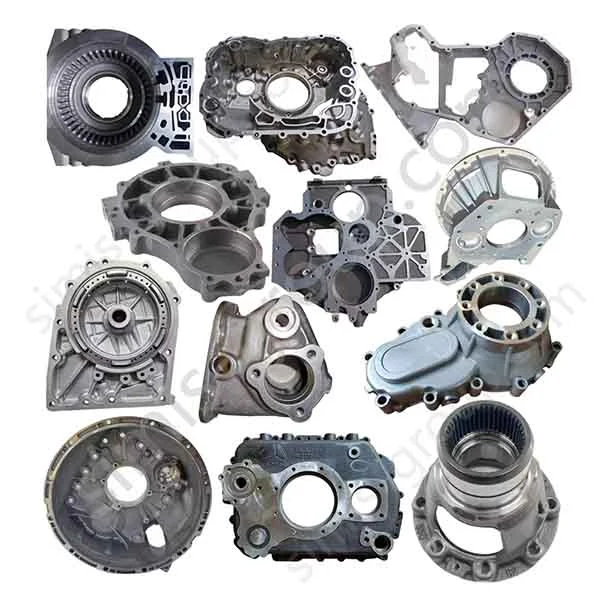
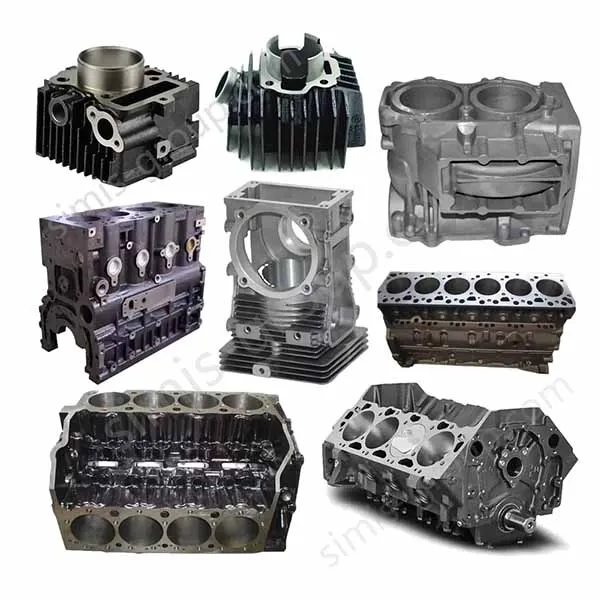
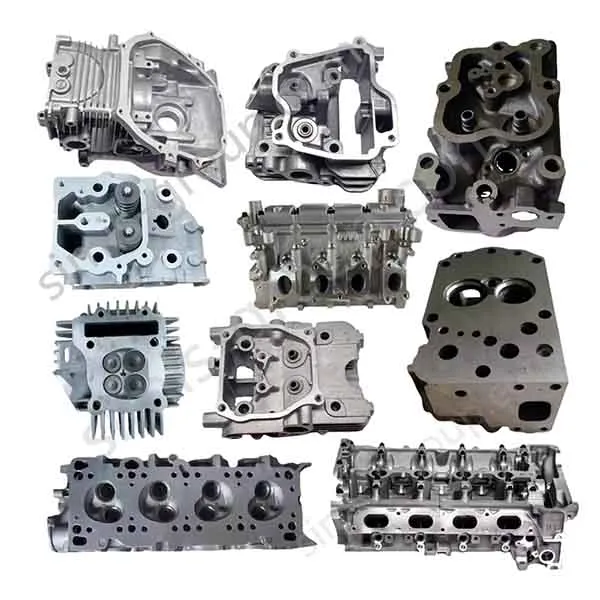
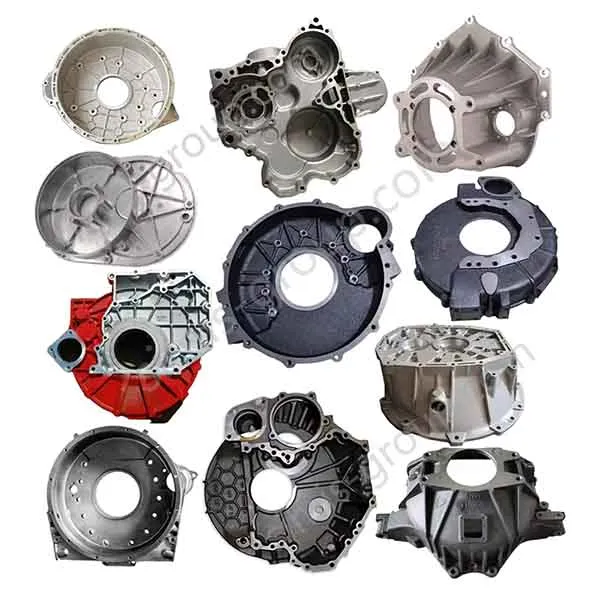
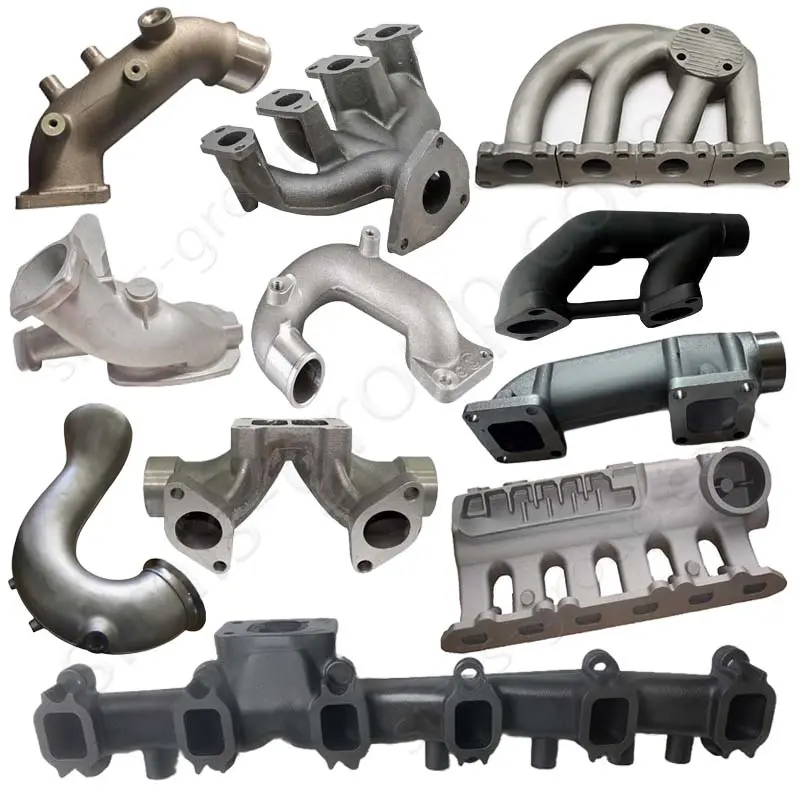
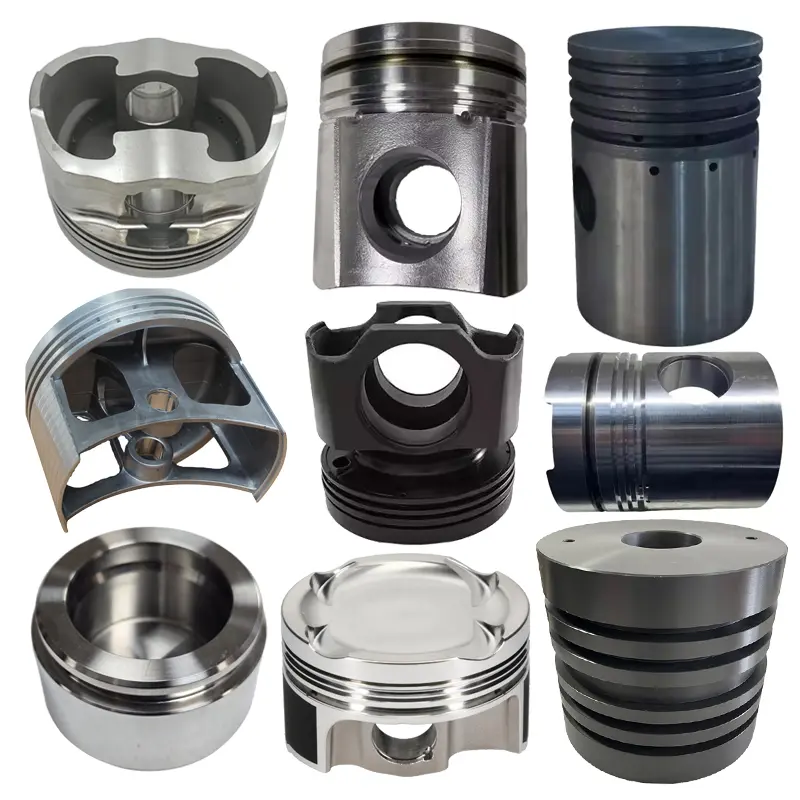
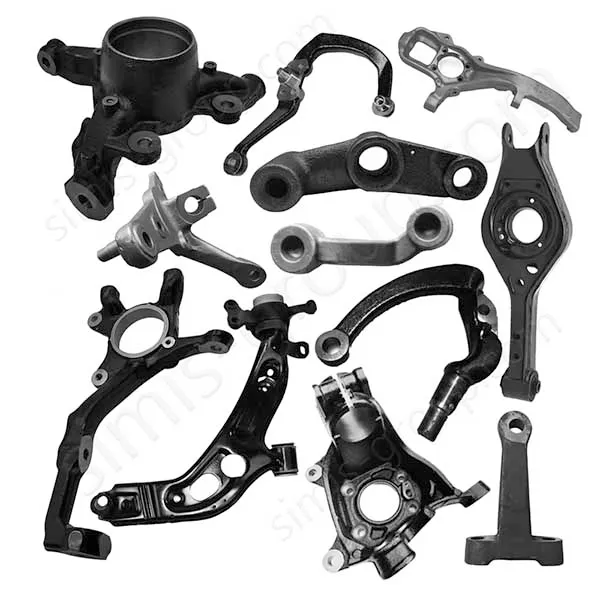
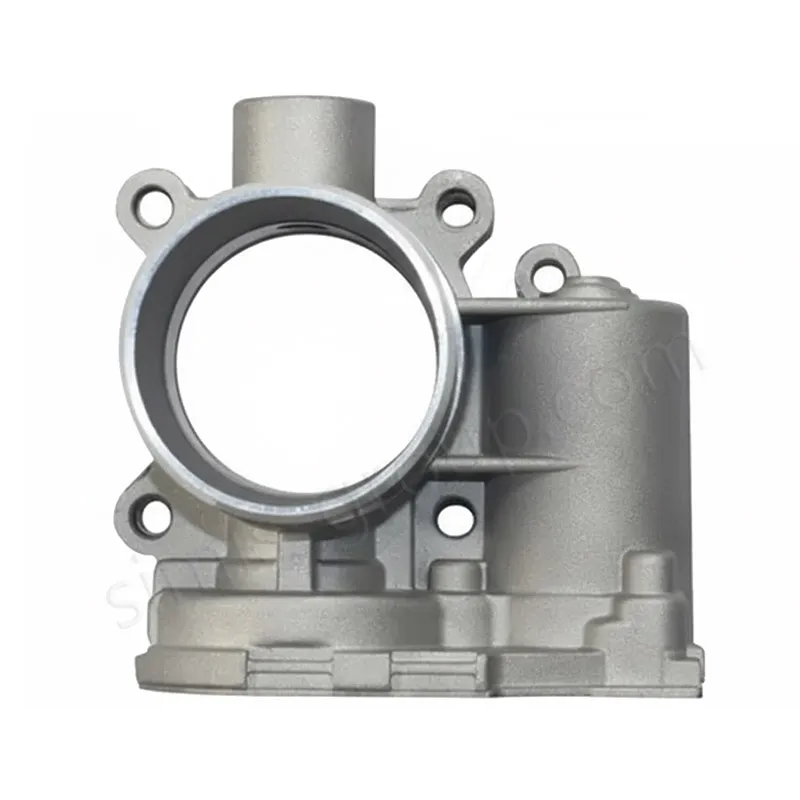
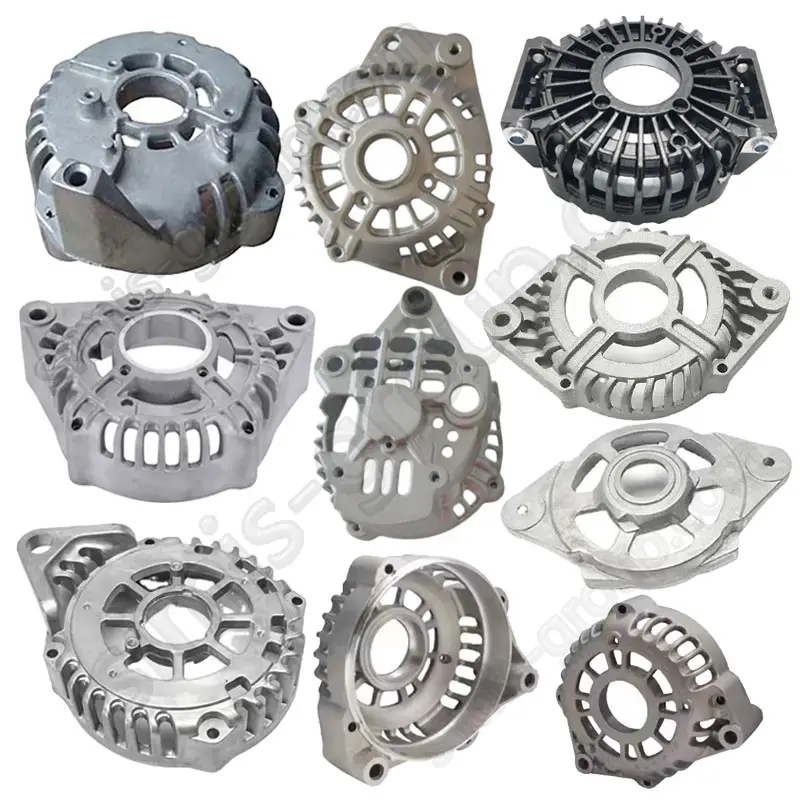
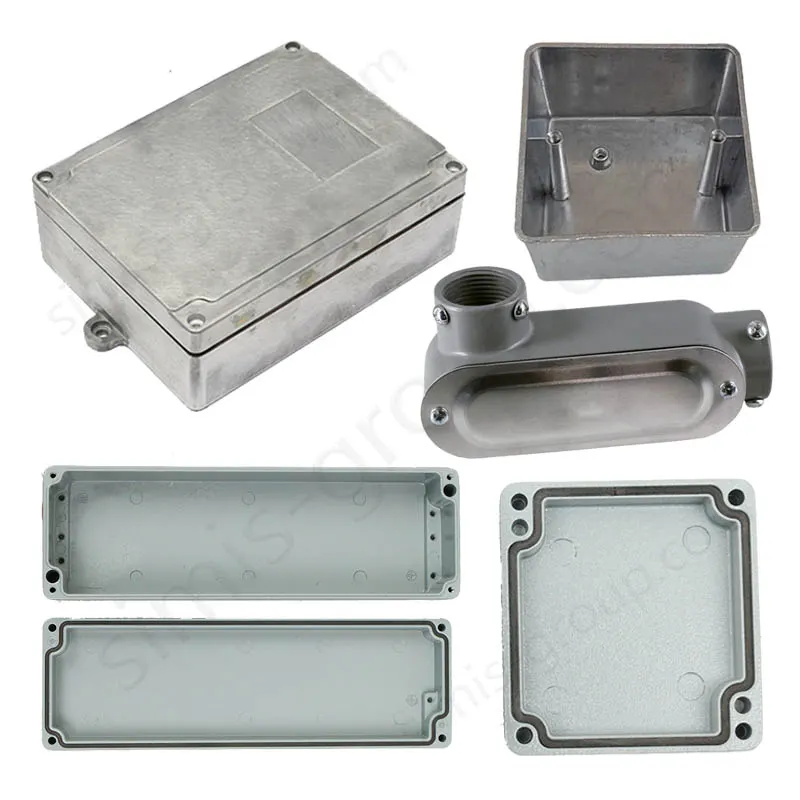
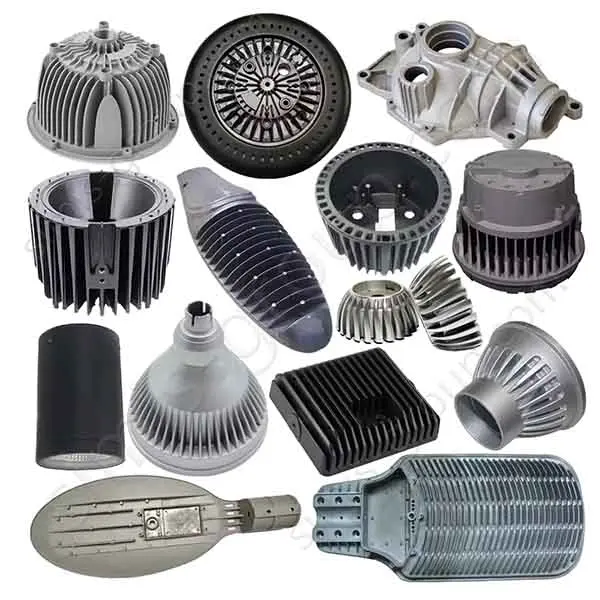
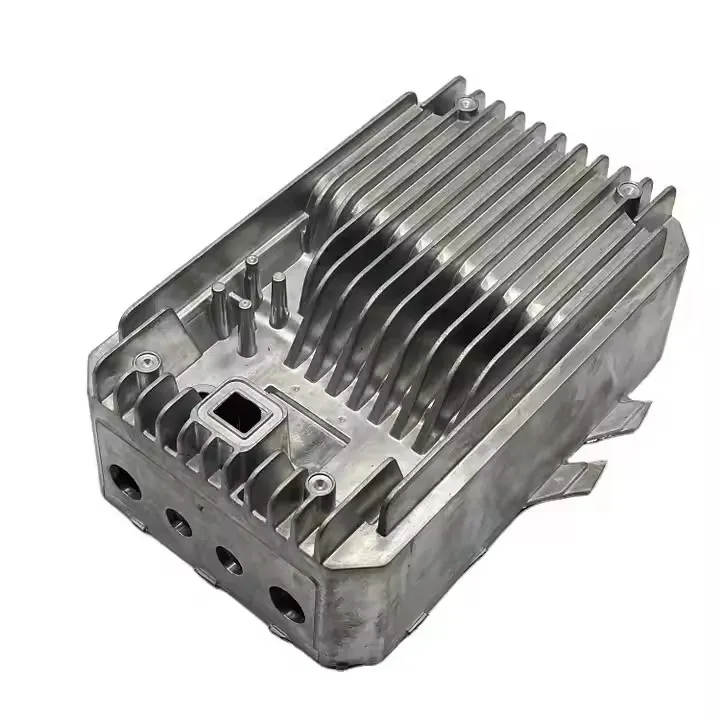
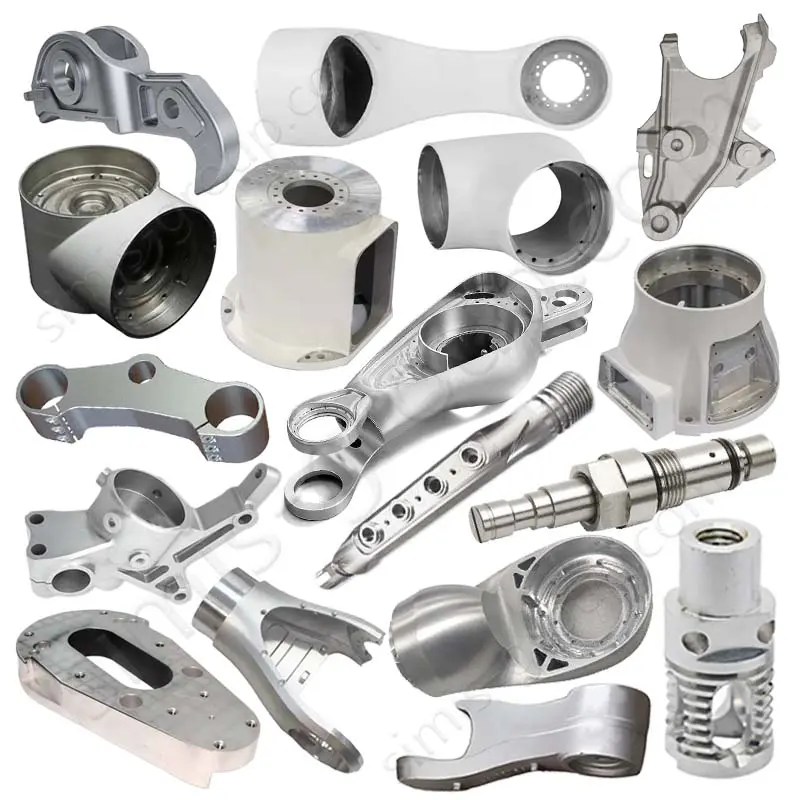
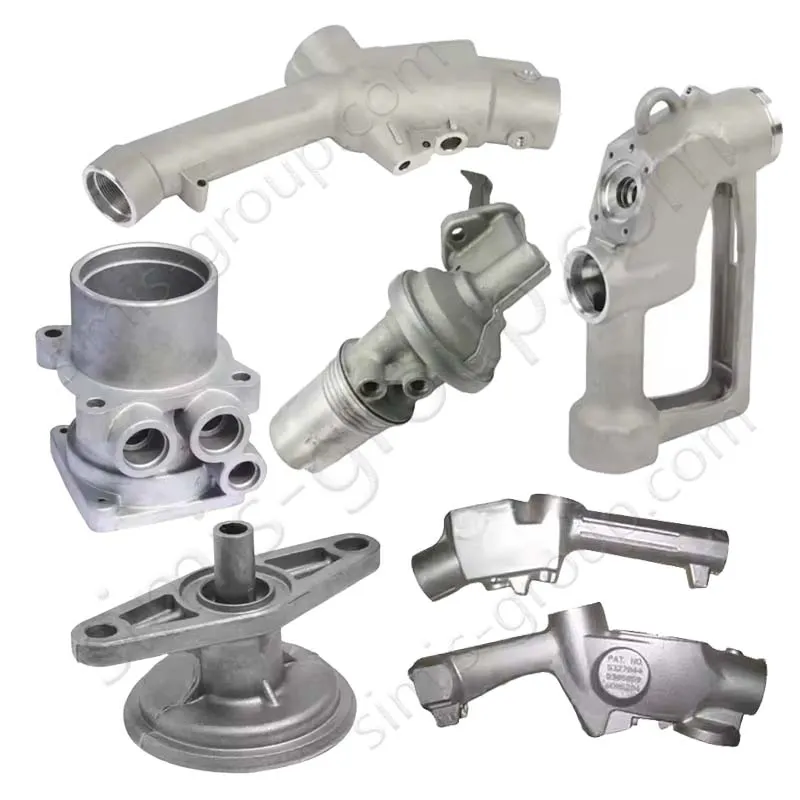
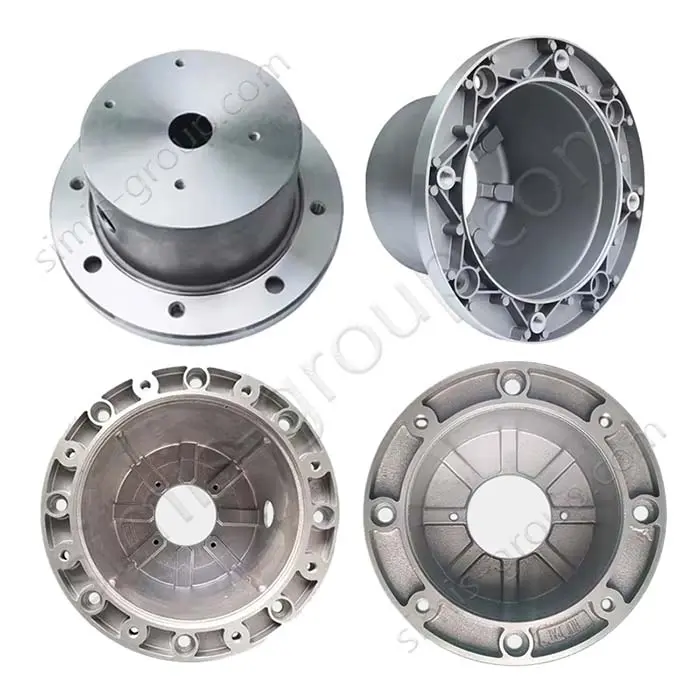
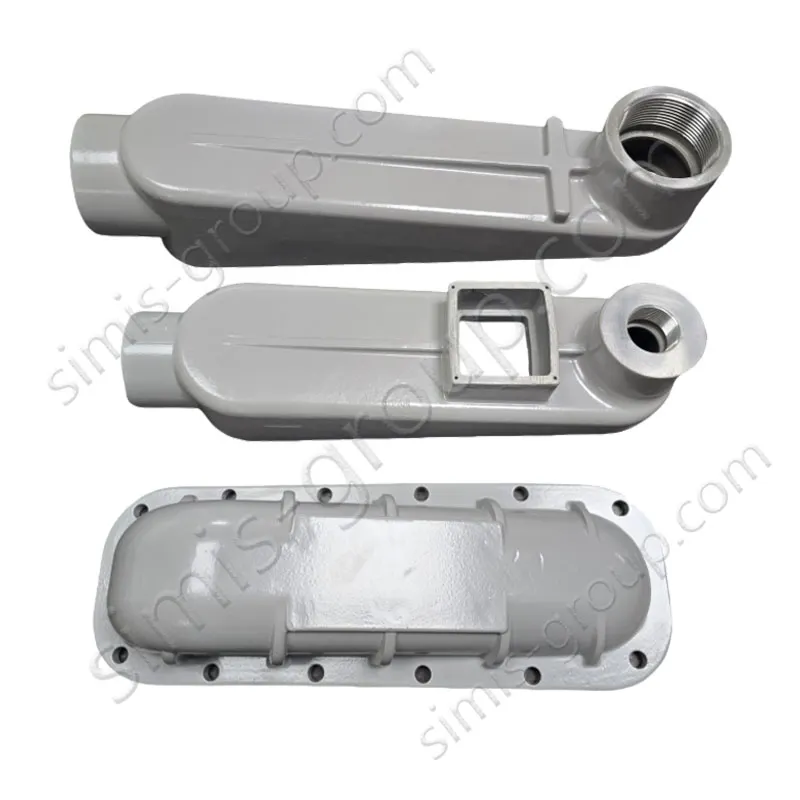
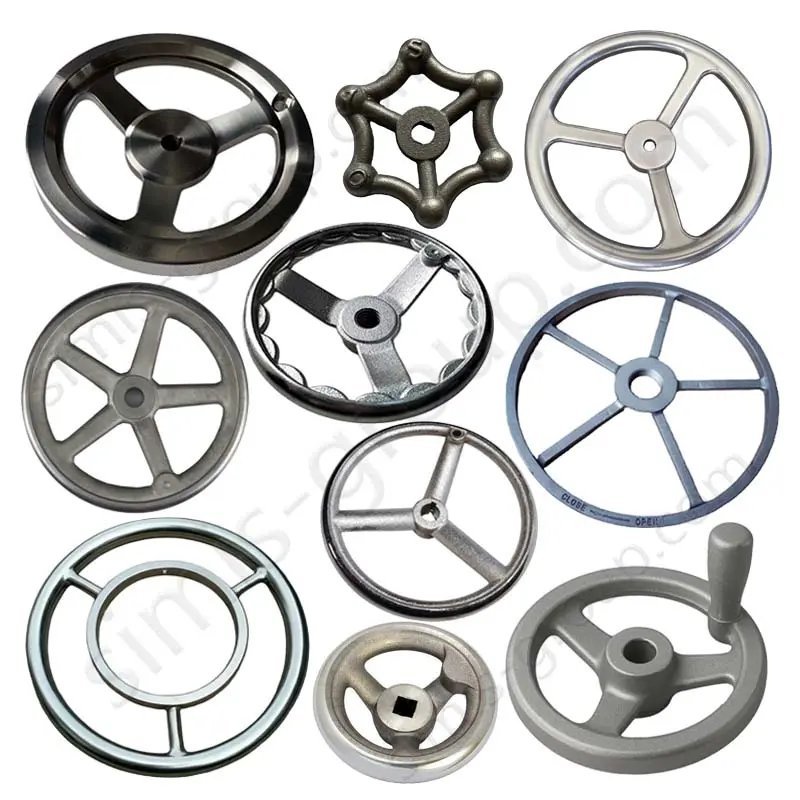
SIMIS provides custom gravity permanent mold casting for aluminum alloy components manufactured to customer drawings. We use reusable metal molds and gravity-fed filling for gearbox housings, pump components, brackets, machinery fittings and other OEM castings. Selected copper alloys can be evaluated where the alloy, geometry and tooling requirements are compatible with this process.
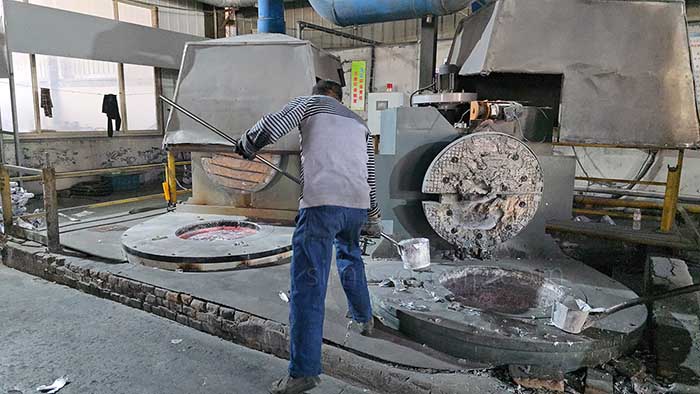
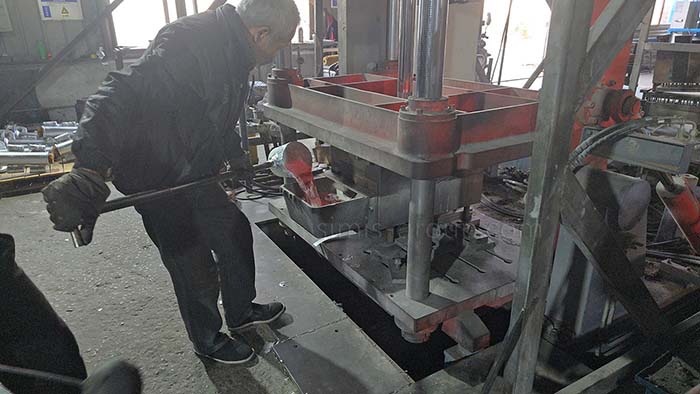
Our production setup includes semi-automatic gravity pouring with tilt control, mold heating and cooling, and induction or resistance melting equipment. Mold design, gating, solidification, machining allowances and inspection requirements are reviewed before production. CNC machining, applicable heat treatment and finishing can be arranged according to the approved specification.
| Casting material / route | Reference casting weight | Reference maximum dimensions | Indicative as-cast CT grade | Indicative as-cast finish |
|---|---|---|---|---|
| Aluminum alloy gravity casting | 0.5–50 kg | 1000 × 800 × 500 mm | CT7–CT9 | Ra 6.3–12.5 μm |
| Selected copper alloy gravity casting | 0.5–30 kg | 600 × 400 × 300 mm | CT8–CT10 | Ra 6.3–12.5 μm |
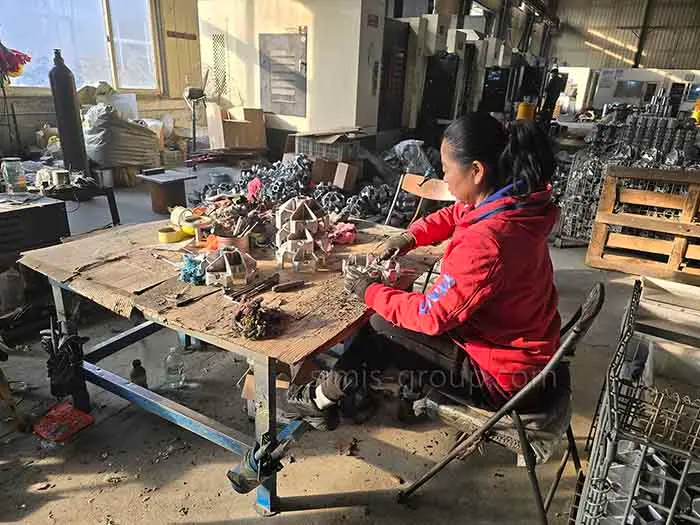
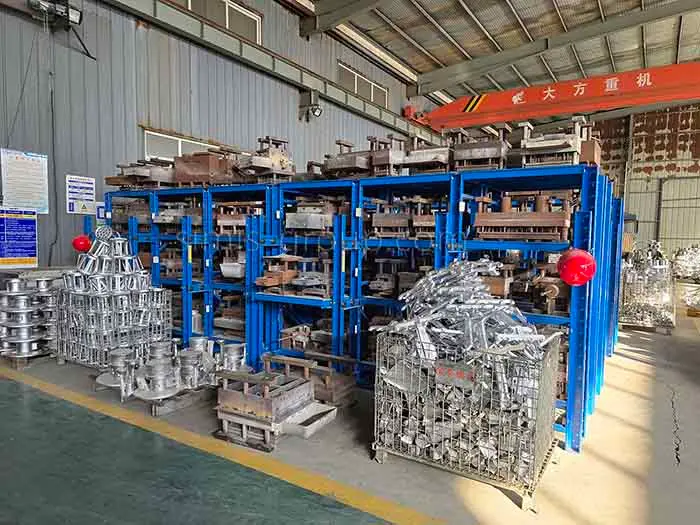
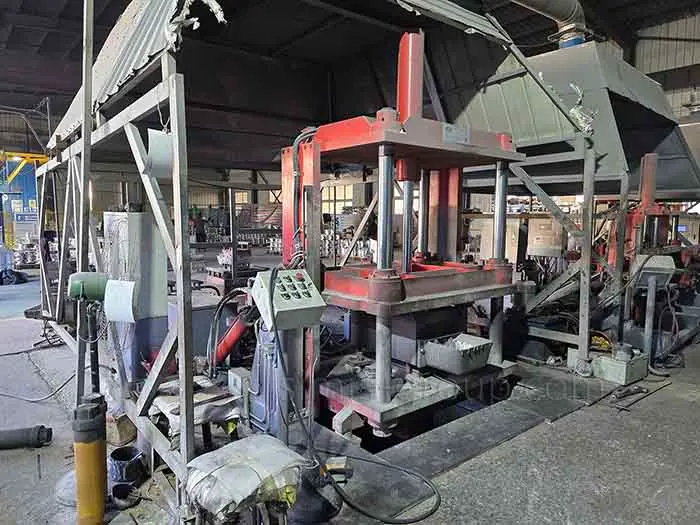
OEM Gravity Castings & Custom Metal Parts




Gravity Permanent Mold Casting Process & Quality Control
Gravity Permanent Mold Casting Process Overview
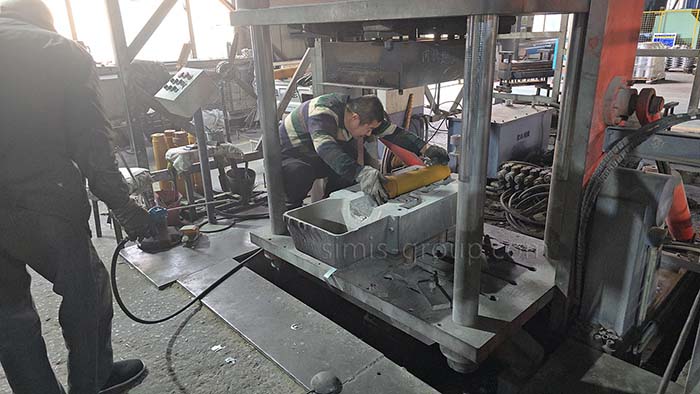
Our gravity casting workflow starts with a customer-approved drawing and a reusable metal mold designed for the chosen alloy. After die preparation and melting, molten metal fills the mold by gravity rather than high-pressure injection. Controlled solidification, part removal, finishing, machining and inspection follow according to the project specification. The sequence may vary with cores, tooling design and heat-treatment requirements.
1. Die Preparation
Permanent molds are constructed from durable metal or ceramic materials. The mold design process must carefully account for the metal's fluidity, the cooling rate, and the complex geometry of the final casting.
2. Alloy Melting and Preparation
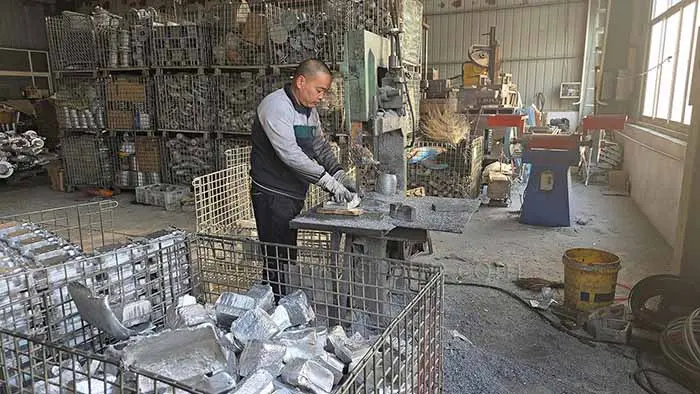
Melt the approved aluminum alloy or other qualified material using the specified furnace and melt-control procedure. Check charge identification and relevant melt conditions before pouring. Chemical composition, degassing, cleaning or other melt treatments are applied where required by the alloy and quality plan.
3. Controlled Gravity Pouring
Transfer molten alloy into the prepared die using a controlled gravity-fed or tilt-pouring method, as appropriate for the tooling. Monitor pouring temperature, flow and mold filling to reduce turbulence and avoidable defects. Gating and feeding arrangements are selected for the component geometry and alloy.
4. Cooling and Solidification
Control die temperature and cooling conditions so that the casting solidifies in line with the approved process plan. Particular attention is given to section changes, feeding and potential shrinkage or distortion. Cooling time depends on the alloy, part size and mold arrangement.
5. Mold Opening and Casting Removal
Open the reusable die and remove the casting when it has sufficient strength for safe handling. Inspect obvious surface defects, parting-line mismatch and potential damage caused during ejection or removal. Prepare the mold for the next cycle and check its working condition as needed.
6. Gate, Riser Removal and Cleaning
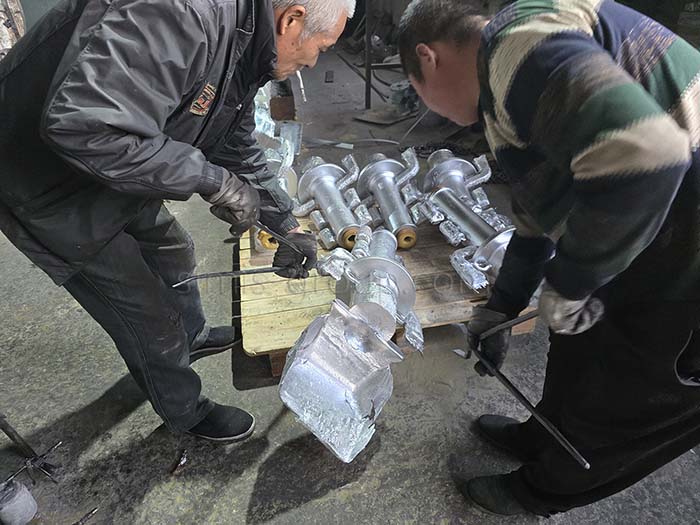
Remove gating, feeders and excess metal, then clean the casting using the applicable trimming, deburring or surface-cleaning method. Check the casting for visible defects and preserve machining allowances on critical features. Any rework is handled under the agreed acceptance criteria.
7. Heat Treatment and CNC Machining
Apply the specified heat treatment where the alloy and required temper permit it, and machine critical bores, threads, mounting faces and sealing interfaces to the released drawing. Not all alloys or castings require the same heat treatment. Finishing and coating are arranged according to the part specification.
8. Final Inspection and Approval
Comprehensive quality inspection is performed. This includes surface quality inspection, dimensional checks, and mechanical property testing to ensure the finished permanent mold castings strictly adhere to the requirements of the design drawings.
Aluminum & Copper Alloys for Gravity Casting
Materials for Custom Gravity Permanent Mold Castings
SIMIS focuses on custom aluminum alloy gravity castings and evaluates selected copper alloy components where the permanent-mold route is technically suitable. The material grade, heat-treatment condition, service environment and casting method are confirmed from customer drawings. Representative grades are subject to supply, tooling and production review.
| Material category | Representative grades / material basis | Typical OEM applications |
|---|---|---|
| Aluminum casting alloys | A356.0 / AlSi7Mg-type and 319.0, subject to project confirmation | Gearbox and motor housings, brackets, pump parts, covers and machinery components |
| Selected copper casting alloys | Customer-specified bronze or brass; permanent-mold suitability must be confirmed for each grade | Small pump components, bushings, impellers and industrial fittings |
| Other specified light alloys | Engineering review only; no routine gravity-casting grade or capacity is implied | Projects requiring alloy-specific melting, mold and quality qualification |
For more material-specific capabilities, see our Aluminum Casting and Copper Alloy Casting pages. Please provide a 2D drawing or 3D model, material grade, estimated quantity, required temper and inspection criteria for a technical quotation.