Quality Control
Quality Management for OEM Castings & Forgings
SIMIS coordinates quality planning for custom metal castings, forgings and machined components using customer drawings, purchase specifications and agreed acceptance criteria.
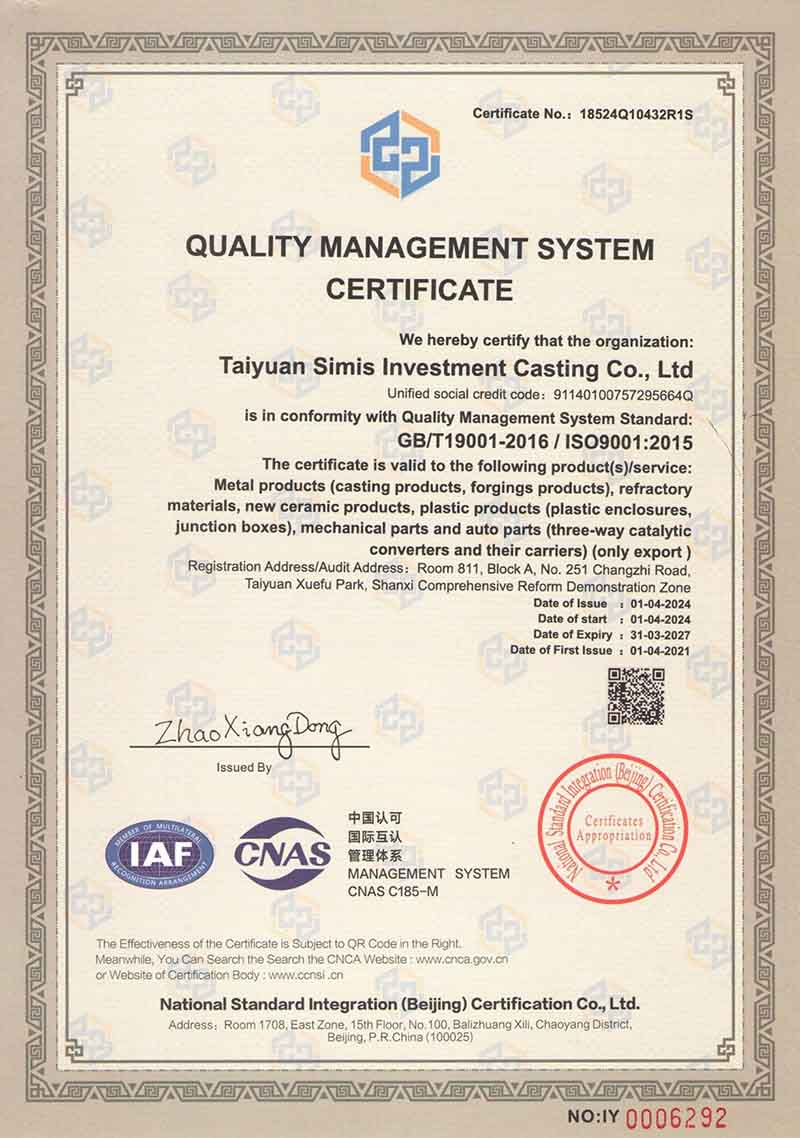
Inspection plans depend on the alloy, manufacturing route, component function and critical characteristics. Before production, material grade, drawing revisions, dimensional tolerances, test methods, sampling requirements and documentation are reviewed for the specific order. Third-party or specialist testing can be discussed when required by the customer.
Quality requirements are addressed at three practical stages:
• Incoming materials: Check material identification, specified grade and available supplier documentation; arrange further verification as required.
• In-process manufacturing: Monitor critical casting, forging, heat-treatment and machining characteristics at agreed control points.
• Final acceptance: Evaluate required dimensions, appearance, material test results and inspection records against approved criteria.
Not every component requires every laboratory test or non-destructive examination method. The inspection scope, test coverage, applicable standards and acceptance limits are defined by the customer specification and the approved production plan.
SIMIS supports drawing-based iron castings, steel castings, aluminum castings, steel forgings and machined metal components for industrial OEM projects. Share your drawing, material grade, intended application and inspection requirements through our contact page for a project-specific manufacturing and quality review.
Casting & Forging Inspection and Testing Process
1. Incoming Material Inspection & Traceability
Before production, incoming stock, ingots, scrap additions or purchased blanks are checked against the specified material grade and available identification records as appropriate to the process. Heat or batch traceability, supplier certificates and chemical composition are reviewed where required. Mechanical testing, metallography and other checks are planned according to the material specification rather than automatically applied to every incoming item.
2. Visual Inspection of Castings & Forgings
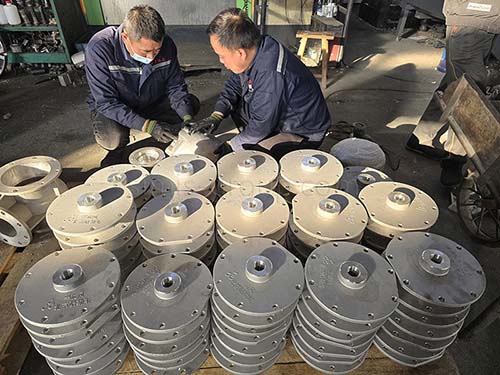
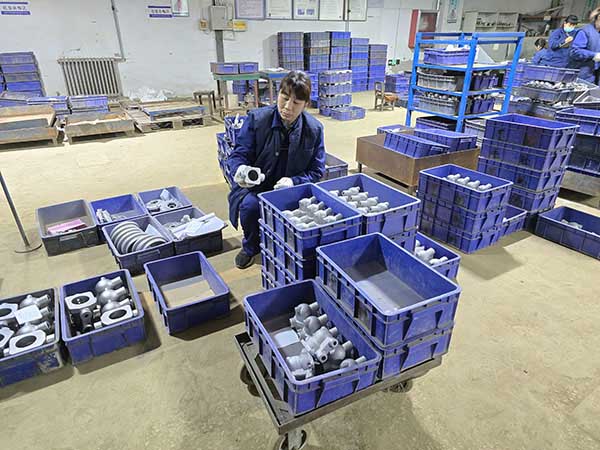
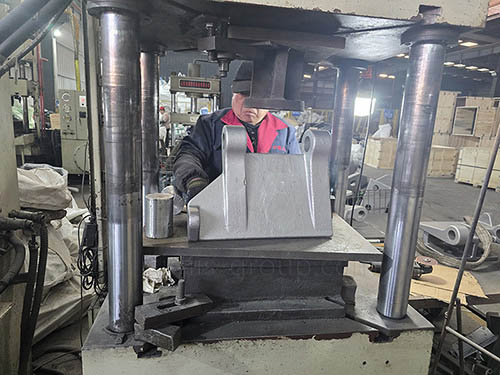
Castings, forgings and machined components are visually examined at relevant manufacturing stages for accessible surface discontinuities, excess flash, burrs, remaining gates and risers, handling damage or visible cracks. Inspection frequency and acceptance levels follow the agreed control plan; not every order requires individual 100% visual examination.
• Visual examination: Assess accessible surfaces under suitable lighting, using magnification when needed to clarify an indication.
• Machined surfaces: Check deburring, obvious tool marks, edge condition and visually accessible functional surfaces against the drawing or sample.
3. Surface Finish & Coating Inspection
• Surface roughness: Measure specified machined surfaces with a suitable roughness instrument when a numerical finish requirement is defined; review as-cast surfaces against applicable visual or comparator criteria.
• Coatings and corrosion protection: For painted, plated or otherwise treated parts, confirm the required coverage and examine coating thickness, appearance or adhesion when specified. Any corrosion testing and acceptance conditions must be agreed separately.
4. Chemical Composition Verification
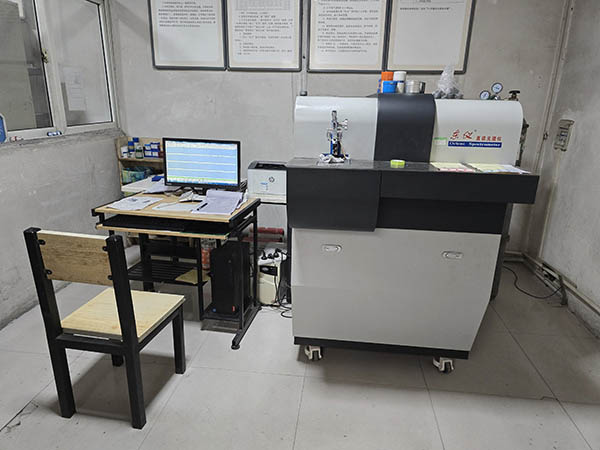
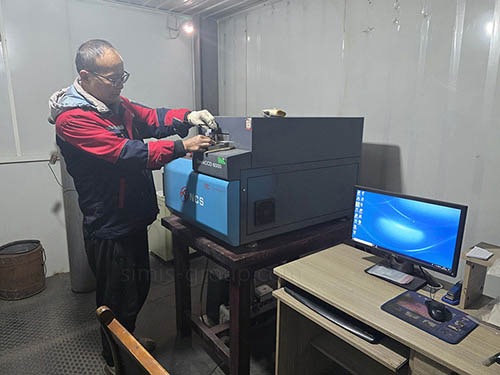
• Spectrometric analysis: Optical emission spectroscopy or another suitable technique may be used to check alloying elements and compare results with the specified grade or heat analysis requirements.
• Supplemental chemical verification: Where particular trace elements, alloy types or purchasing standards require additional analysis, the analytical method, sampling location and report format are agreed for the project.
5. Dimensional, Geometric & Weight Inspection
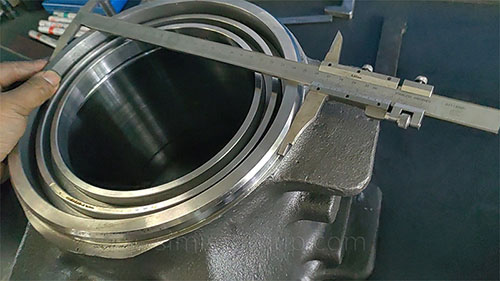
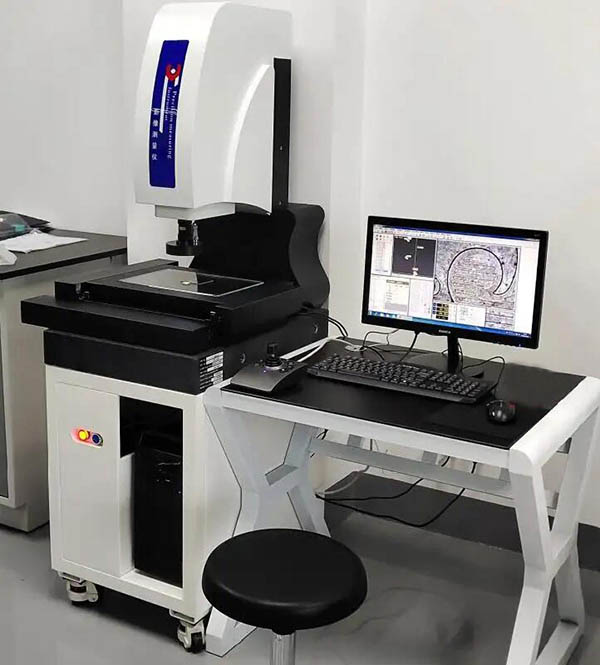
Calipers, micrometers, bore gauges, height gauges and other appropriate instruments are used to check specified dimensions and machining features. Critical dimensions, sampling frequency and measurement conditions are identified from the drawing and inspection plan.
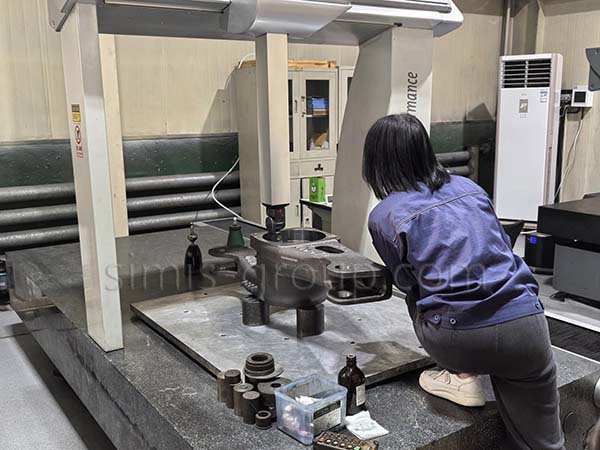
Coordinate measuring machine (CMM) inspection can be selected for complex machined surfaces, bore positions, datums and geometric relationships when these features require coordinate-based verification. The program and measurement approach are based on the approved drawing.
Flatness, perpendicularity, parallelism, roundness, concentricity or positional tolerances are evaluated where specified. Measurement setups use the defined datum system rather than relying only on overall length and width dimensions.
Part mass may be checked when weight affects assembly, packaging, balance or contractual acceptance. The weighing method, allowable variation and inspection frequency are established for the particular component.
6. Mechanical Properties & Metallographic Testing
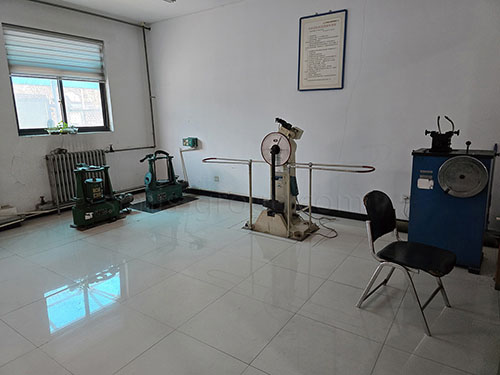
Brinell, Rockwell, Vickers or other suitable hardness methods may be selected according to alloy, heat-treatment condition, section size and the specified hardness range. Test locations and surface preparation are considered when interpreting results.
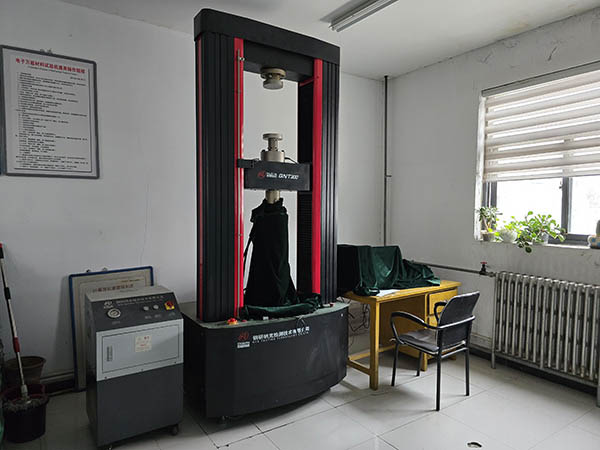
Tensile tests are typically performed on representative test coupons or samples, where specified, to determine properties such as tensile strength, yield strength and elongation. Sampling practice and acceptance values follow the applicable material or purchase specification.
Charpy impact testing may be specified for components requiring defined toughness, including at a designated low test temperature. The specimen orientation, notch configuration, temperature and minimum absorbed energy are confirmed before testing.
Bend testing is considered only when required by a material standard, fabrication procedure or order-specific acceptance plan. Because the test can deform or destroy the specimen, its purpose and sampling arrangement must be established in advance.
Compression testing may be applicable to selected materials or component designs. Loading conditions, specimen geometry and required results are determined by the relevant test specification; it is not a routine test for every casting or forging.
Metallographic examination can evaluate graphite morphology, matrix structure, grain features, inclusions or heat-treatment effects when required for the specified material. The preparation, examination locations and acceptance criteria depend on the alloy and test standard.
7. Non-Destructive Testing (NDT)
Radiographic testing (RT), using suitable X-ray or gamma-ray techniques, can reveal certain volumetric discontinuities, such as porosity and inclusions, in eligible castings. Feasibility and sensitivity depend on section thickness, geometry, access and the agreed examination procedure.
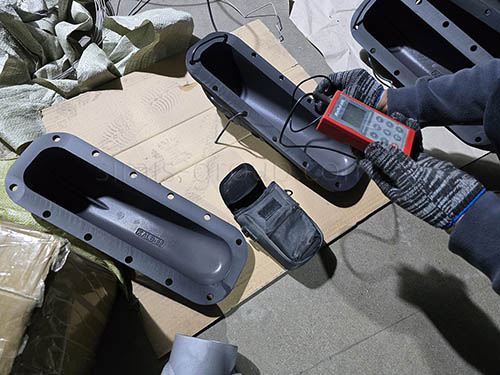
Magnetic particle testing (MT/MPI) is intended to reveal surface and near-surface discontinuities in ferromagnetic materials. It is not a method for detecting deep internal defects, and it is not appropriate for nonmagnetic aluminum or copper alloys.
Ultrasonic testing (UT) can examine internal discontinuities in suitable cast or forged sections. The effectiveness of UT depends on geometry, surface condition, material structure and inspection access; the coverage and acceptance level are defined by the applicable specification.
Liquid penetrant testing (PT/LPT) identifies discontinuities open to the surface of solid, nonporous materials. It can be applied to suitable aluminum, copper and stainless steel components, as well as other eligible materials, after appropriate surface preparation.
The choice of VT, MT, PT, UT or RT is based on the possible defect type, part material, section geometry and customer specification. Required examination areas, extent, personnel qualifications, reporting and acceptance levels should be agreed before production; some projects may require an approved external laboratory.
8. Application-Specific Tests & Inspection Records
• Leak and pressure testing: When specified for pump housings, valve bodies or other pressure-containing parts, confirm the test medium, applied pressure, holding time, allowable leakage and safety arrangements in the purchase specification.
• High-temperature or oxidation evaluation: Specialized exposure testing may be relevant to selected heat-resistant parts, but test conditions and laboratory arrangements must be defined by the project.
• Corrosion assessment: Coating evaluations, salt-spray exposure or other corrosion tests are arranged only where a defined test method and acceptance criterion are provided; such tests do not directly guarantee service life.
• Additional tests and records: Where specified, thermal exposure, environmental testing or other functional checks may be arranged. Depending on the order, deliverables can include material certificates, dimensional results, test reports and traceability records. Submit your inspection requirements with the RFQ through our contact page.


