
Custom Electrical & Lighting Castings and Forgings
OEM Metal Parts for Electrical & Lighting Equipment
SIMIS supports drawing-based OEM manufacturing of custom castings, forgings, CNC-machined parts and suitable fabricated components for electrical equipment and lighting systems. Typical inquiries include aluminum lamp housings, heat sinks, junction boxes, conduit bodies, transformer and motor housings, electrical equipment brackets and street-light pole bases. We review customer drawings, material grades, thermal and mechanical requirements, mounting interfaces, surface finishes, order quantities and inspection specifications before recommending a manufacturing route. Components intended for energized equipment, outdoor installations or regulated systems must be assessed against the customer's applicable design, testing and approval requirements; a metal component alone does not establish an enclosure IP rating or complete-equipment electrical certification. Send 2D drawings or 3D CAD files for feasibility review and quotation.
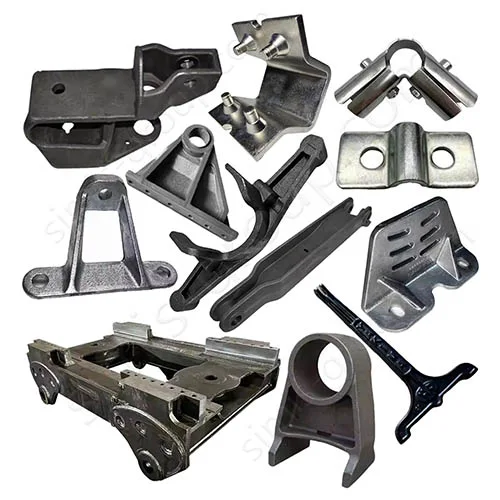
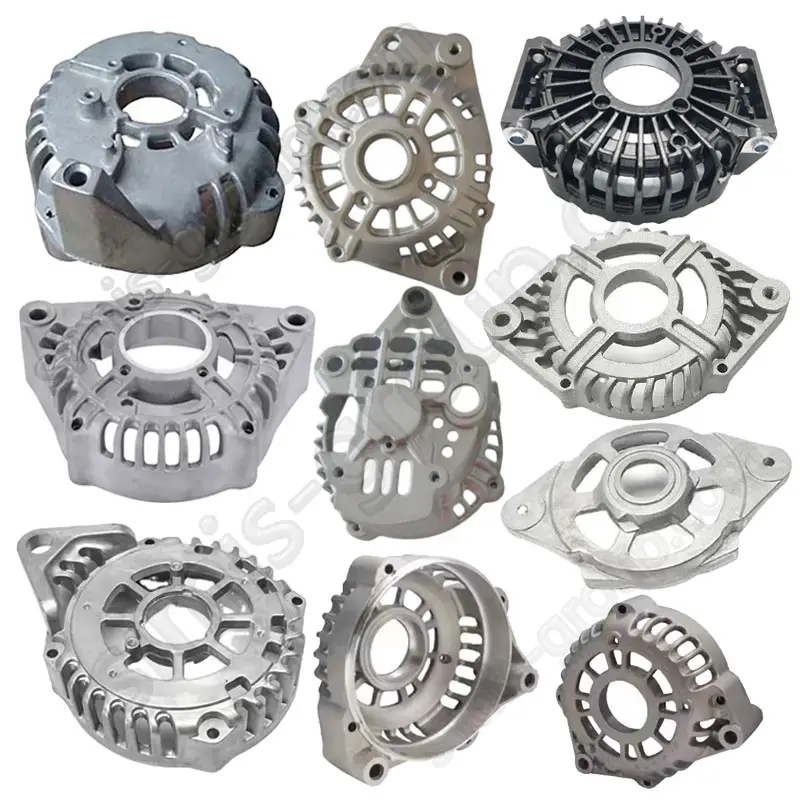
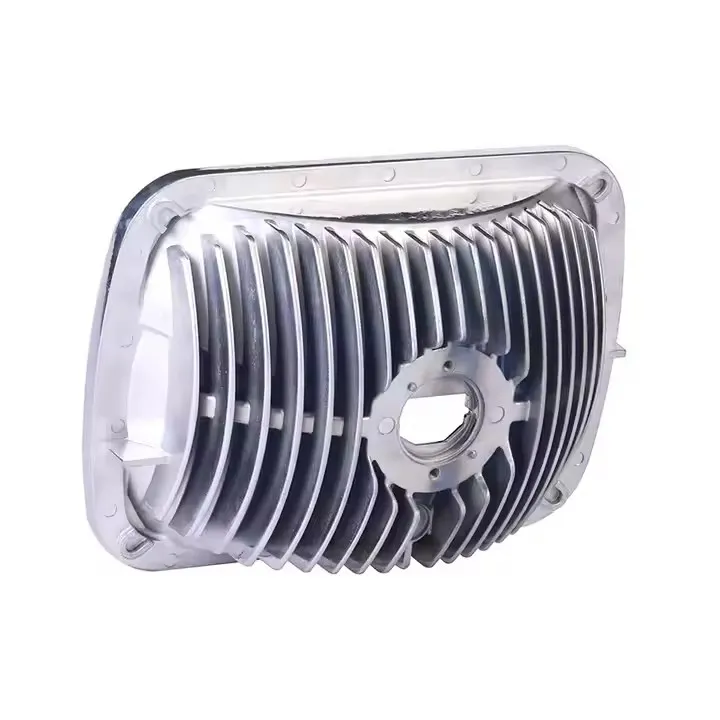


Custom Electrical & Lighting Components & Applications
1.Lighting Fixtures, Lamp Housings & Heat Sinks
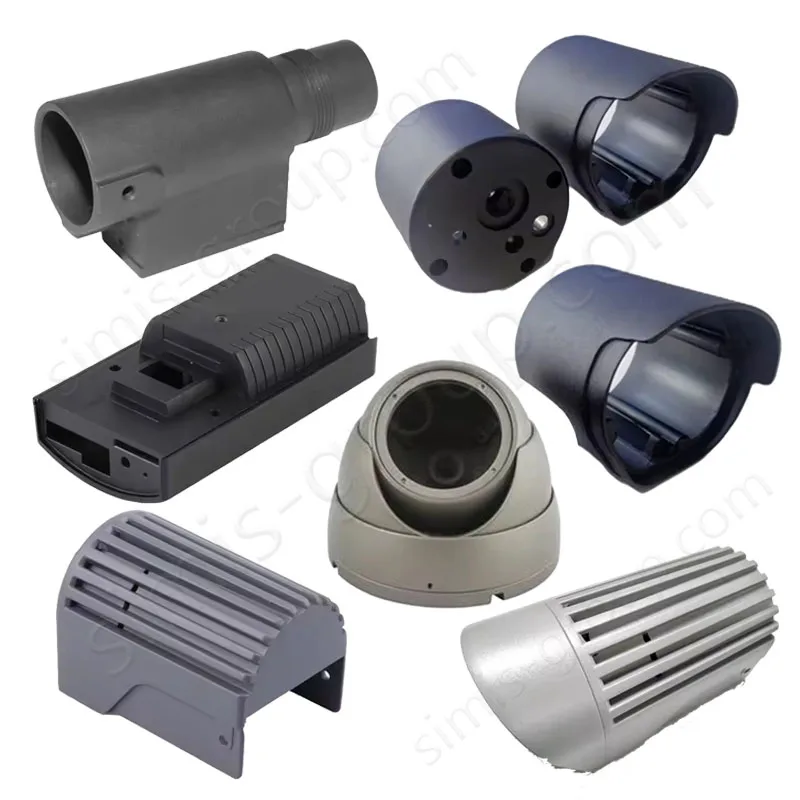
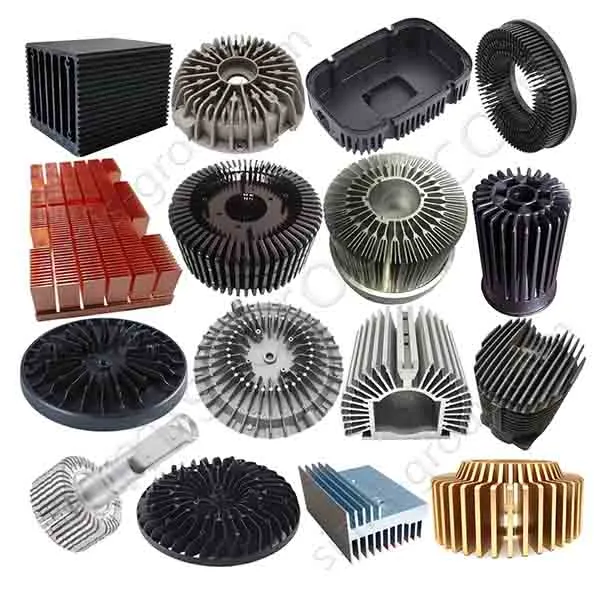
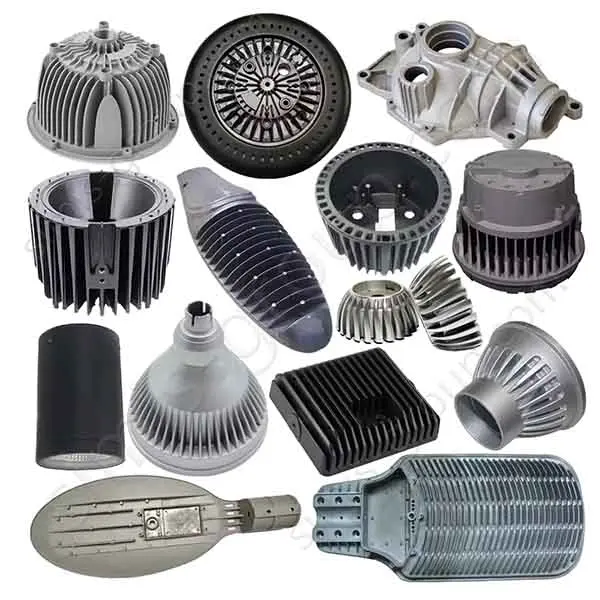
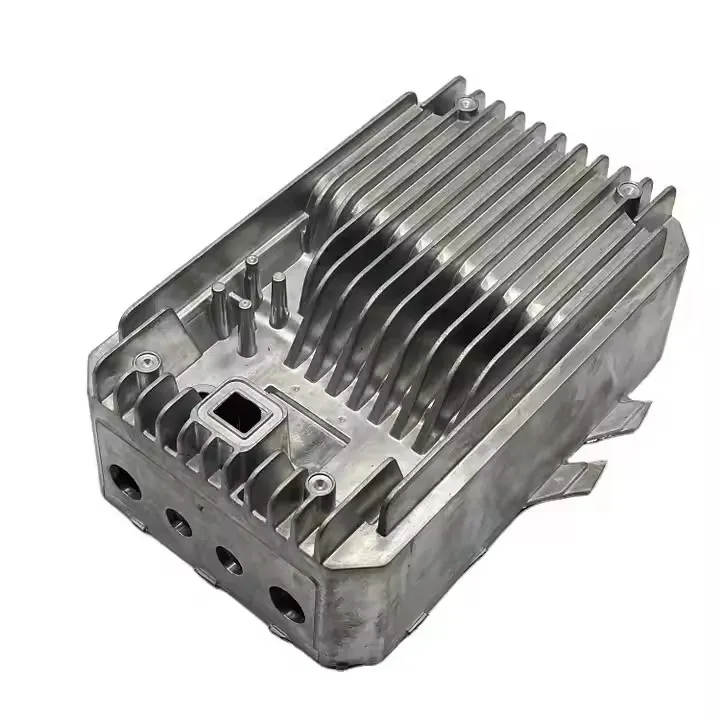
Lighting OEMs use custom lamp housings, LED light housings, heat sinks, bezels, brackets and mounting bases. Aluminum die casting or gravity casting can be assessed for integrated fins and complex mounting features; CNC machining may finish LED board seats, gasket grooves and optical-module interfaces. Sheet-metal parts may suit simpler covers and supports.
Drawing review should establish heat-flow paths, fin geometry, wall sections, mounting-flatness requirements, cable exits, surface finish and appearance. Actual thermal performance, optical output and ingress protection depend on the complete luminaire design, assembly and validation rather than on a housing casting by itself.
2.Electrical Enclosures, Junction Boxes & Conduit Bodies
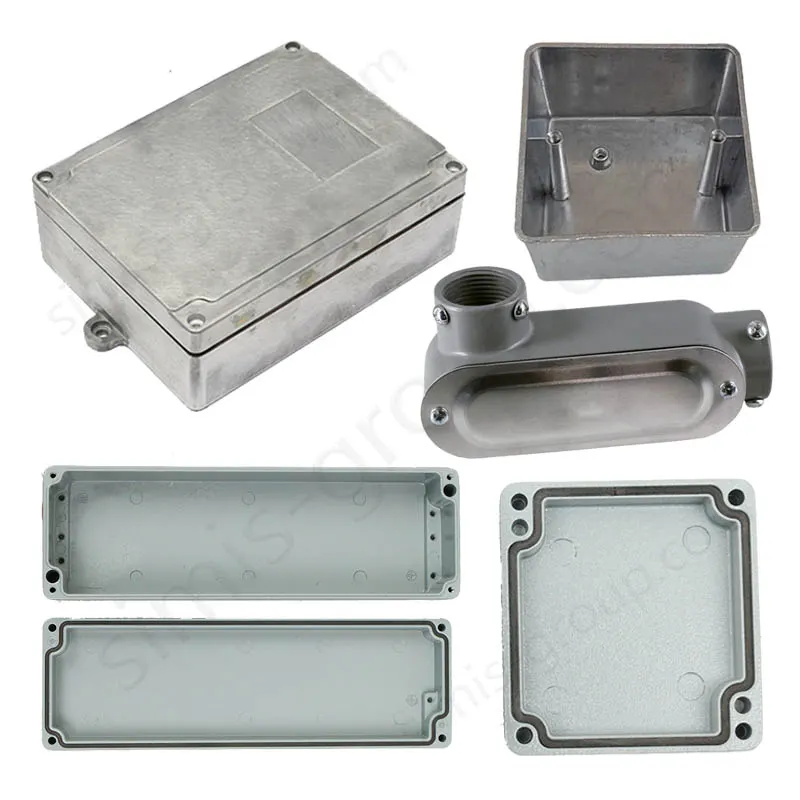
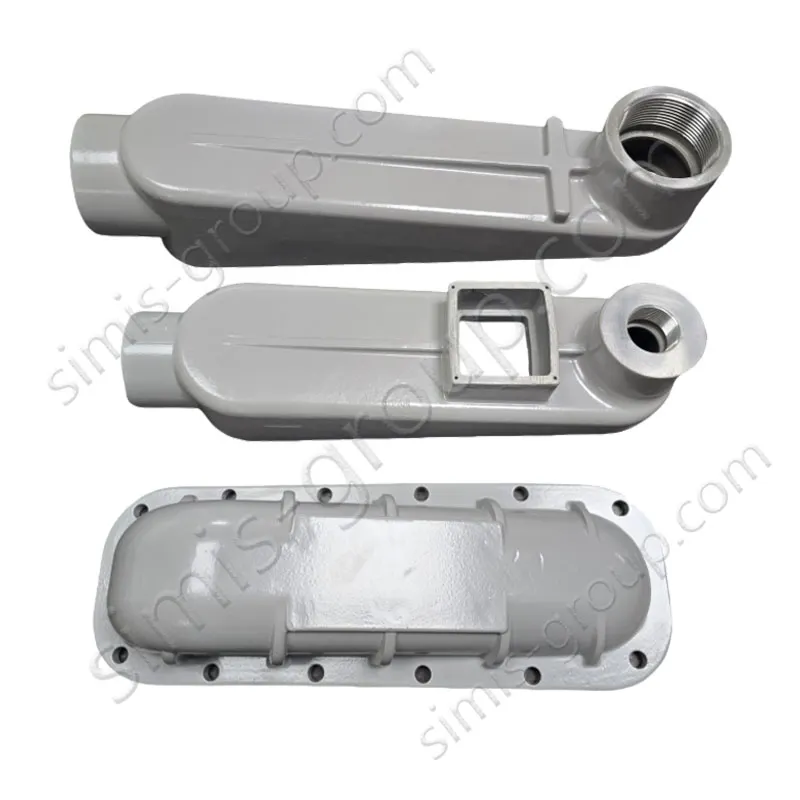
Custom junction boxes, conduit outlet bodies and covers, control housings, cover plates and equipment enclosures may be produced by aluminum casting, CNC machining or sheet-metal fabrication, depending on wall thickness, complexity, volume and the specified alloy.
Important features include cover-to-body flatness, threaded conduit entries, gasket grooves, hinges, fastener bosses, earthing provisions, cable access and finish. The buyer should specify the required sealing arrangement and installation environment. An IP, NEMA or other enclosure rating can only be claimed when the applicable product design and tests support it.
3.Switchgear & Circuit Protection Hardware
Electrical switchgear assemblies use metal support frames, mounting plates, actuator housings, mechanical linkage components and selected insulating-system mounting hardware. Casting can form complex mechanical housings; machined or fabricated steel and aluminum are often appropriate for brackets and equipment structures. Forging may be considered for selected mechanically loaded pins and linkages, not as a universal route for circuit breaker contacts.
The RFQ should identify clearance and creepage constraints, grounding or bonding interfaces, operating forces, dimensional datums, corrosion exposure and whether a part is electrically conductive or purely structural. Electrical withstand, dielectric, arc-fault and equipment certification requirements belong to the specified assembly and approved validation program.
4.Electrical Connectors, Terminals & Mounting Fittings
Electrical connectors may require copper-alloy contact pieces, machined terminals, mechanical clamps, protective housings and custom mounting connectors. The manufacturing choice can involve machining, cold forming, stamping, extrusion, forging or casting depending on conductivity requirements, cross-section, tolerances and production volume.
For any current-carrying component, the customer should specify alloy conductivity, contact geometry, plating, surface condition and the test or qualification method. A mechanically strong forging does not automatically offer the required conductivity, resistance or contact performance; insulating parts and finished connector systems may require other specialist processes.
5.Power Distribution & Transformer Equipment Parts
SIMIS can review transformer enclosures, distribution equipment covers, instrument housings, cable-box components, mounting feet and busbar support hardware. Casting can suit complex bosses or integrated mounting details, while sheet metal or welded frames are often preferable for larger panel-style enclosures. CNC machining can finish gasket seats, terminal openings and precision mounting locations.
Buyers should define required material and finish, heat exposure, cable entries, ventilation, grounding interfaces, mechanical loads and dimensional tolerances. Transformers, busbar systems and energized switchgear are engineered assemblies; a fabricated or cast metal enclosure is not proof of electrical-system approval or short-circuit performance.
6.Electric Motor & Generator Mechanical Components
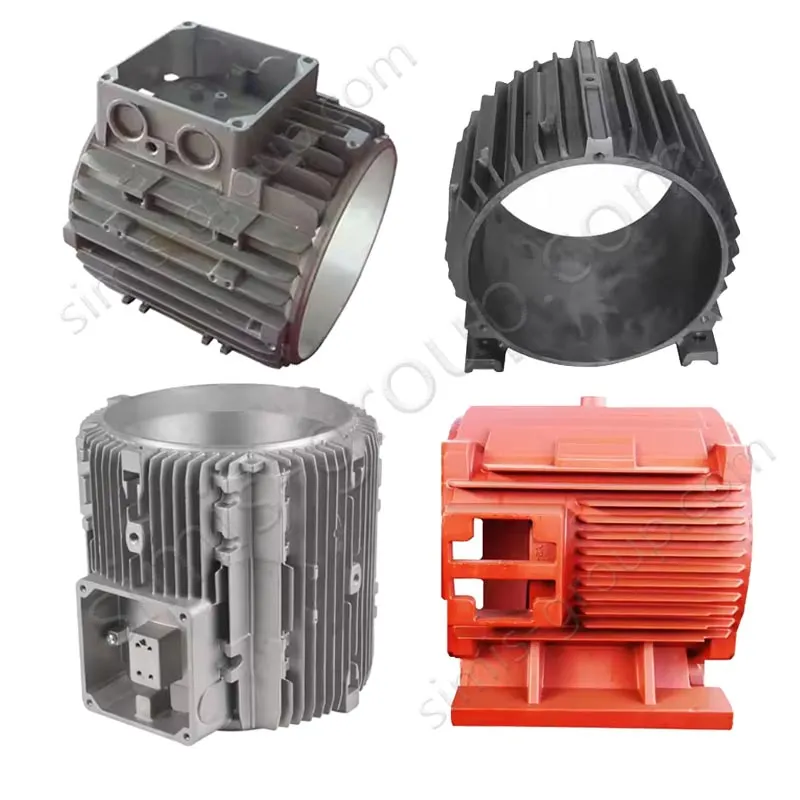
Motors and generators use motor housings, generator housings, bearing supports, end covers, shafts and mounting structures. Gray iron or aluminum casting may suit specific housing designs, while steel forging and machining can be evaluated for shafts or other load-bearing parts when justified by torque, geometry and production quantity.
Critical manufacturing features include bearing-bore coaxiality, shaft-seat fit, end-face runout, sealing surfaces, fastening datums, ventilation openings and thermal growth allowances. The drawing must define acceptable material properties and inspection points; overall motor efficiency, vibration and electrical performance require complete-machine validation.
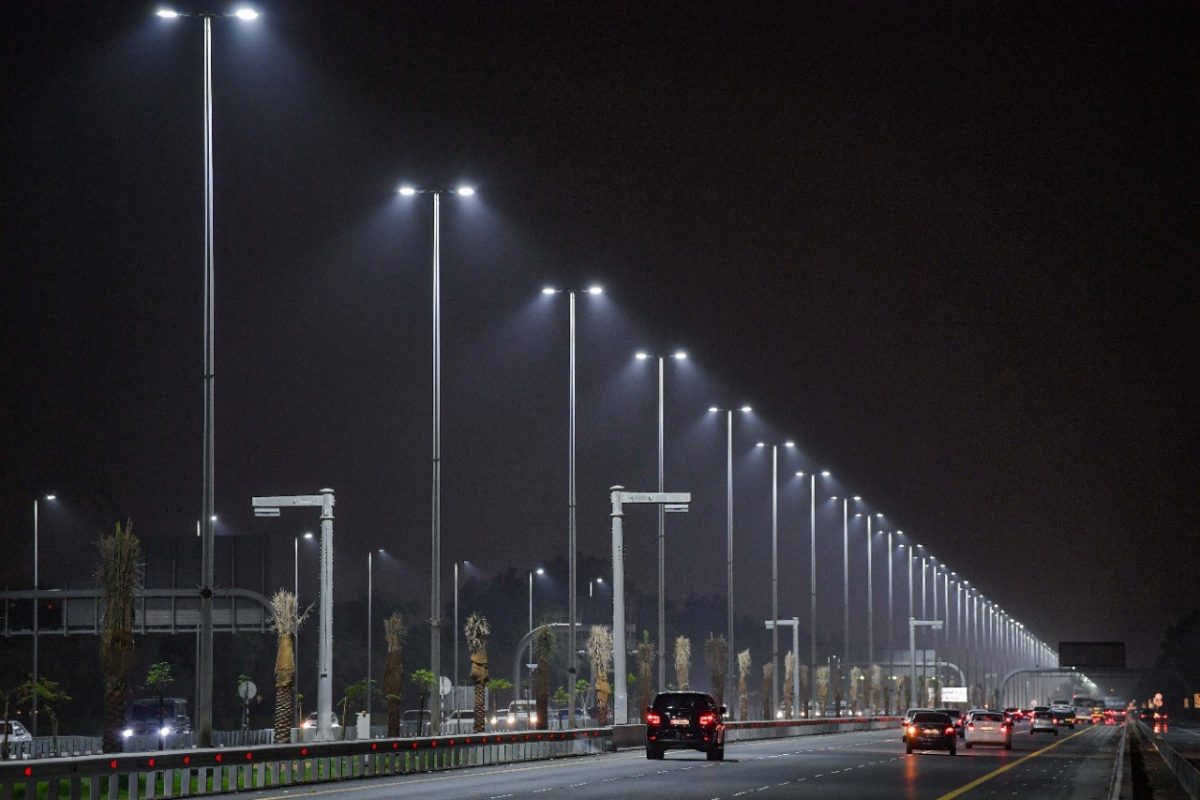
7.Street & Industrial Lighting Pole Hardware
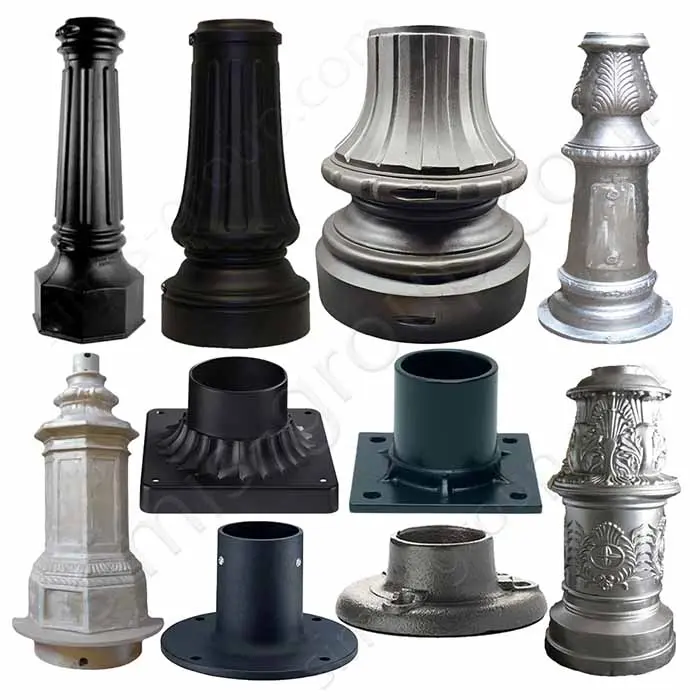
Outdoor lighting assemblies may need street-light pole bases, mounting rings, anchor fittings, support arms and connection brackets. Complex pole bases can be evaluated as castings, while most long poles, tubes and formed arms are produced by fabrication, rolling, extrusion or welding—not routinely by forging entire poles.
For exposed installations, drawings should define anchor-bolt patterns, foundation interfaces, arm geometry, assembly clearances, surface coating and any applicable wind-load, fatigue or structural requirements. Corrosion protection and performance are project-specific; the completed pole assembly may require independent structural approval and site-specific design checks.
Materials for Electrical & Lighting Metal Parts
Cast Iron for Motor Bases & Equipment Supports
Gray iron can suit selected motor bases, generator housings, rigid equipment supports and vibration-sensitive mechanical components when the specified loads and geometry allow. Ductile iron may be considered for brackets or housings needing greater ductility and impact resistance. Iron casting routes depend on section thickness, size and quantity.
Confirm the cast grade, loading, mounting-hole positions, bearing or contact faces, heat exposure, machining requirements and protective finish. Cast iron is generally not a substitute for electrically conductive copper parts or thin-wall aluminum lighting housings.
Carbon, Alloy, Cast & Stainless Steel
Carbon and alloy steel can be assessed for motor shafts, support frames, formed brackets, fittings and mechanical linkages, using steel forging, steel casting, machining or fabrication as appropriate. Stainless steel may suit selected outdoor fittings and enclosures exposed to moisture or corrosive conditions.
Material grade, strength, magnetic properties where relevant, weldability, heat treatment, protective coating and dimensional tolerances should be specified for the actual part. Steel structural components must not be described as electrically insulated or approved for energized service merely because of the material selected.
Aluminum Alloys for Housings & Thermal Components
Aluminum alloys are frequent candidates for heat sinks, LED housings, junction boxes, motor covers and lightweight mounting components. Suitable projects may use aluminum casting, including pressure die casting for appropriate volumes, or CNC machining and fabrication for other geometries.
The alloy and process should be chosen with fin thickness, castability, porosity sensitivity, required flatness, surface treatment and working temperature in mind. Die-cast, gravity-cast, extruded and wrought aluminum grades are not interchangeable without reviewing the specified mechanical and thermal requirements.
Copper Alloys & Other Specified Metals
Copper, brass and bronze may be specified for selected terminals, grounding fittings, bushings, electrical connectors and mechanical interface pieces. Depending on the part, copper-alloy casting, machining or suitable forming and forging routes can be evaluated. Conductive contacts and busbars are often made by rolling, extrusion, stamping or machining rather than conventional shape casting.
For energized parts, the required conductivity, alloy temper, plating, contact resistance and acceptance tests must come from the customer specification. Bronze is also useful for certain non-current-carrying bearing components. Other metals or alloys are considered only when their availability and process suitability are confirmed.
Engineering Review, Manufacturing & Quality Control
3D Drawings
Processing Drawings
Sample
1. Review Drawings & Functional Interfaces
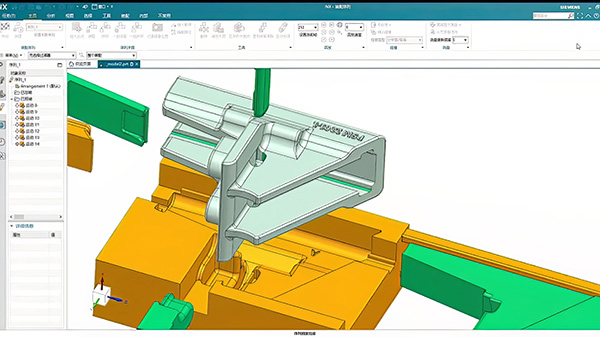
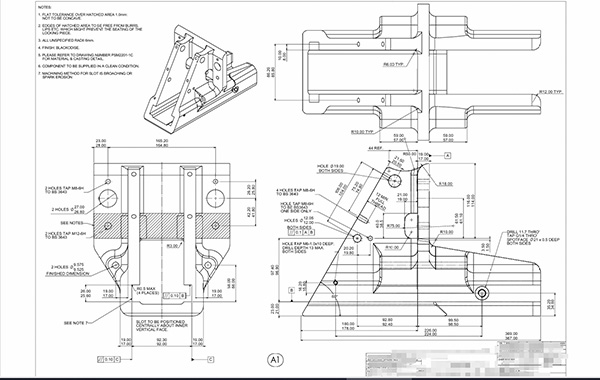
Send 2D engineering drawings, 3D CAD models or representative samples together with target quantities and application details. SIMIS reviews component geometry, intended material, achievable production route, critical features and the assembly surfaces that will locate or seal the part. Typical concerns include LED mounting faces, thermal interfaces, motor bearing seats, gasket channels, conduit threads, cable openings and anchor-bolt patterns.
For electrical and outdoor applications, customers should also identify operating temperature, mechanical loading, relevant environmental exposure and any certification or system-level requirements. A drawing review provides manufacturing feasibility feedback; it is not a substitute for the OEM's design responsibility or formal product approval.
2. Confirm Materials, Process & Acceptance Criteria
Before tooling or machining, the material grade and manufacturing route should be agreed against geometry, required properties, expected batch size and target cost. Aluminum casting may suit finned housings; steel forging may suit a specified shaft or load-bearing linkage; sheet metal may be preferable for large enclosure panels. Copper contact parts require a process and material condition appropriate to their electrical function.
Critical tolerances, coating areas, surface roughness, mating features, appearance limits and required material documentation should be identified on approved drawings. Where applicable, define electrical conductivity or coating-performance tests as customer acceptance criteria instead of assuming they are included in standard casting inspection.
3. Plan Tooling, Prototypes & Process Controls
Where casting or forging is selected, assess parting lines, draft angles, wall sections, machining allowance and any core or die requirements. CNC machining and sheet-metal projects may instead use fixtures, programs and forming setups. Tooling and sampling arrangements are reviewed according to the part design and production volume, not by a fixed lead time applicable to every project.
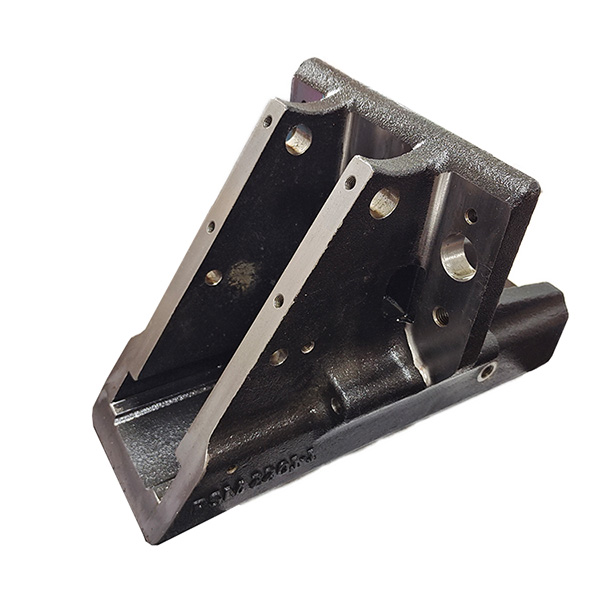
Initial samples can be used to verify mold filling, machining access, assembly clearances and surface-treatment compatibility. Special attention is given to thin cooling fins, threaded bosses, sealing grooves and other features where later rework may be difficult or expensive.
4. Inspect Initial Samples & Confirm Fit
Sample checks are planned around the drawing and the specified risk areas. Dimensional inspection may cover CMM measurements, bore sizes, flatness, true position, profile, thread gauges and visual examination of cast surfaces or coatings. A trial assembly or fit check may be important for electrical housings with mating lids, gaskets, PCB mounts or heat-generating modules.
Chemical analysis, hardness, mechanical tests, pressure or leak tests, NDT and coating tests are added when relevant and required by the purchase specification. IP, dielectric or thermal validation of complete electrical equipment is performed under a separately defined, applicable test plan; these cannot be inferred from a dimensional inspection report alone.
5. Control Manufacturing & Change Management
Following approved sample and specification review, production planning identifies the applicable casting, forging, machining, fabrication, heat-treatment and finishing operations. Important features such as bearing bores, gasket seats, mounting datums, cooling surfaces and contact locations can be assigned appropriate in-process checks. Material identification and process records are controlled to the degree specified by the project.
Any requested adjustment to alloy, process, tooling, coating or drawing revision should be assessed for effects on assembly fit, durability and performance before release. Repeated production should be governed by documented acceptance limits, not by a claim that every item will be dimensionally identical to the sample.
6. Final Inspection, Records & Delivery
Before release, the agreed final inspection plan may include dimensional sampling or 100% checks of designated critical characteristics, visual examination, coating verification, marking and packaging review. For enclosure components, inspect mating surfaces and preserve machined or treated features during shipment; for shafts or supports, protect critical fits and document required measurements.
Reports, material certificates or other traceability documentation are supplied according to the confirmed order requirements. Buyers can review the SIMIS quality control approach and specify any additional inspection or third-party witnessing needed. Compliance with an electrical product standard or enclosure rating must be supported by the appropriate qualified system-level evidence.
Electrical & Lighting Parts Manufacturing Processes
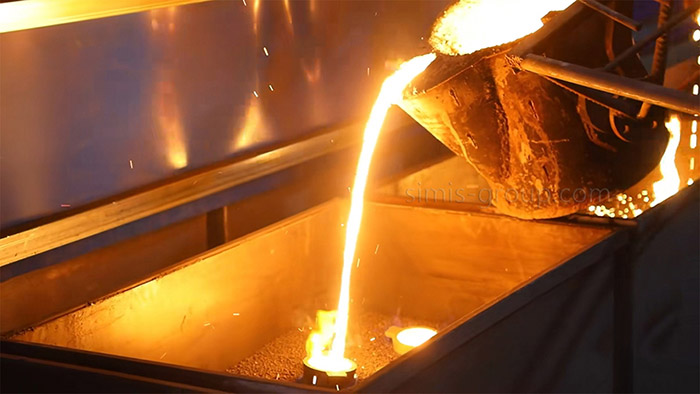
Casting for Electrical Housings & Lighting Parts
Aluminum casting may suit LED lamp bodies, heat sinks, junction-box housings and equipment covers with integral fins, ribs or mounting bosses. Iron casting may be assessed for selected heavy motor bases or rigid supports. The choice between pressure die casting, sand casting and other routes depends on size, alloy, geometry, quantity and drawing requirements.
Casting layout considers wall transitions, shrinkage, machining allowance, porosity sensitivity and finishing operations. Sealing and thermal interfaces may require machining after casting.
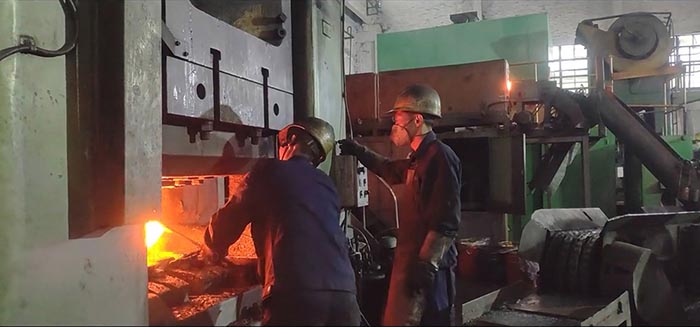
Forging for Shafts & Mechanical Connectors
Steel forging can be evaluated for motor shafts, selected mechanical linkages, load-bearing pins and connecting parts when the material, load and order volume justify this route. Closed-die forging may suit repeat components requiring formed geometry followed by finish machining.
A forging does not by itself establish conductor suitability, contact resistance or electrical safety. Copper terminals, busbars and small contacts may use different forming, machining or stamping routes specified by the customer.
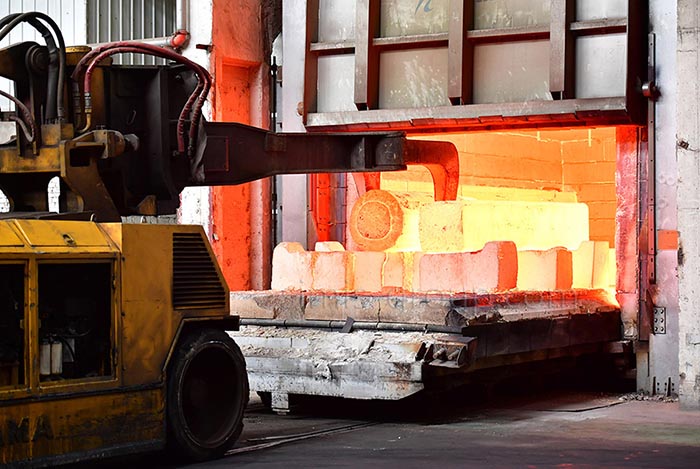
Heat Treatment of Selected Metal Parts
Heat treatment may be required for steel shafts, mechanical fittings or selected cast components to obtain specified hardness, strength, stress relief or dimensional stability. Available routes and acceptable material conditions depend on the alloy and the released manufacturing plan.
Treatment selection should account for possible distortion of bearing fits, mounting faces and threaded features. Heat treatment does not automatically improve electrical conductivity, arc resistance or corrosion behavior.
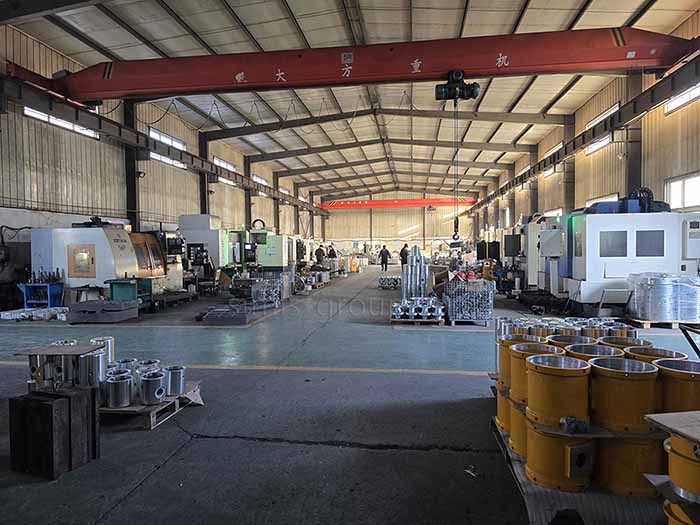
CNC Machining of Fits & Thermal Interfaces
CNC machining can finish motor bearing bores, generator end-cover faces, gasket grooves, threaded conduit entries, LED board seats, mounting patterns and heat-sink contact surfaces. Cast, forged and fabricated blanks may need different workholding and datum strategies.
Dimensional targets such as coaxiality, flatness, surface roughness, thread fit and hole position are defined by the drawing and checked with suitable inspection methods.
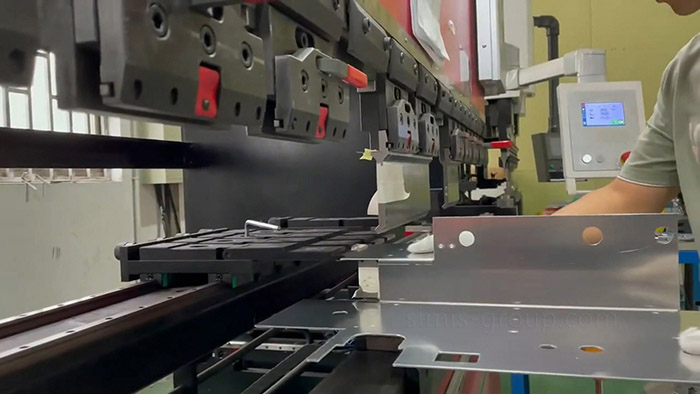
Sheet Metal Fabrication for Enclosures
Sheet metal fabrication may suit control cabinets, electrical enclosure panels, covers, guards, mounting brackets and selected lighting supports. Cutting, bending, forming and welding can be assessed according to material thickness, access openings, assembly method and production quantity.
Reviews cover bend allowances, hole-to-bend distances, panel flatness, seam design, grounding features and finish preparation. Final enclosure protection ratings depend on the completed assembly and tests.
Surface Treatment & Corrosion Protection
Surface treatment may be specified for electrical and lighting metal parts to manage corrosion, appearance or surface wear. Suitable options can include aluminum anodizing, coating or painting, powder coating for appropriate components, and project-specified plating where the substrate and function permit.
Conductive contact areas, grounding paths, heat-transfer faces, threads and gasket seats may need masking or a defined finish. Coating thickness, adhesion, appearance and any conductivity requirements must follow customer specifications; not all coatings preserve electrical contact or heat transfer.


